
Forging & Bladesmithing
Choosing Your First Forge: Gas, Coal, or Two Bricks
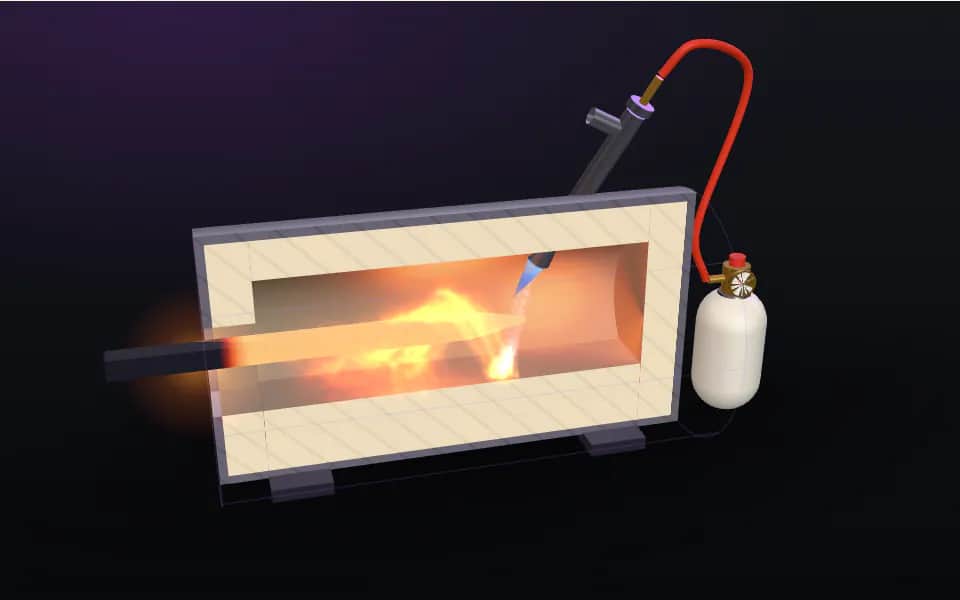
Every forged blade starts with the same purchase decision, and the good news is it’s gotten cheap: a genuinely usable knifemaking forge now costs less…
Forging & Bladesmithing
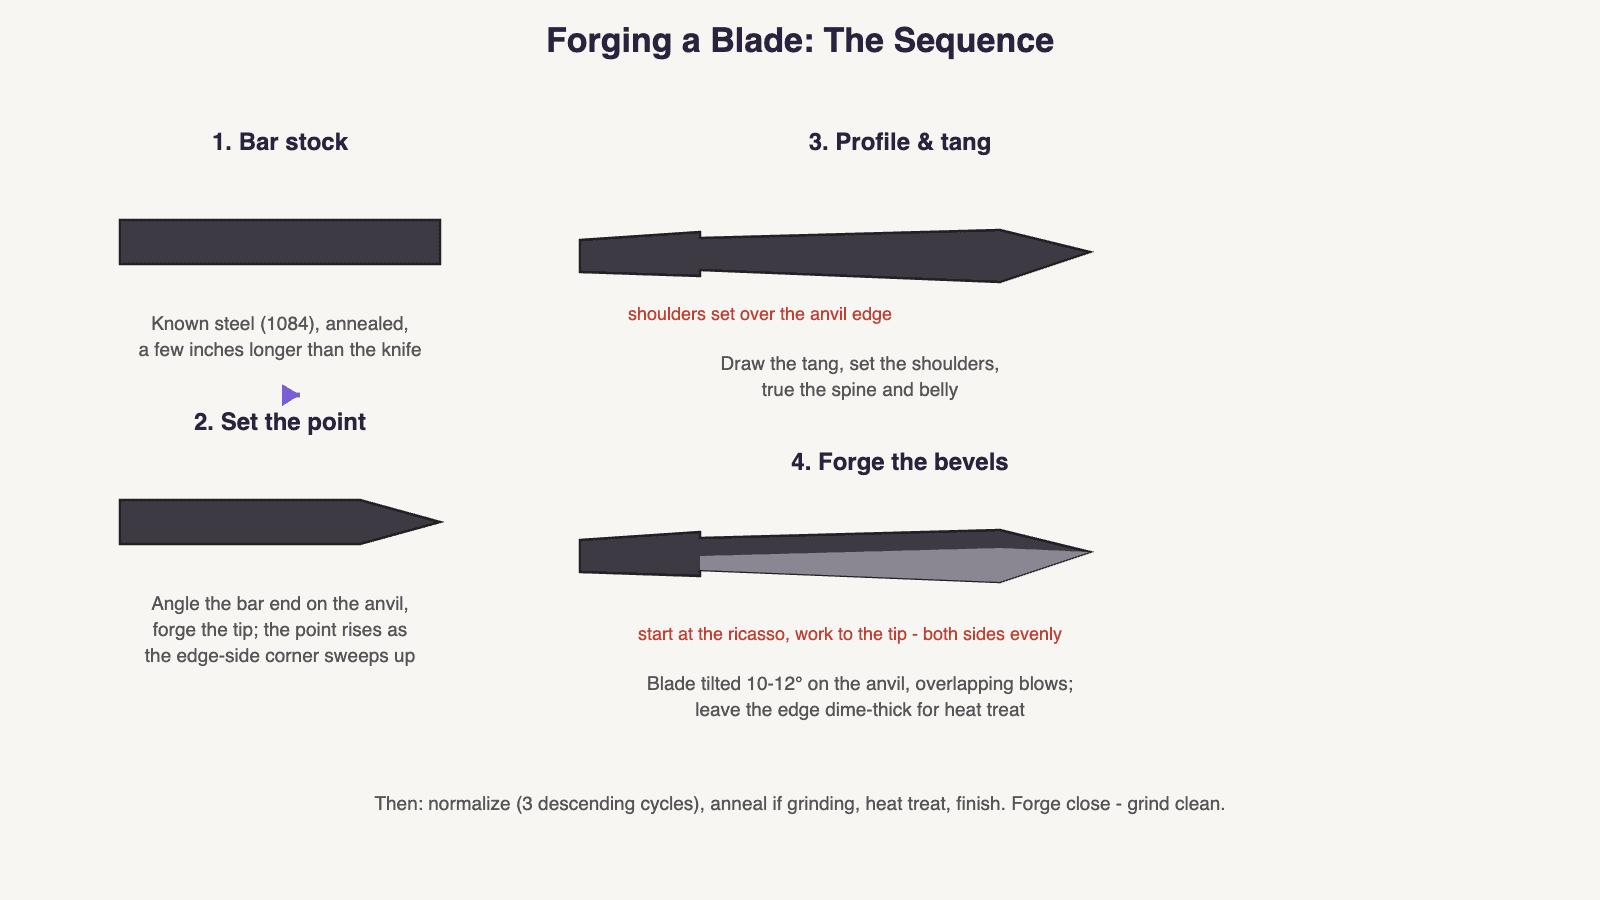
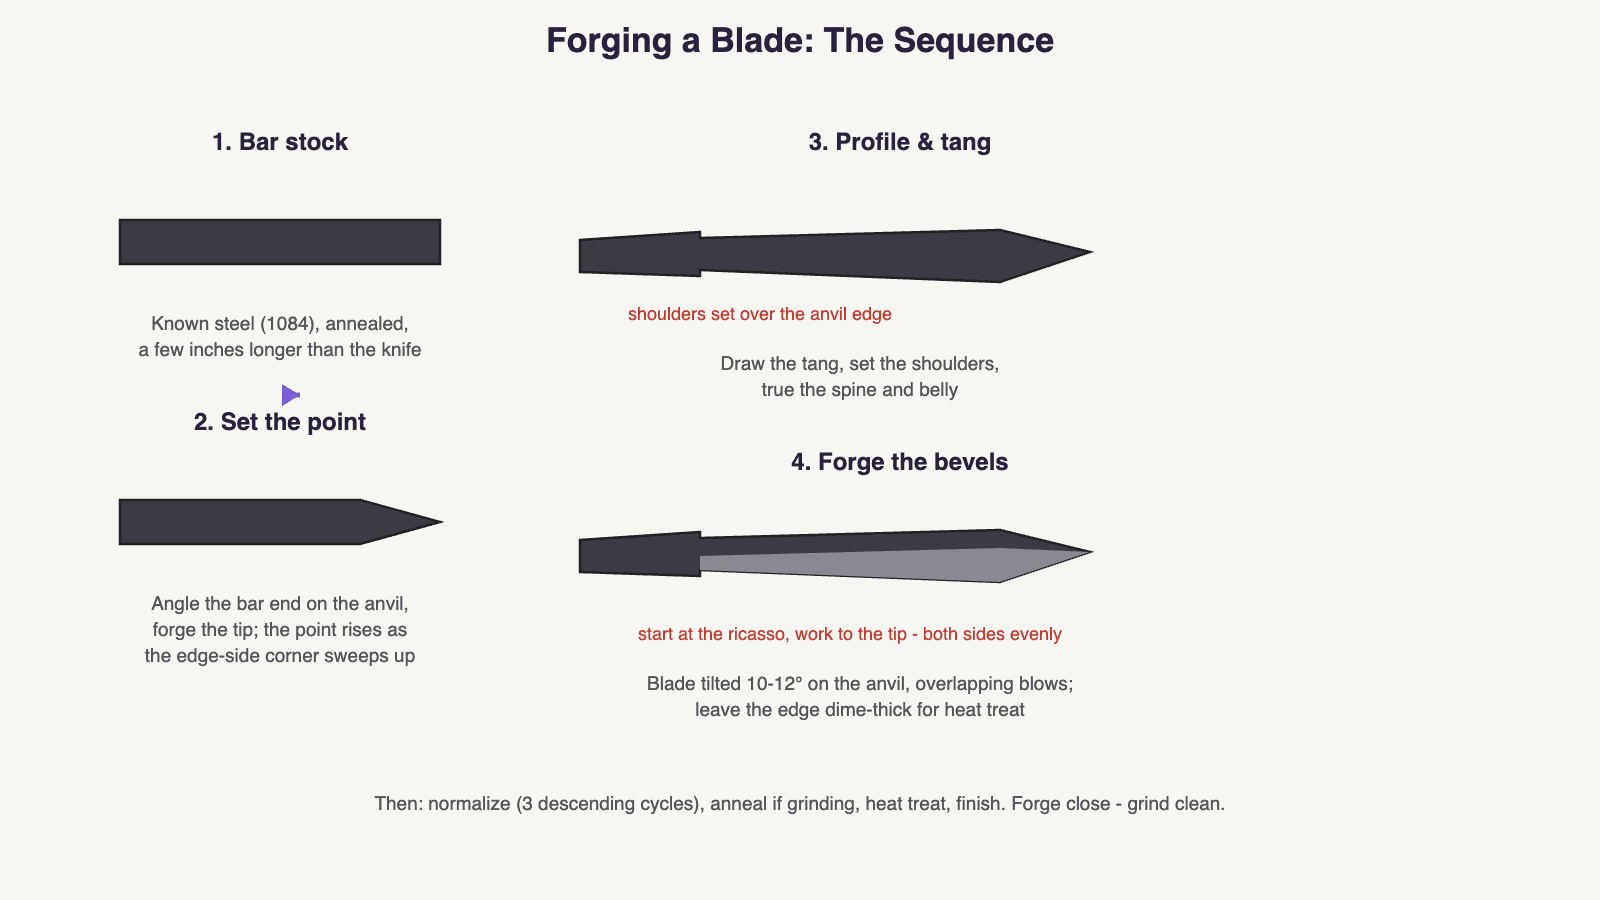
Forge a first blade in sequence: set the point, profile, shoulders and tang, then bevels last at a 10-12 degree tilt, stopping at a dime-thick edge.
3 min readWritten by Rich LinvilleFree to read
Forging a knife is not sculpting with sparks — it’s a sequence, and once you know the sequence, every session has a plan. This guide walks a first forged blade from bar stock to ready-for-heat-treat: a simple 3–4″ drop point from 1084, the steel every smith recommends for exactly this (see why). Gear assumed: the forge and anvil/hammer/tongs from the setup guides.
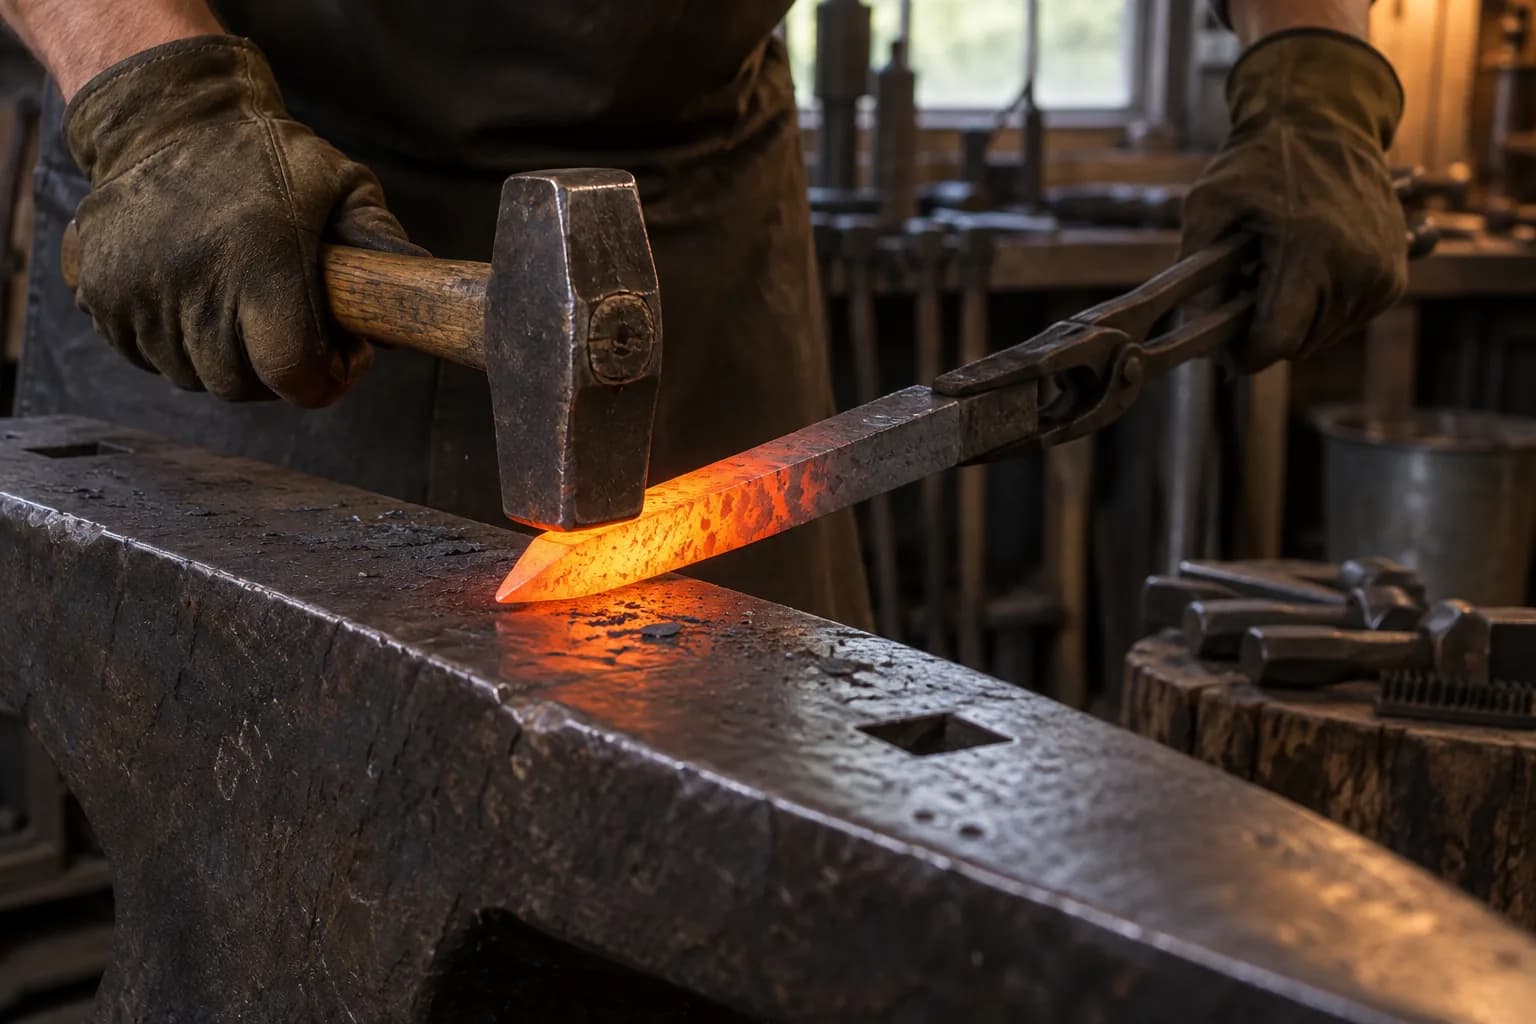
Work steel at bright orange to yellow-orange. Stop hammering at dull red. Steel moves easily at forging heat and tears/cracks when hammered too cold — more first blades die from cold hammering than any other sin. Dim your shop so colors read true, take more heats rather than stretching each one, and remember the forge does the work of softening; the hammer only redirects.
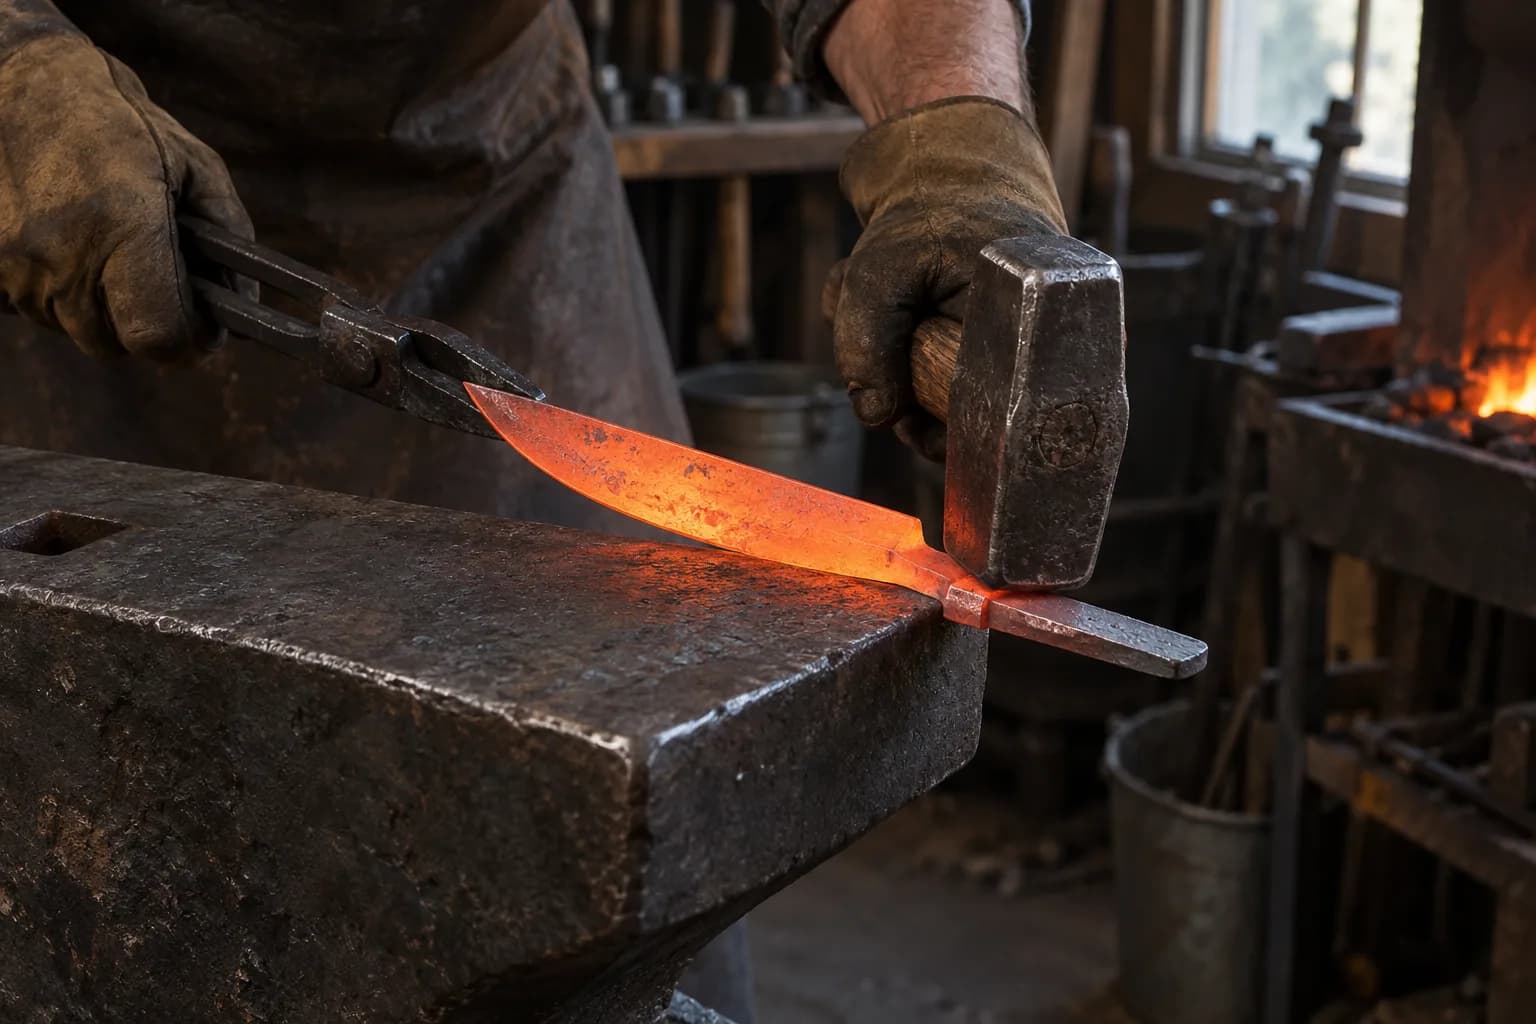
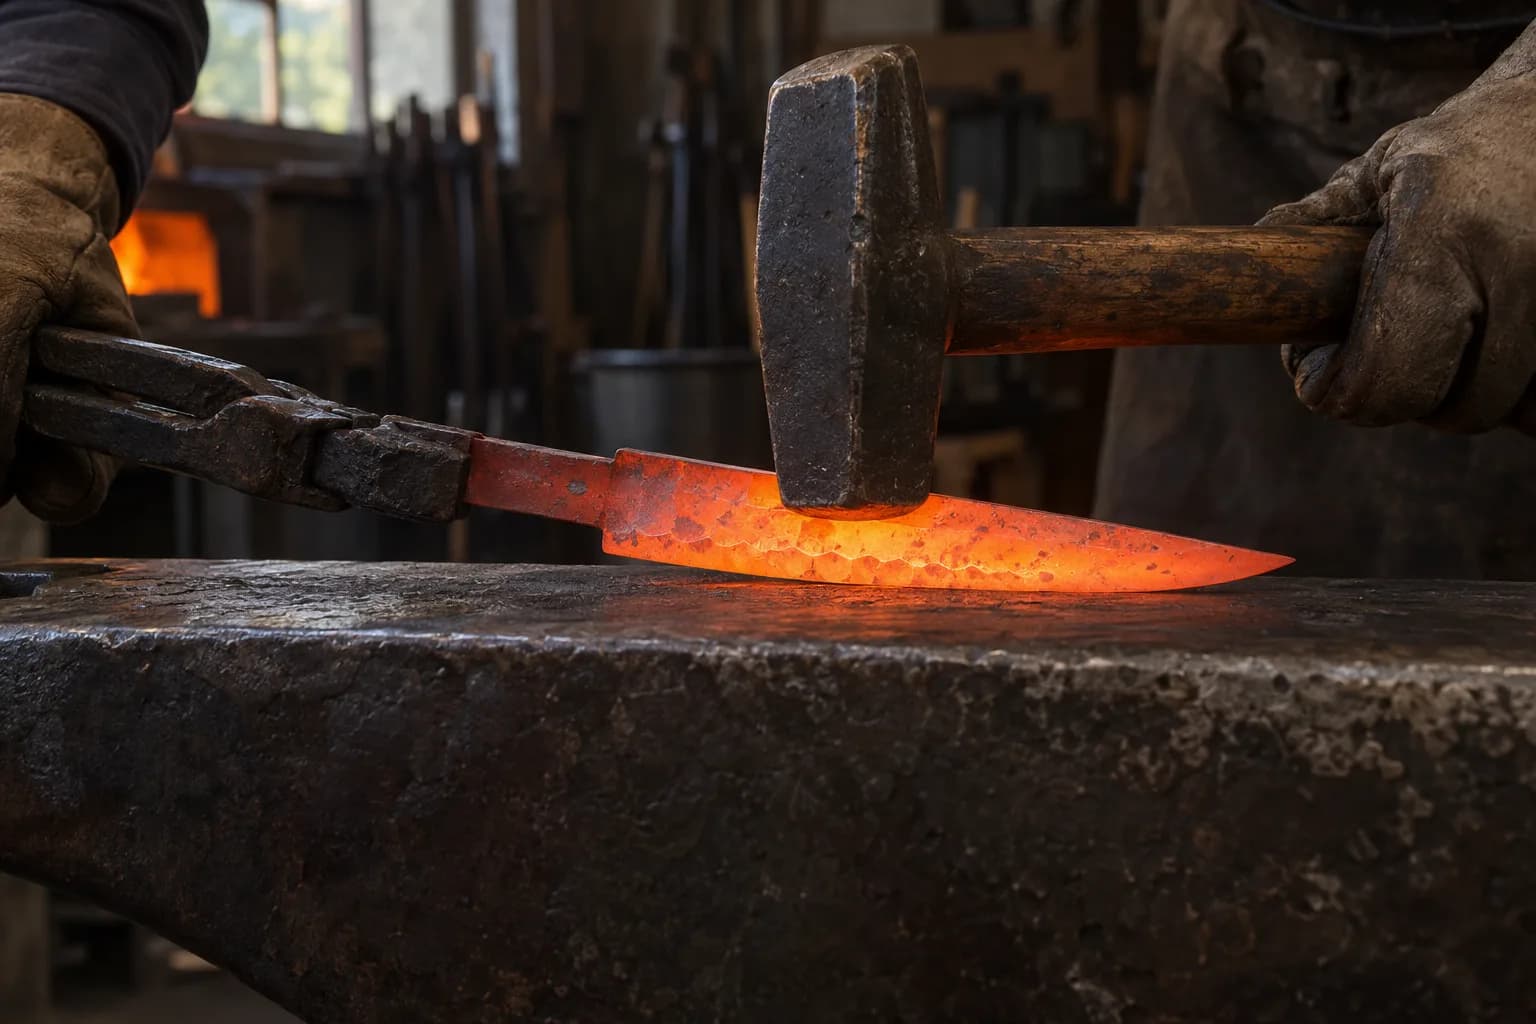
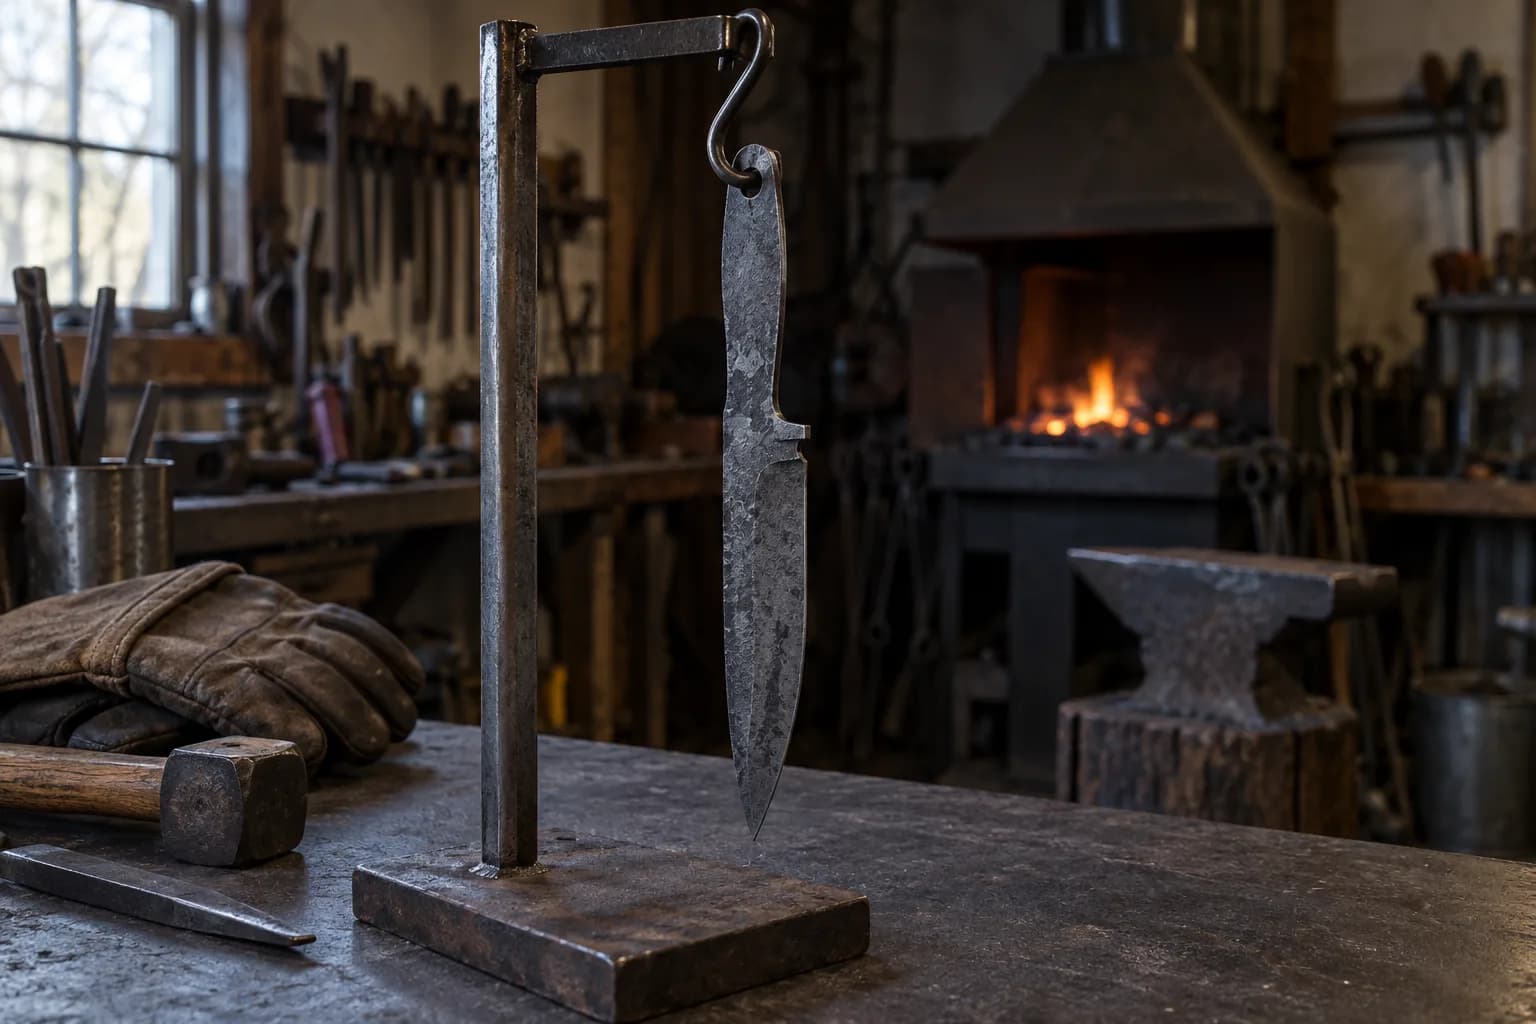
Expect the first one to be thicker than planned, slightly wandery in profile, and absolutely thrilling. Forge close, not perfect — leave yourself grinding stock (forged surfaces also lose a little carbon to the fire; grinding past that decarb layer is part of the plan, covered in the normalizing guide). Blade three will look like you meant it. And if the forging bug bites hard, the damascus section is where these same skills — heat control, hammer accuracy, patience — go to graduate school.
Keep reading
Three more from the same bench.
Every forged blade starts with the same purchase decision, and the good news is it’s gotten cheap: a genuinely usable knifemaking forge now costs less…
Nobody ever quit knifemaking because their anvil was too small — plenty quit because they spent the whole budget on a 250-pound showpiece and had nothing…
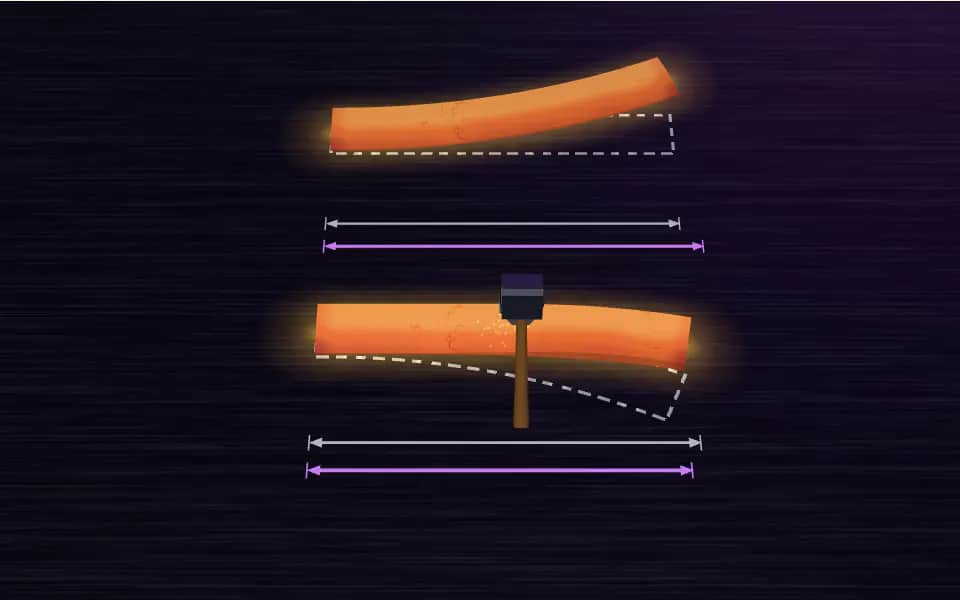
Bevels are where forging stops being blacksmithing and starts being bladesmithing — and where every new smith meets the same betrayal: you forge beautiful…
Same bench
I machine the parts, hand-assemble, track and test Torus grinders in Sterling, Illinois. Most orders ship in seven to ten business days from time of order.

Current dual-axis platform with a fiber-laser-cut 6061 chassis and single-knob tracking.

Current dual-axis platform with a steel chassis, more mass and less vibration.

Prior-design aluminum chassis, 90-degree tilt and 1.5-inch tooling arms.

One-man shop
I answer my own email. Tell me the steel, the machine and what it is doing, and I will tell you what I would try next.