
Beginner Guides
Essential First Tools & Equipment for Knifemaking
It’s easy to look at a fully outfitted professional shop and assume you need all of it to make your first knife. You don’t. Here’s what actually matters…
Beginner Guides
No belt grinder? Hacksaw the profile, file the bevels with a simple jig, hand sand, torch heat treat 1084, then handle and sharpen. Plan on 10-20 hours.
4 min readWritten by Rich LinvilleFree to read
No belt grinder? You can still make a real knife — a genuinely good one. Stock removal knifemaking predates power tools by centuries, and the hand-tool path costs about $100 in equipment, most of which stays useful forever. It’s slower (a knife per weekend instead of per evening), but it teaches flat-grinding fundamentals better than any machine, because every stroke is deliberate. Here’s the full build, hand tools only.
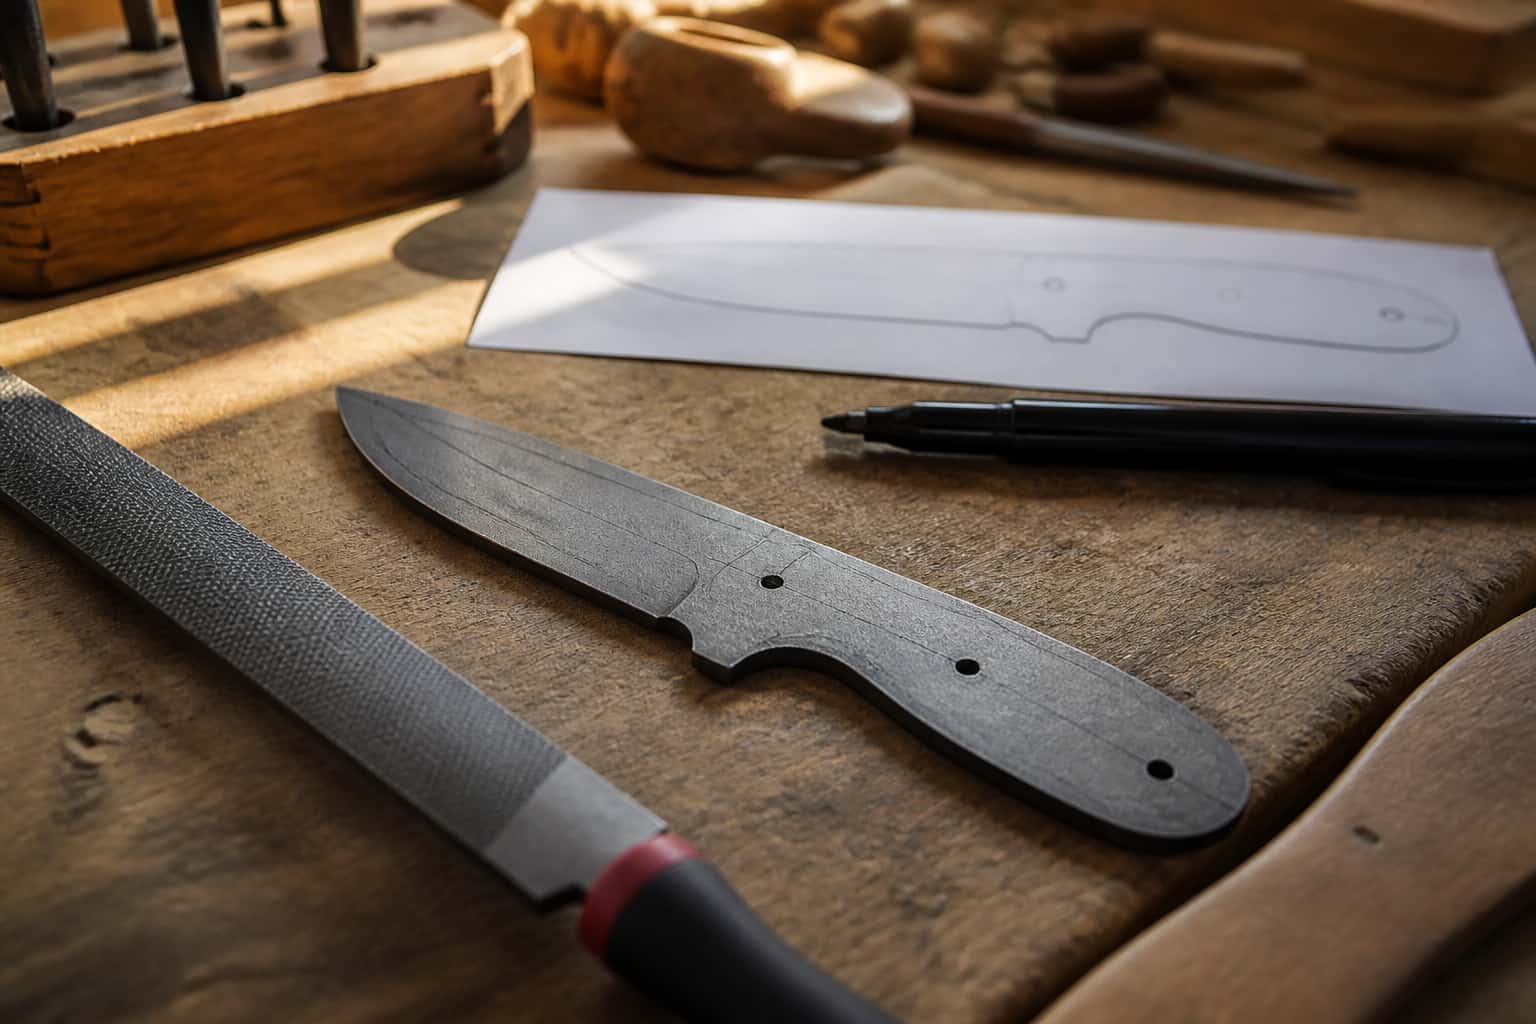
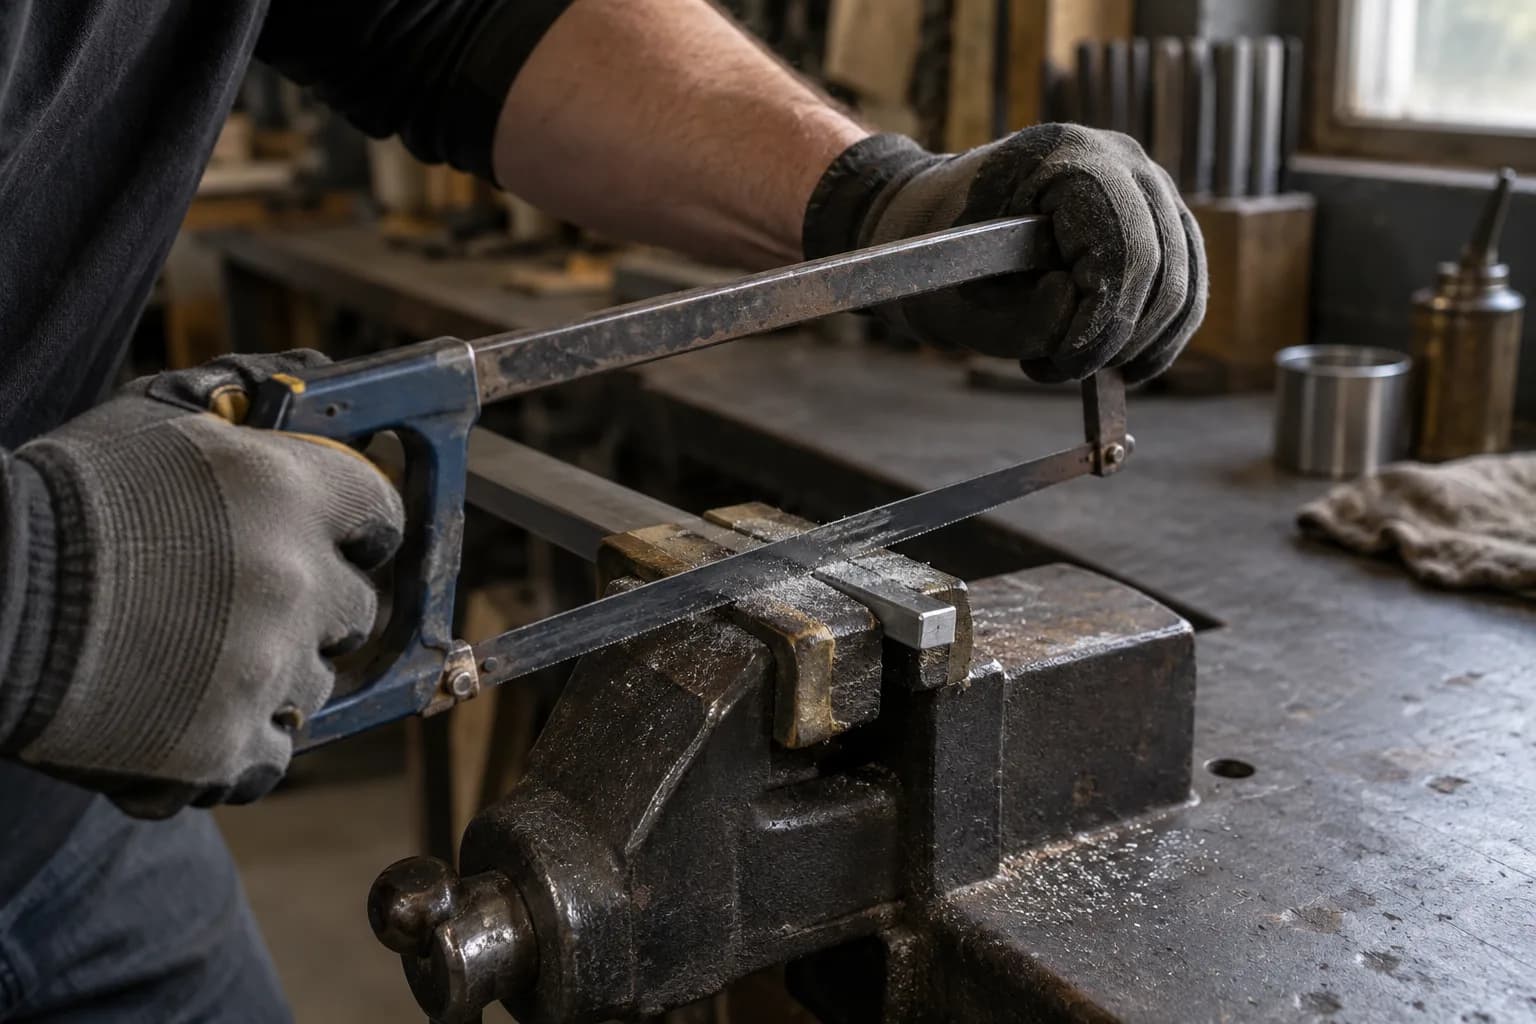
Draw your design, glue it to the steel (see the template guide), and hacksaw close to the line — straight cuts plus relief cuts around curves. Then file down to the line. Round the spine, true the flats, and you’ve got a knife-shaped blank. Drill your pin holes now, while the steel is soft.
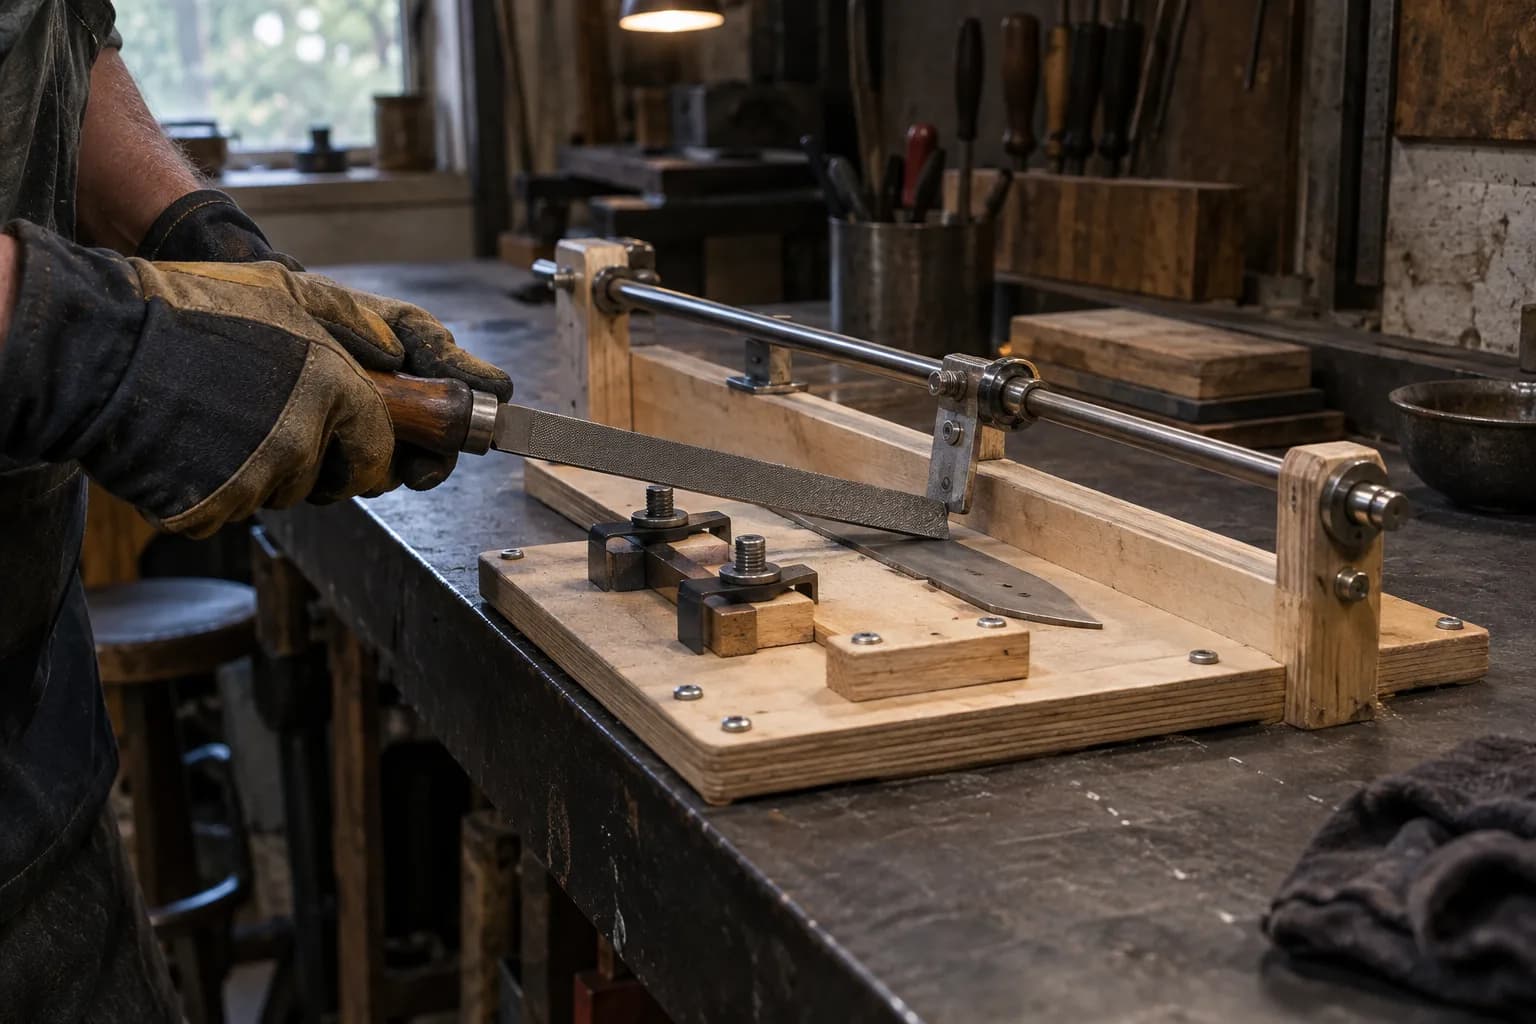
Freehand-filing a consistent bevel is the hard part, and there’s a beginner-proof solution the community has iterated on for a decade (popularized by maker Aaron Gough’s design): the file jig. The concept: your file rides on a guide rod that slides along a raised rail behind the workpiece; the rail height sets the bevel angle, mechanically, on every stroke. Build one from plywood scraps, a length of threaded rod, and hardware-store bits for about $20 — free plans and 3D-printable versions abound online. It turns “years of feel” into “an afternoon of setup,” which is exactly what a first-knife maker needs.
Draw filing technique: files cut on the push stroke only. Push with even pressure, lift or lighten on the return — dragging a file backward under pressure dulls it and clogs teeth (then card it clean often). Work both sides evenly, counting strokes, and stop while the edge is still about a dime thick (0.030″) for heat treat.
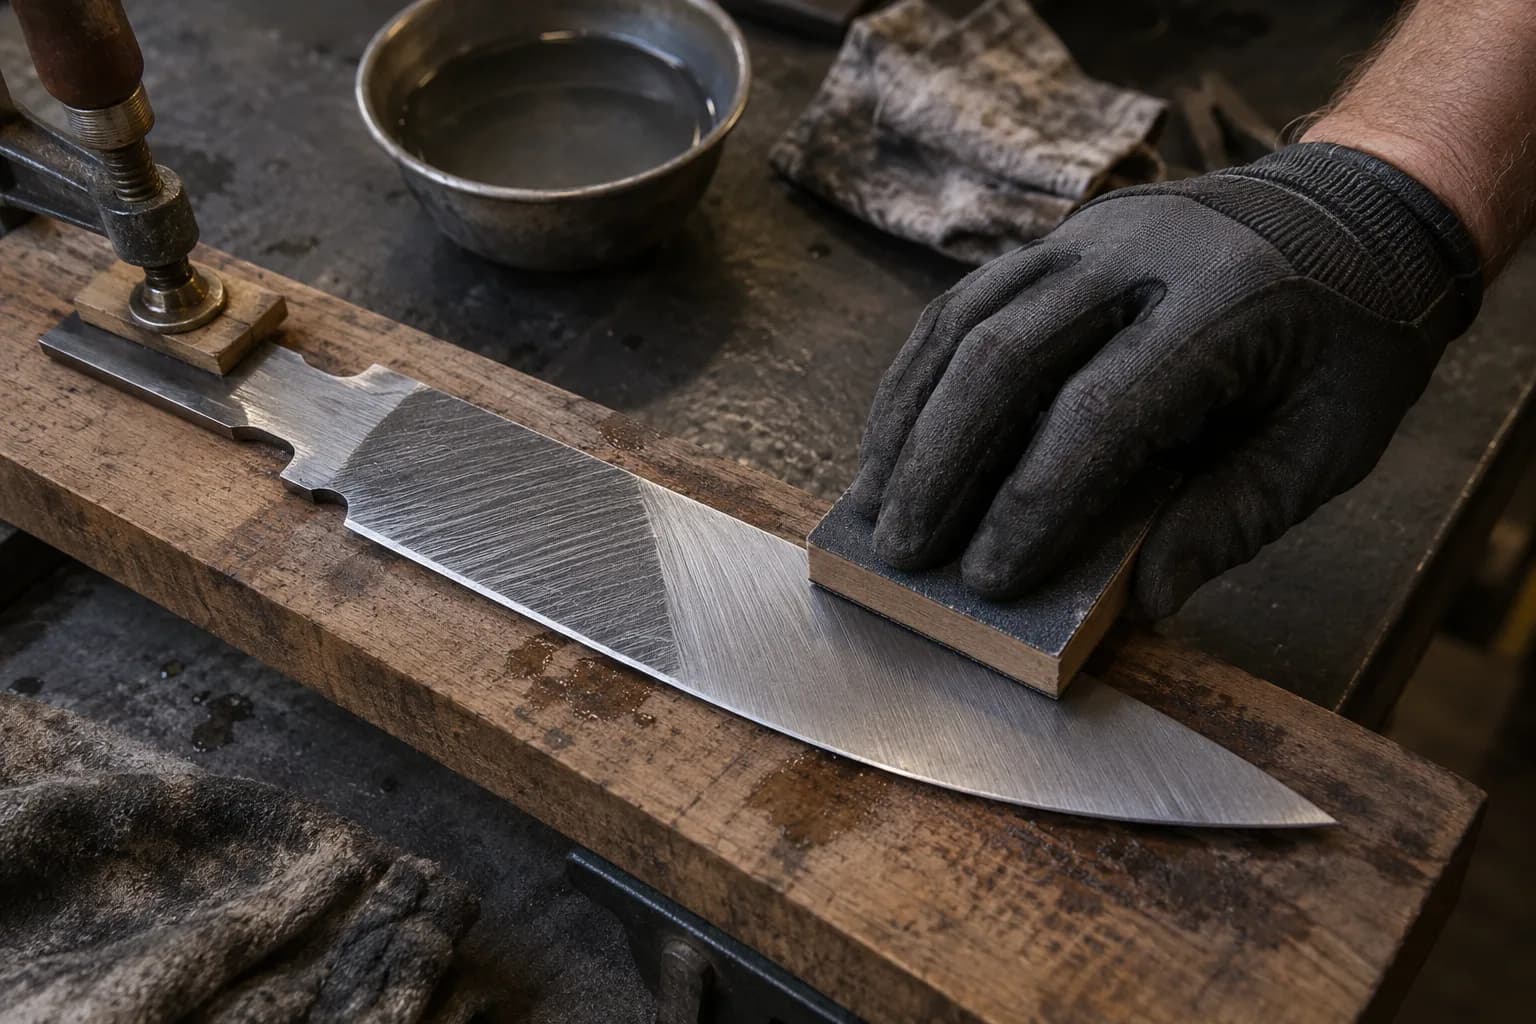
Wrap sandpaper around your hard backing block and work 120 → 220 → 400, changing stroke direction ~45° with each grit so you can see when the previous grit’s scratches are fully gone — the cardinal rule of hand finishing. Chasing every last deep scratch at the next grit up is the classic time-waster; if 220 isn’t removing a 120 scratch quickly, go back down. (This same skill applies to grinder-made knives later — machine-then-hand-sand is how fine finishes get done at any level.)
Nothing about heat treating requires a grinder — a propane torch, magnet, and proper quench oil handle 1084 beautifully. Full walkthrough: Heat Treating Without a Kiln. Remember the sequence: all filing and drilling happens before hardening (files can’t cut hardened steel — that’s the point of hardening), and only sanding, handle work, and sharpening happen after.
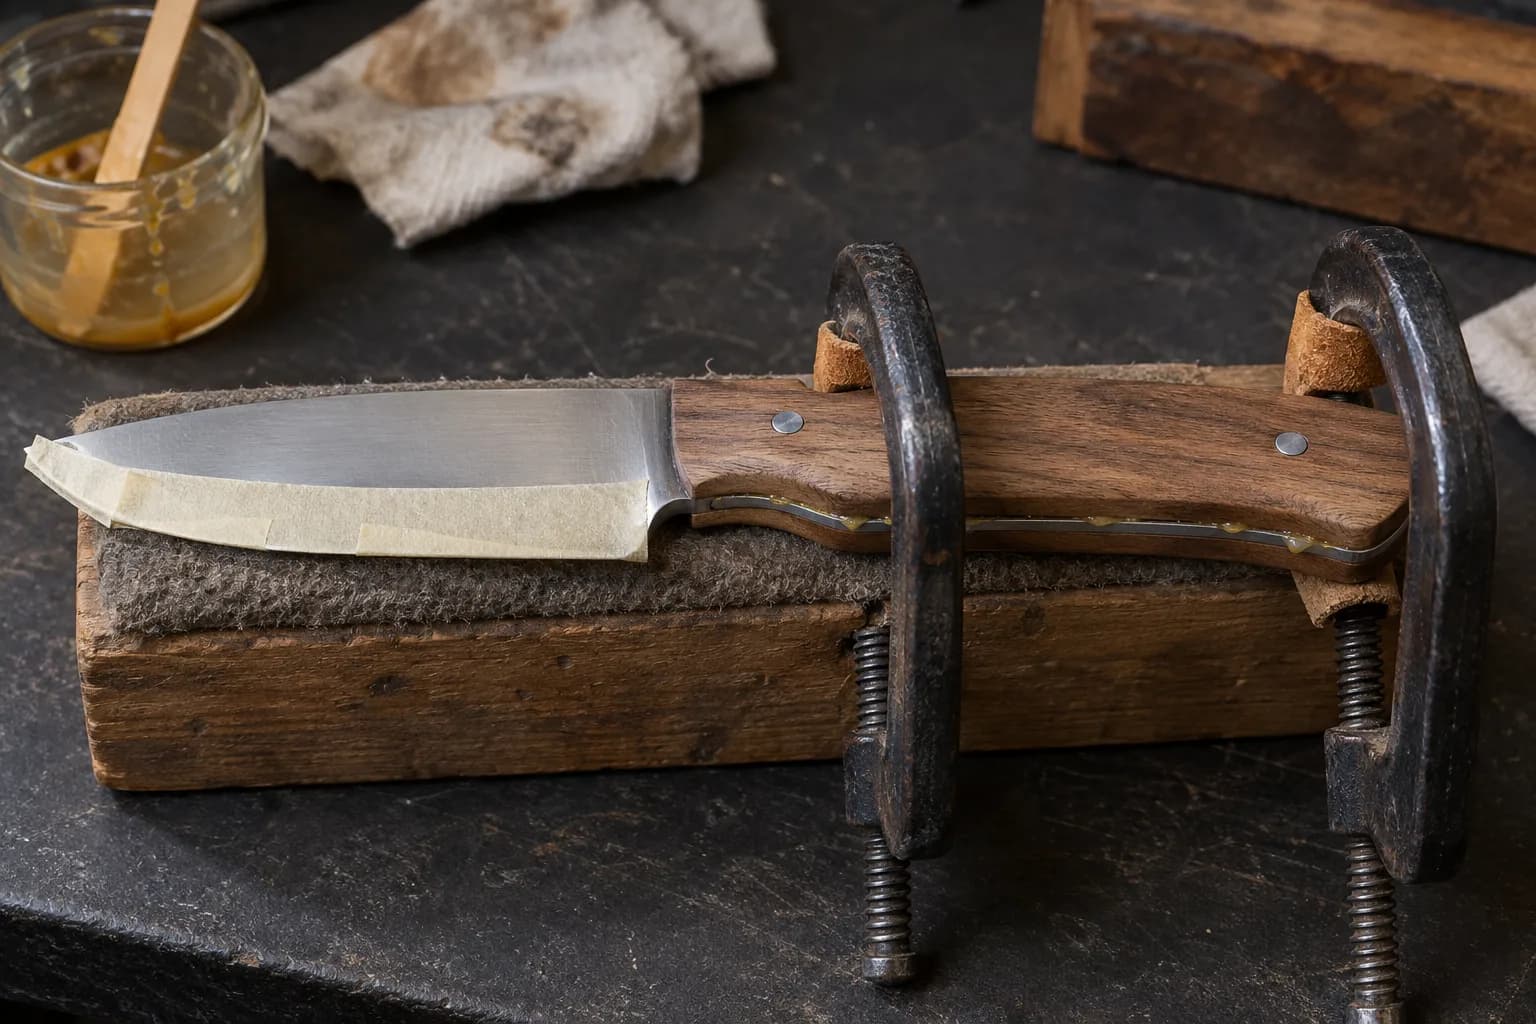
Handle scales, epoxy, and pins need zero power tools — files and sandpaper shape wood and Micarta even more easily than steel. See attaching handle scales and the handle material guide. Finish with your 400-grit hand-rubbed blade, sharpen it properly, and you’ve made a knife with about $100 of tools and your own arms.
Budget 10–20 hours for a first hand-tool knife, and expect a workout. What you get in exchange: flat-grinding instincts (pressure, evenness, watching scratch patterns) that transfer directly to machine grinding, and proof that you love the craft before spending grinder money. The classic progression is exactly this: hand tools first, then — once you know you’re hooked — a 2×72, which turns those 6 hours of bevel filing into 20 minutes and opens up everything from hollow grinds to belt sharpening. When you’re there, the 2×72 buyer’s guide and cost guide cover the decision. Until then: files cut steel just fine, and every stroke is teaching you something.
Keep reading
Three more from the same bench.
It’s easy to look at a fully outfitted professional shop and assume you need all of it to make your first knife. You don’t. Here’s what actually matters…

If you’ve spent any time in knifemaking forums or subreddits, you’ve seen the question a hundred times: “what belt grinder should I buy?” The honest…
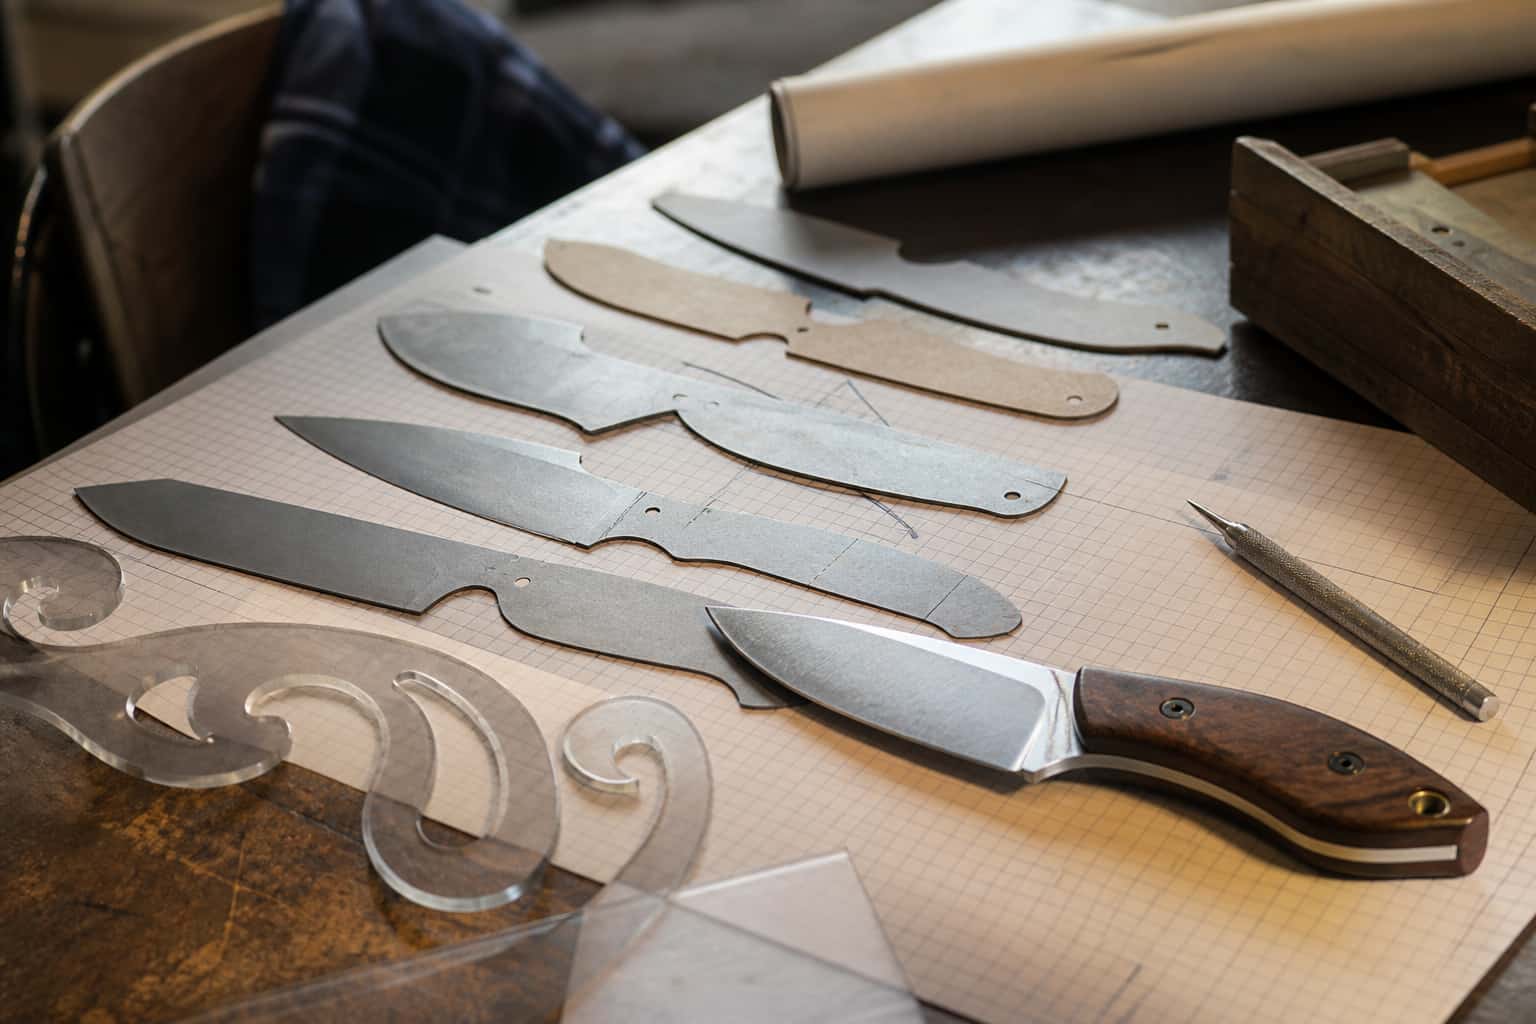
Every knife starts as a drawing before it’s ever a piece of steel. A template, a physical pattern you trace onto stock, is what turns that drawing into…
Same bench
I machine the parts, hand-assemble, track and test Torus grinders in Sterling, Illinois. Most orders ship in seven to ten business days from time of order.

Current dual-axis platform with a fiber-laser-cut 6061 chassis and single-knob tracking.

Current dual-axis platform with a steel chassis, more mass and less vibration.

Prior-design aluminum chassis, 90-degree tilt and 1.5-inch tooling arms.

One-man shop
I answer my own email. Tell me the steel, the machine and what it is doing, and I will tell you what I would try next.