Reference chart
Belt Speed by Task Chart (SFPM)
Set your VFD by the job: working SFPM ranges for hogging, bevel grinding, hardened steel, handles and leather, with percentages for a direct-drive 2x72 setup.
Live tool
Answer four questions - use, rust care, heat treat setup, sharpening gear - and get your three best-fit knife steels from the 33-steel database.
Run it
Thirty-three steels in the database is wonderful for depth and paralyzing for a decision. Answer four questions and get your three best-fit steels — each linked to its full page with composition, ratings, heat treat and grinding notes.
Your numbers
The arithmetic
The selector scores every steel in the database against your answers: what the blade is for, whether rust care is acceptable, what your heat-treat setup can actually harden (a forge hardens carbon steel and the low-carbide stainless like AEB-L, 14C28N and Nitro-V, a point or two softer than a kiln gets them; high-carbide stainless like MagnaCut and M390 needs a kiln), and whether your stones can handle high-carbide steels. The scoring mirrors the advice in How to Choose Your First Knife Steel and Steel Selection by Application — this is the same logic, automated.
Browse more tools in the Calculators section.
More shop math
Eight tools, all free, all running in the page.
Set your VFD by the job: working SFPM ranges for hogging, bevel grinding, hardened steel, handles and leather, with percentages for a direct-drive 2x72 setup.
Find your 2x72's surface speed in SFPM from drive wheel diameter and motor RPM, with optional VFD frequency, and see how hard a belt cuts and how hot it runs.
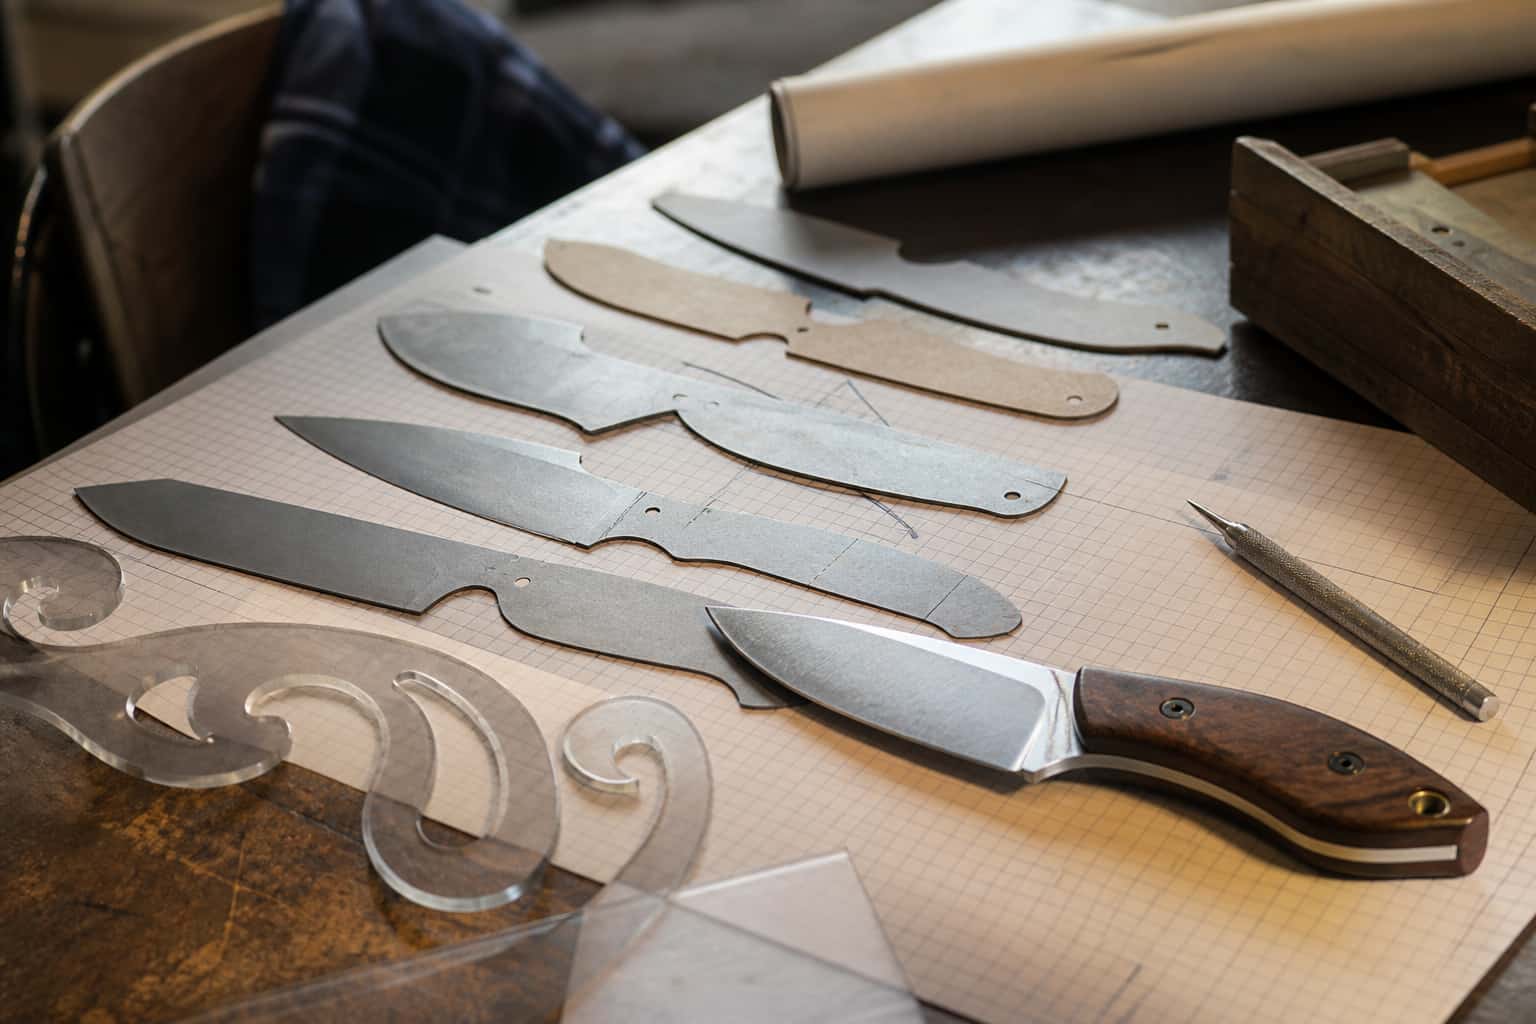
Turn stock thickness, edge thickness and bevel angle into the scribe height for a flat grind, with notes on reading the answer and using it at the machine.
Same bench
Speed, angle and pressure only mean something on a grinder that holds its setting. I machine the parts, hand-assemble, track and test Torus grinders in Sterling, Illinois.
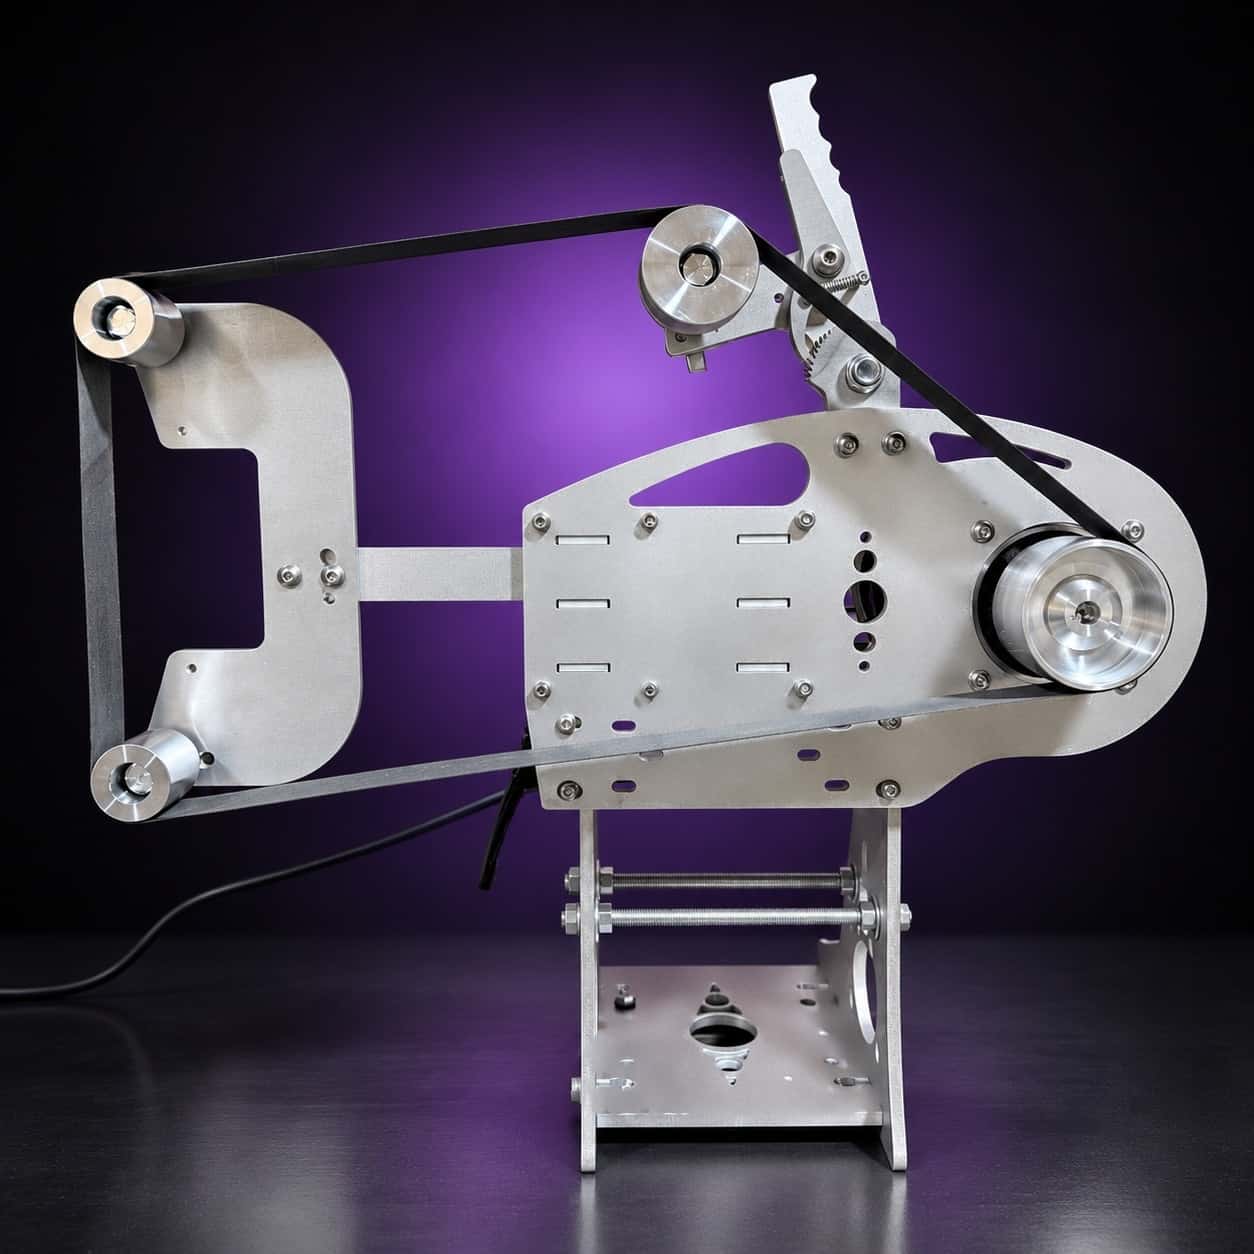
Current dual-axis platform with a fiber-laser-cut 6061 chassis and single-knob tracking.
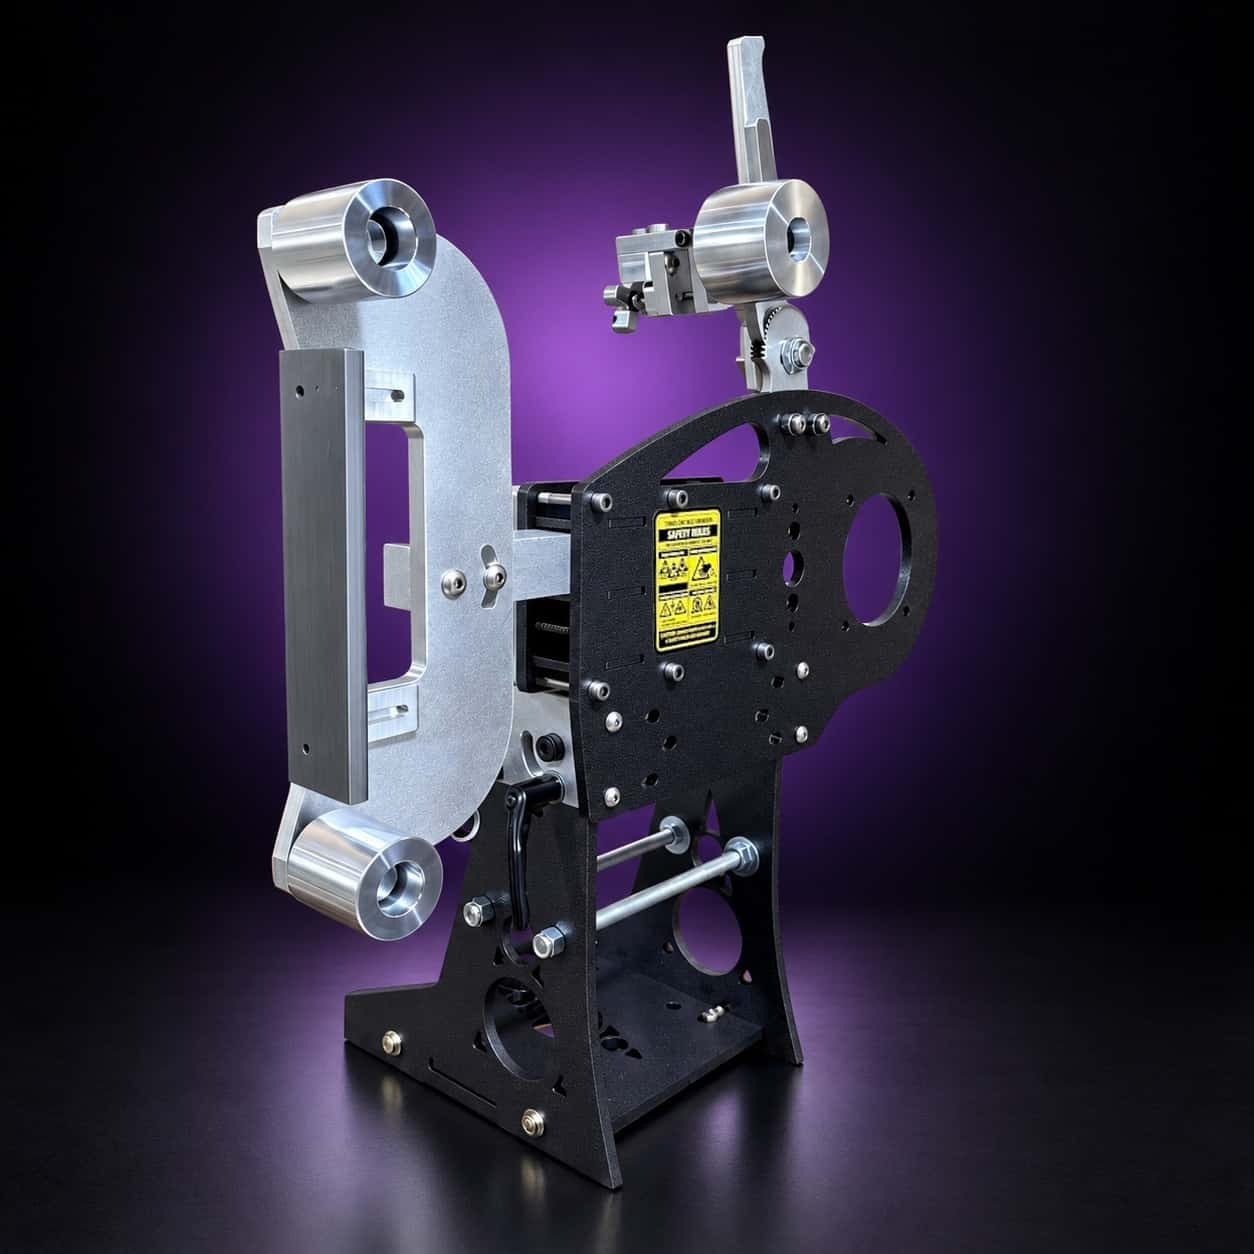
Current dual-axis platform with a steel chassis, more mass and less vibration.
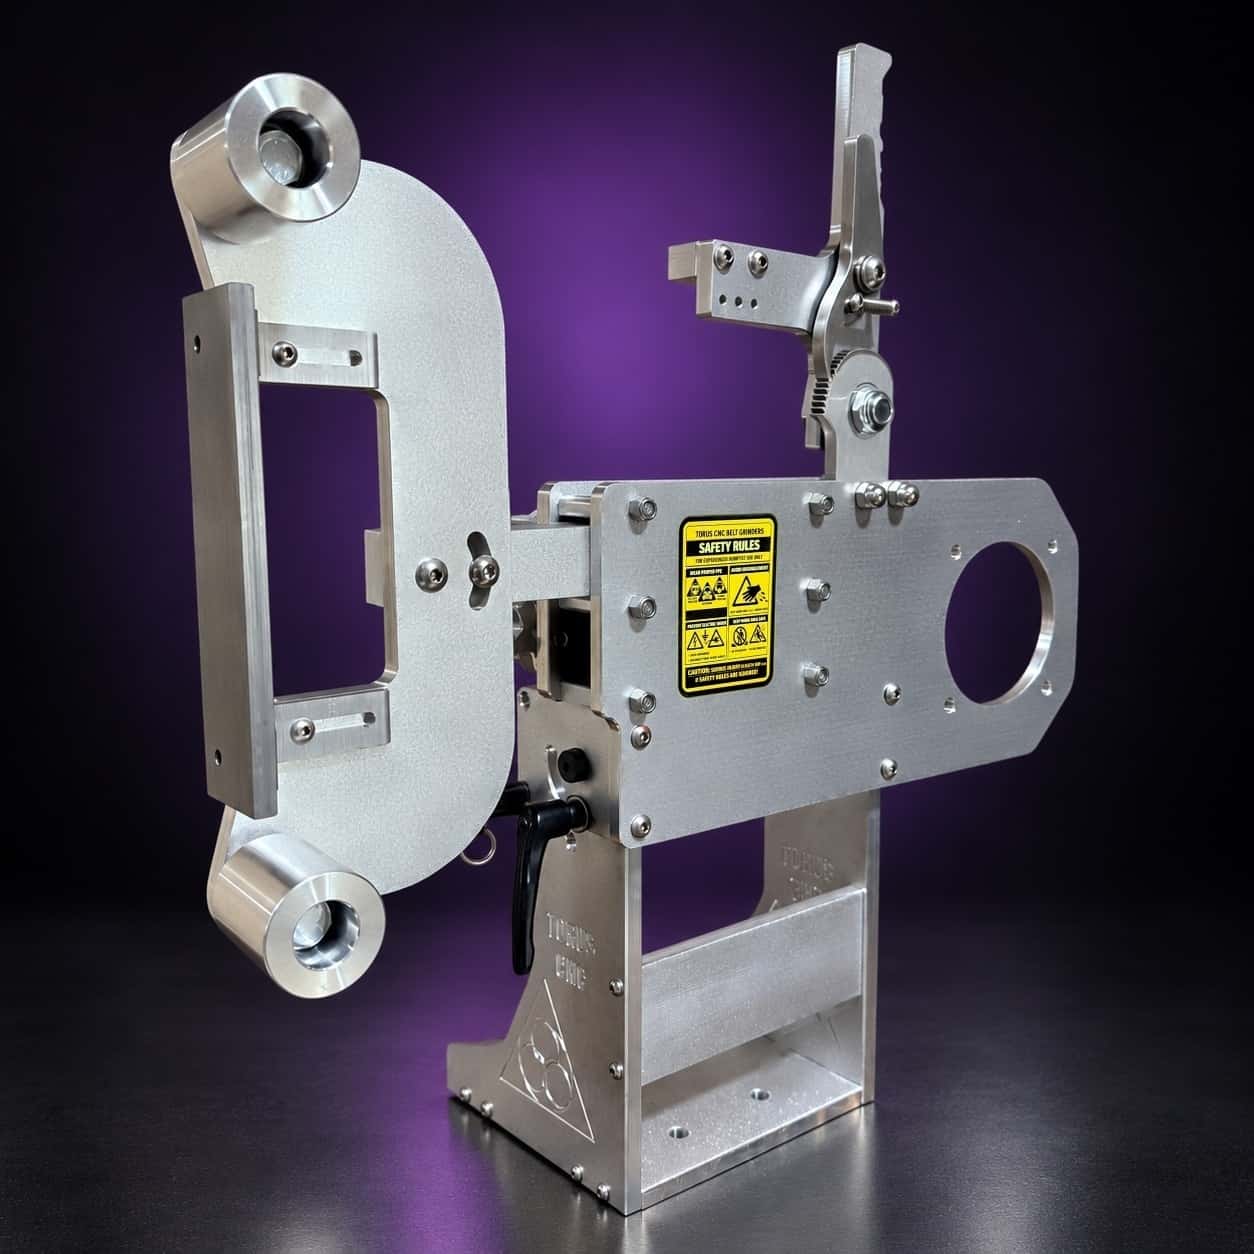
Prior-design aluminum chassis, 90-degree tilt and 1.5-inch tooling arms.
One-man shop
Send me your wheel size, motor and VFD details so I can compare them with the belt-speed calculation.