

Abrasives
Belt Buyer’s Guide: Which Abrasives to Actually Buy
Belts are the single biggest recurring cost in this hobby, and buying the wrong ones wastes money twice: once on belts that wear out fast, and again on…
Abrasives
Surviving 9% vanadium: grind S90V annealed with fresh ceramics, use feather pressure and constant dunks once hard, and sharpen with diamond or CBN stones.
1 min readWritten by Rich LinvilleFree to read
S90V is the steel that teaches makers what vanadium carbide really means: nine percent of the bar is particles harder than most of your abrasives. Every hour the edge lasts in cardboard was pre-paid at the grinder and the bench. Here is how to pay efficiently.
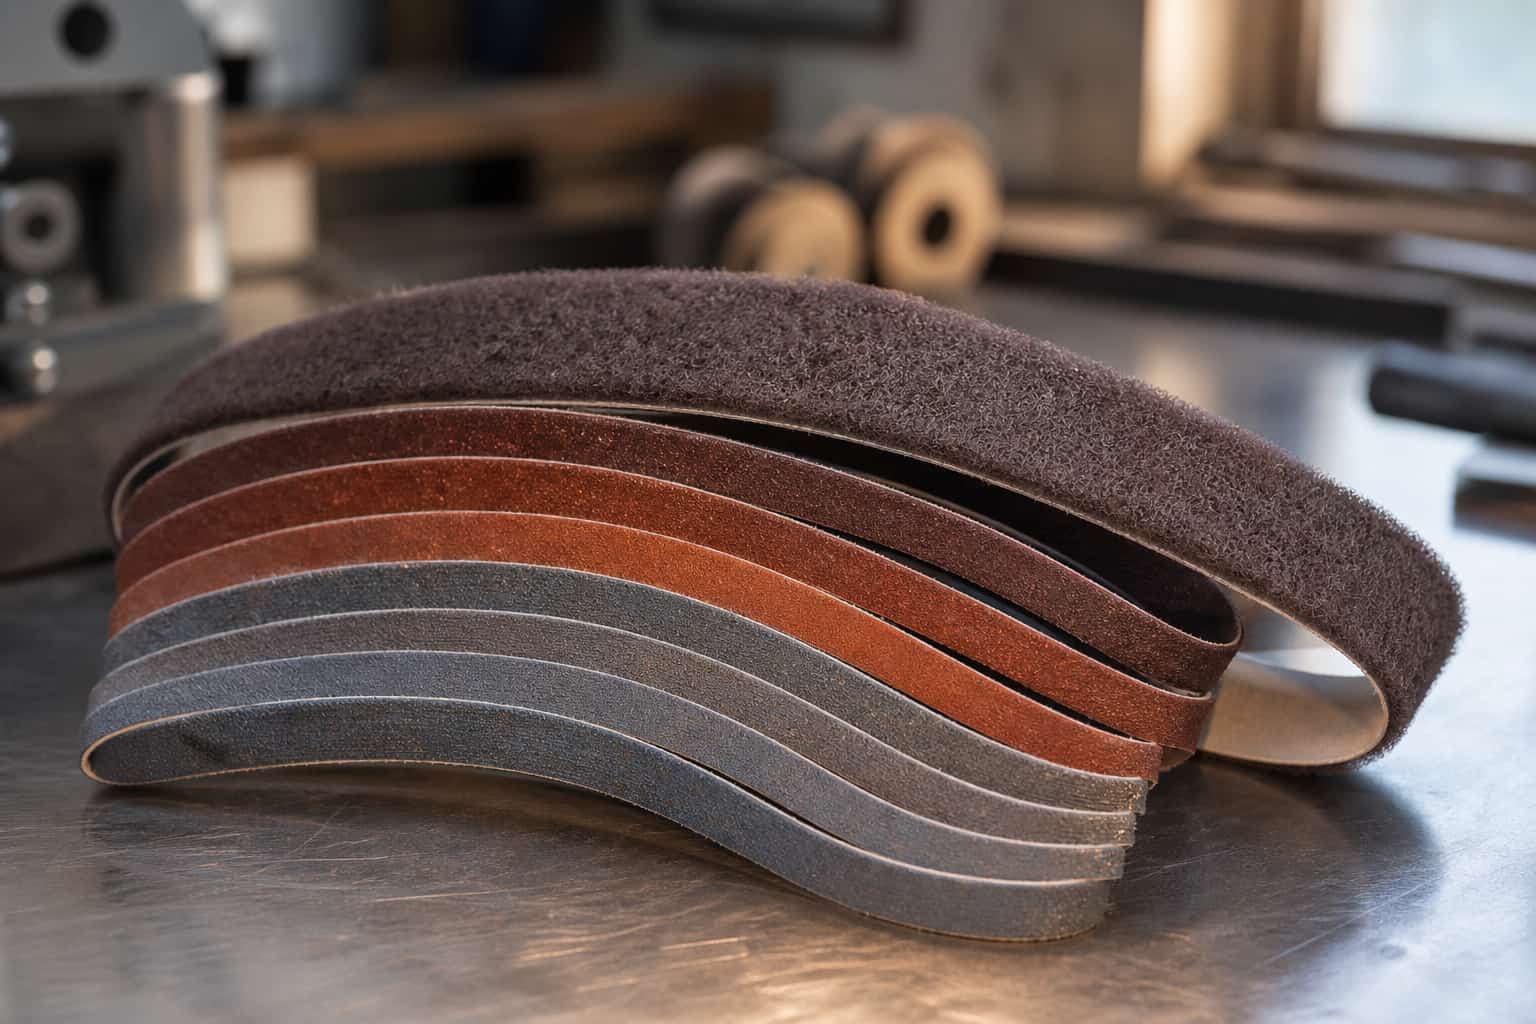
Premium ceramic belts, replaced early and often — S90V kills the cutting edge of a ceramic faster than any steel on this site, and a half-worn belt on this steel is a heat gun. Hog everything possible in the annealed state (profile, bevels to 80-90%, drilling — carbide bits live longer); after heat treat at 59-61 HRC, sharp 120-grit ceramics with feather pressure and constant dunking. Finishing: structured abrasives, low expectations, and acceptance that hand-sanding S90V is a hobby for people who hate themselves — machine-finish this steel.
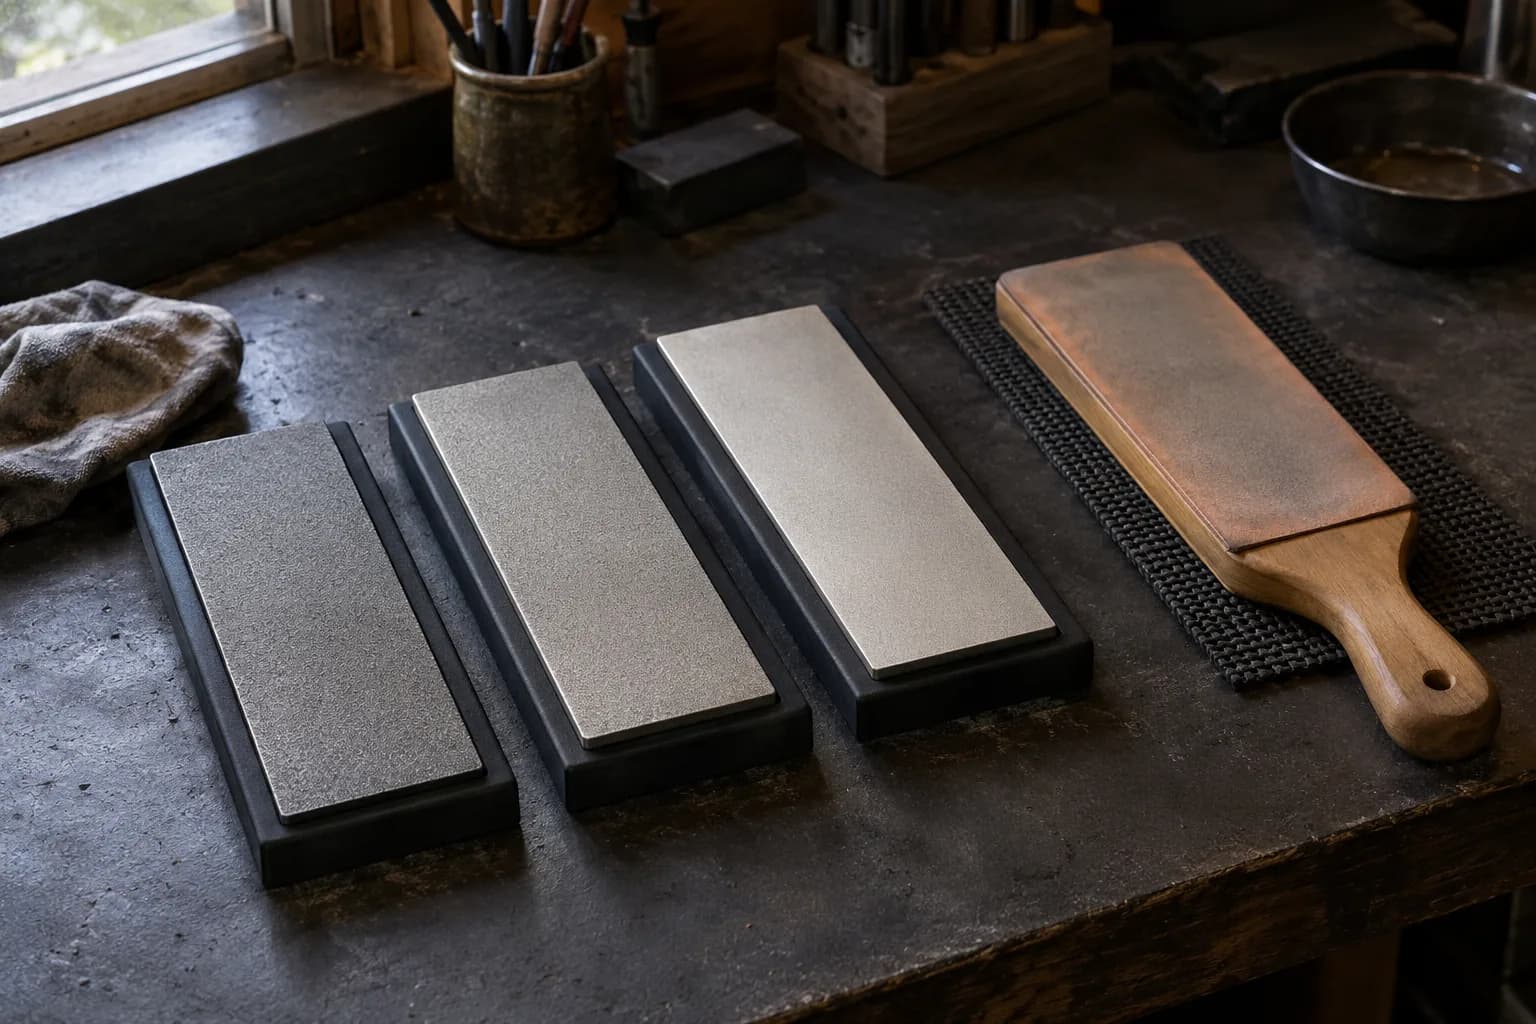
Diamond or CBN, mandatory — not preferred, mandatory. Conventional stones burnish the matrix and leave the carbides standing proud: the edge feels sharp-ish and performs dull. A coarse-medium-fine diamond progression plus diamond-emulsion strop delivers the edge the spec sheet promised; angles 18-20 dps. Sell every S90V blade with the diamond conversation, or field the ‘won’t sharpen’ email later — the physics live in the sharpening guide and the microbevel guide (a microbevel is extra useful here: touch-ups without fighting the full bevel).
Double the belts, double the bench time of M390 — which was already half again a normal stainless. Quote build hours accordingly; S90V flagships are priced like flagships for shop-floor reasons, not marketing ones.
Keep reading
Three more from the same bench.
Belts are the single biggest recurring cost in this hobby, and buying the wrong ones wastes money twice: once on belts that wear out fast, and again on…
Sharpening is where knifemaking gets humbled: you can grind a flawless blade and still hand someone a knife that won’t slice paper. The good news …
M390 earns its benchmark status at the cutting board and collects the bill in the shop: its vanadium and chromium carbides resist your abrasives exactly…
Same bench
I machine the parts, hand-assemble, track and test Torus grinders in Sterling, Illinois. Most orders ship in seven to ten business days from time of order.

Current dual-axis platform with a fiber-laser-cut 6061 chassis and single-knob tracking.

Current dual-axis platform with a steel chassis, more mass and less vibration.

Prior-design aluminum chassis, 90-degree tilt and 1.5-inch tooling arms.

One-man shop
I answer my own email. Tell me the steel, the machine and what it is doing, and I will tell you what I would try next.