Knife Making
Precision Grinding Techniques for 2×72: Hardened Dies & Punches
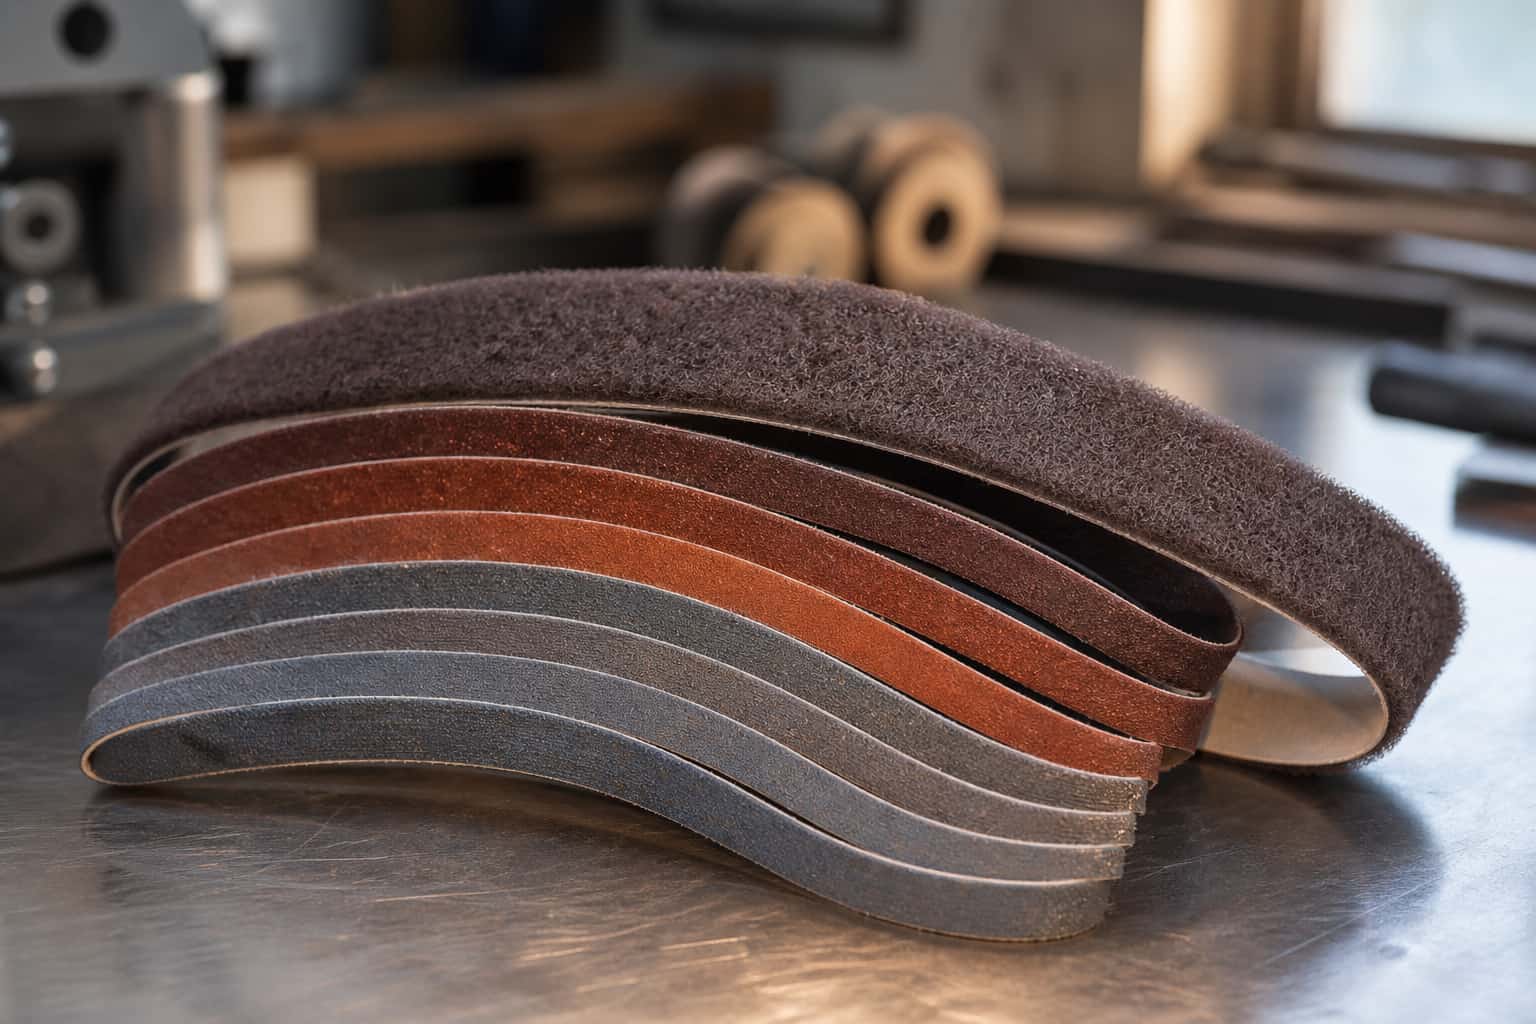
Hardened tool steel does not care how good your grinder is unless the belt, speed and fixture are right. Here is how I grind dies and punches on the 2×72: ceramic belts, slow speed, coolant, a rigid rest, measuring.
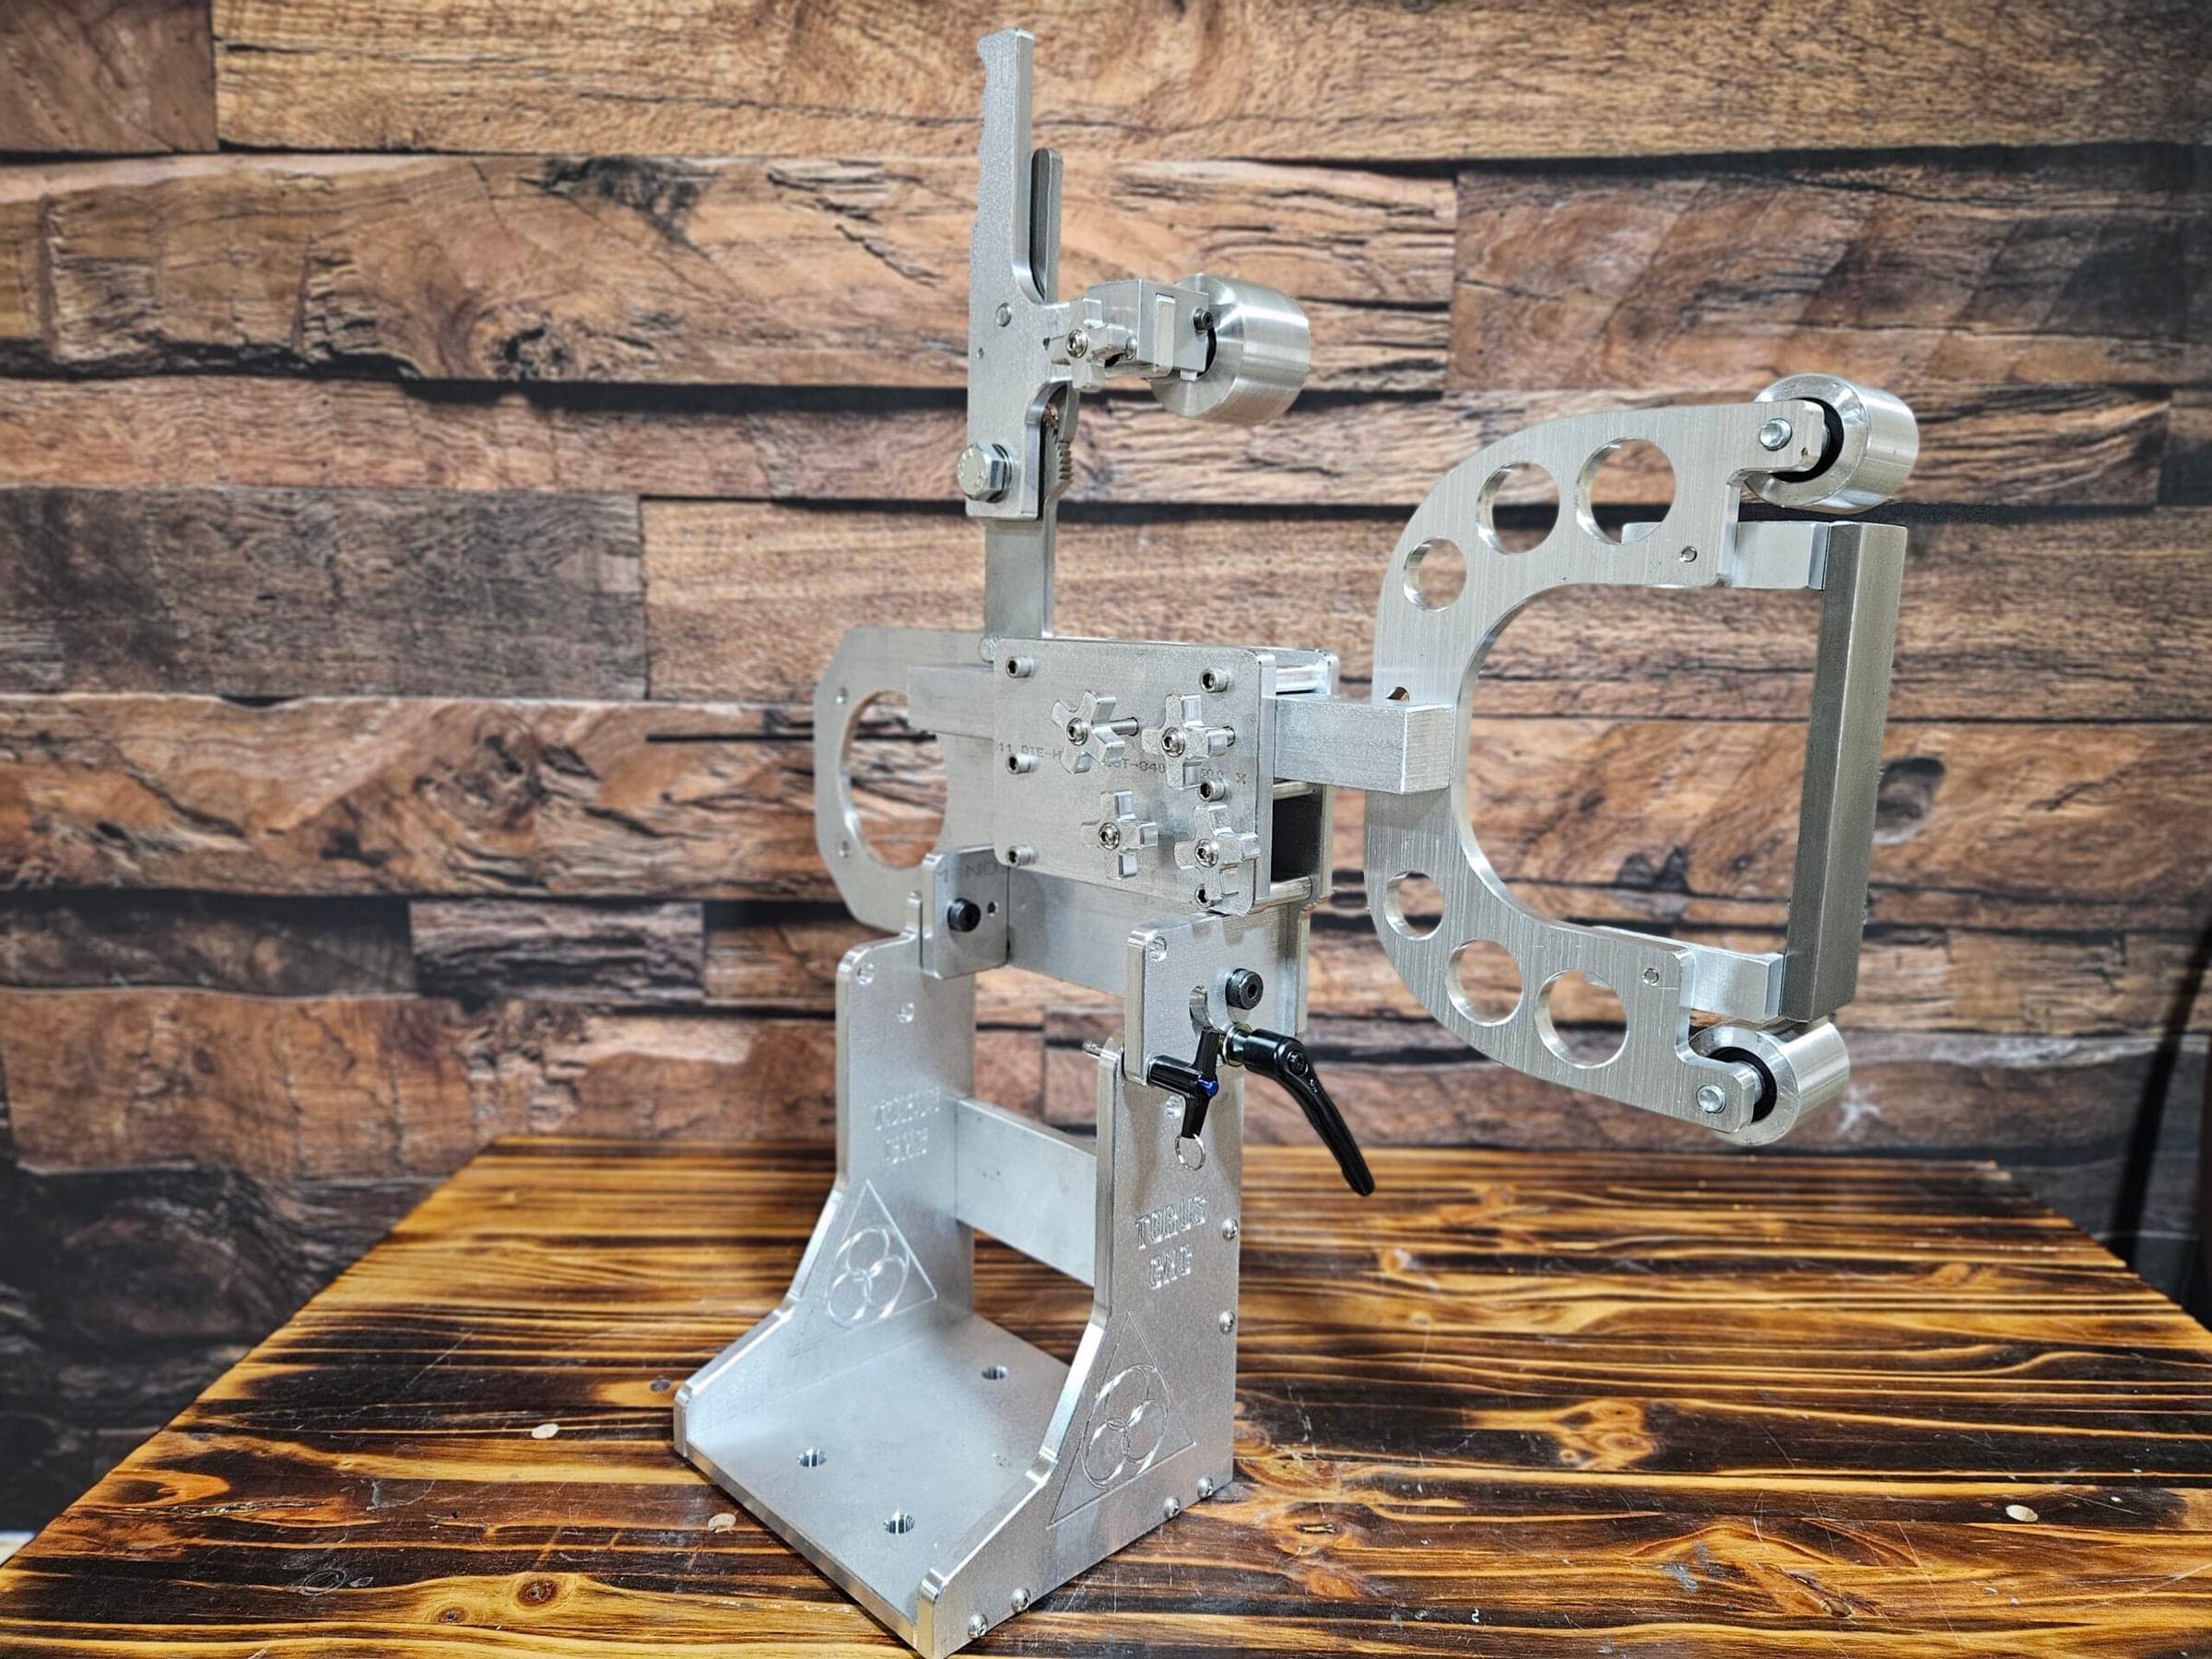
A 2×72 is not only a knife tool. Toolmakers and fabricators use the same machine to dress hardened dies and punches, and the rules are stricter: the steel is already hard, the tolerances are tight, and heat ruins the part. Here is how I grind hardened tooling on the 2×72: sharp ceramic belts, slow belt speed, coolant, a rigid work rest, and a micrometer between passes.
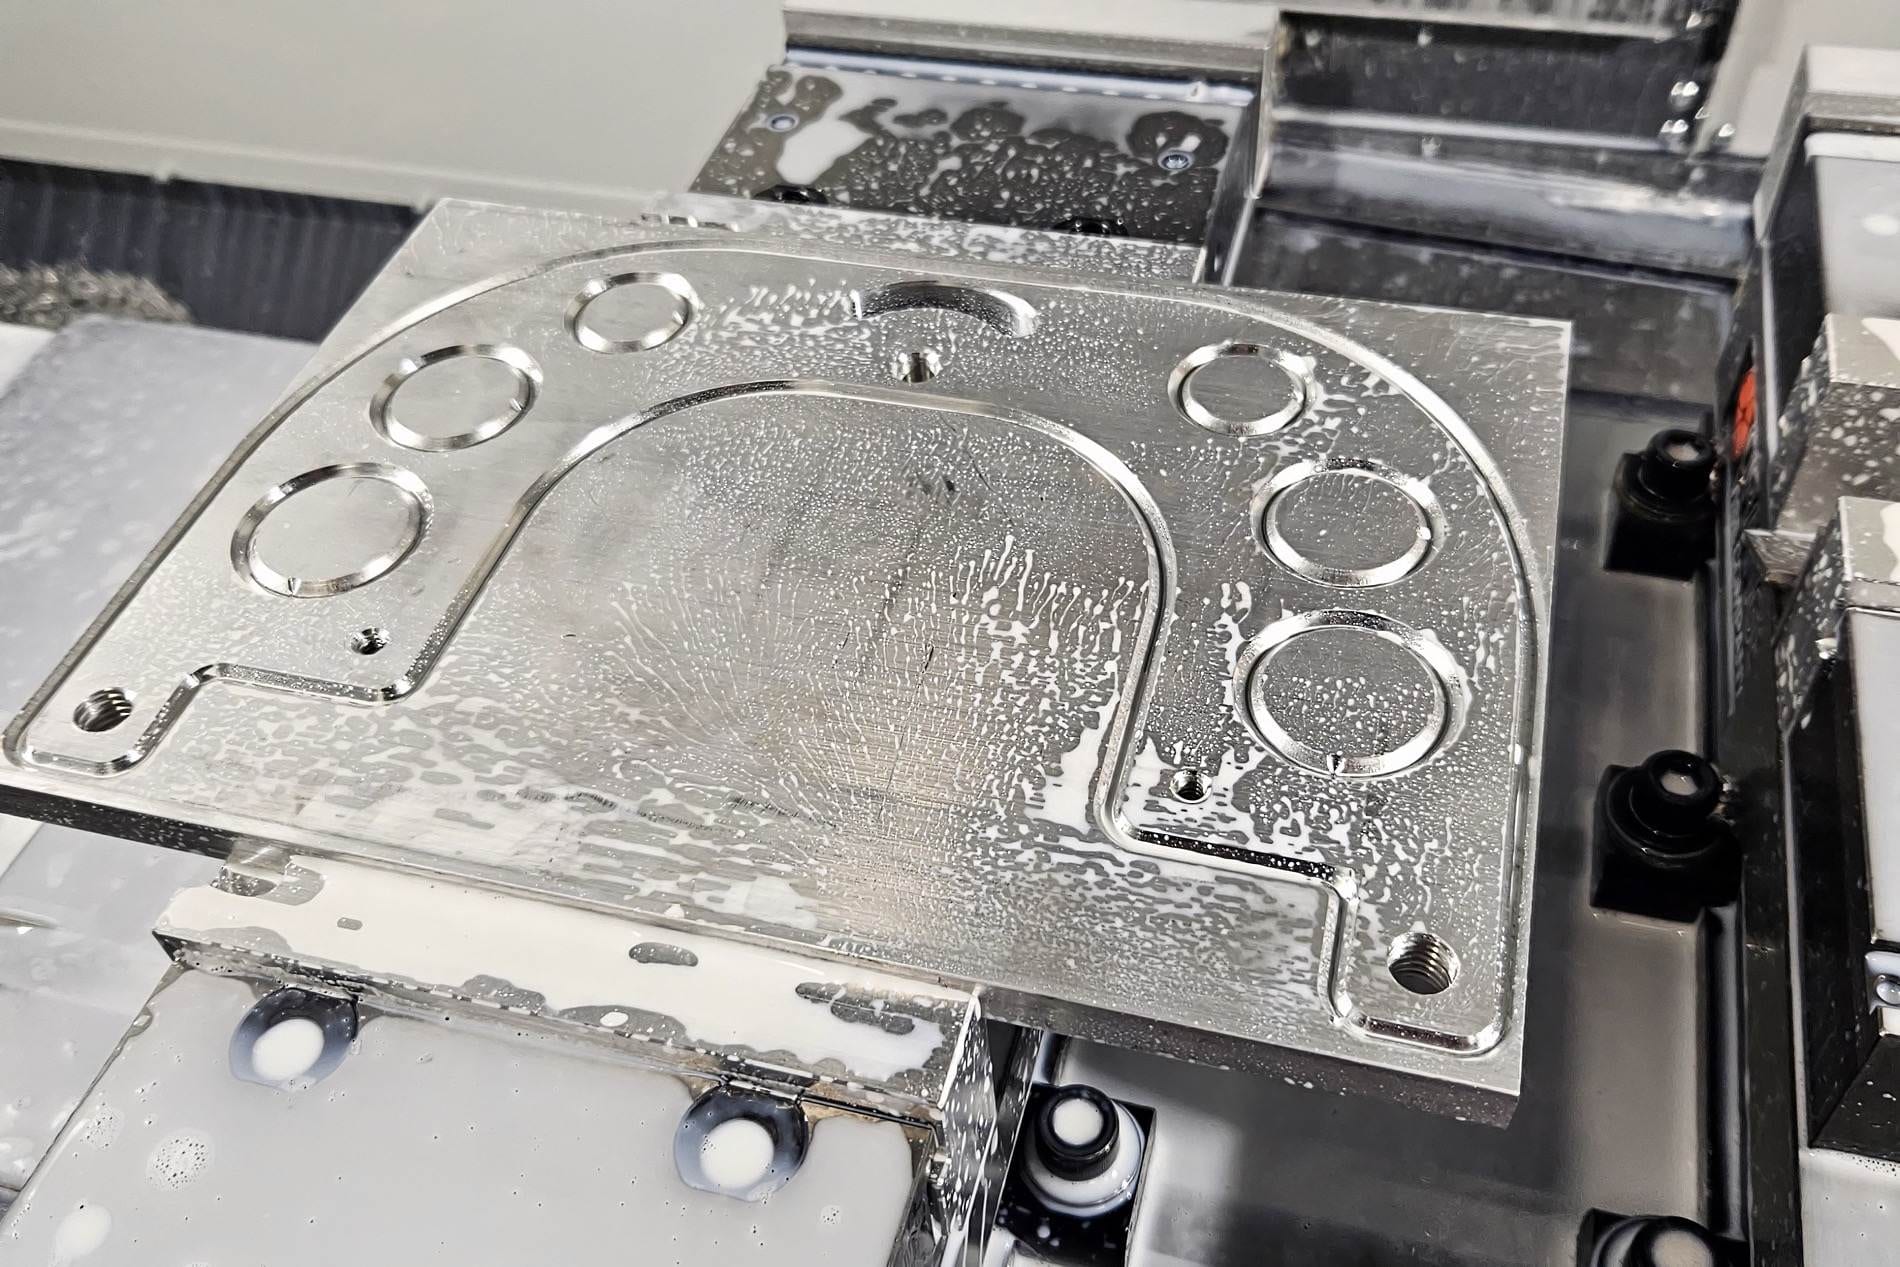
Hardened dies and punches are subjected to extreme conditions during their operational life, including high pressures and abrasive materials. By employing precision grinding techniques, manufacturers can ensure that these tools maintain their integrity over time. The result is a reduction in wear and tear, leading to fewer replacements and lower overall production costs.
Key Takeaways
- Precision grinding is crucial for achieving tight tolerances and uniform surface finish in hardened dies and punches for 2×72 applications.
- Selecting the right grinding wheel is essential for efficient and effective grinding of hardened dies and punches.
- Coolant plays a critical role in precision grinding by reducing heat and friction, and improving surface finish and tool life.
- Consistent grinding pressure is necessary for maintaining uniform surface finish and achieving tight tolerances in precision grinding.
- Post-grinding inspection and quality control are important steps to ensure the accuracy and quality of hardened dies and punches in 2×72 applications.
Selecting the Right Grinding Wheel for Hardened Dies & Punches
I pick the wheel for the die material, the finish I need, and the operation I am running.
For instance, diamond wheels are often preferred for grinding hard materials due to their superior hardness and wear resistance. In addition to material compatibility, the grit size of the grinding wheel plays a crucial role in achieving the desired surface finish. Finer grits are typically used for finishing operations, while coarser grits are more suitable for stock removal.
It is also essential to consider the bond type of the wheel, as this affects its durability and performance under various conditions. A well-chosen grinding wheel not only enhances efficiency but also contributes to achieving tighter tolerances and better overall quality in hardened dies and punches.
The Role of Coolant in Precision Grinding for Hardened Dies & Punches
Coolant plays a vital role in the precision grinding process, particularly when working with hardened dies and punches. The primary function of coolant is to dissipate heat generated during grinding, which can adversely affect both the workpiece and the grinding wheel. Excessive heat can lead to thermal damage, altering the hardness of the material and potentially compromising its structural integrity.
By using an appropriate coolant, manufacturers can maintain optimal temperatures throughout the grinding process, ensuring that both the tool and workpiece remain within acceptable limits. Coolant serves to lubricate the grinding interface, reducing friction between the wheel and the workpiece. This lubrication not only enhances the efficiency of the grinding operation but also contributes to achieving a superior surface finish.
Coolant helps to flush away debris and metal particles generated during grinding, preventing them from interfering with the process. Incorporating coolant into precision grinding operations is essential for maintaining quality and extending tool life when working with hardened dies and punches.
Techniques for Achieving Uniform Surface Finish in Precision Grinding
Achieving a uniform surface finish in precision grinding requires a combination of techniques and best practices tailored to the specific requirements of hardened dies and punches. One effective approach is to employ a systematic grinding strategy that includes multiple passes with varying wheel grits. Starting with a coarser grit allows for efficient material removal, while subsequent passes with finer grits refine the surface finish.
This method not only enhances uniformity but also minimizes the risk of introducing defects such as chatter marks or uneven surfaces. Another critical technique involves controlling the grinding parameters, including speed, feed rate, and depth of cut. By carefully adjusting these variables, operators can optimize the grinding process to achieve a consistent finish across the entire surface area of the workpiece.
Maintaining a stable setup with minimal vibration is essential for preventing inconsistencies in surface quality. Implementing these techniques ensures that hardened dies and punches meet stringent quality standards while maximizing productivity.
Maintaining Consistent Grinding Pressure for Hardened Dies & Punches
Consistent grinding pressure is crucial for achieving optimal results in precision grinding operations involving hardened dies and punches. Variations in pressure can lead to uneven wear on the grinding wheel and inconsistent material removal rates, in the end affecting the quality of the finished product. To maintain consistent pressure, operators must monitor several factors, including wheel wear, workpiece characteristics, and machine settings.
Dressing the Grinding Wheel for Optimal Performance in Precision Grinding
Dressing the grinding wheel is an essential practice that significantly impacts its performance during precision grinding operations for hardened dies and punches. Over time, grinding wheels can become glazed or loaded with material, which diminishes their cutting efficiency and affects surface finish quality. Dressing involves removing this buildup and reshaping the wheel’s surface to restore its cutting capabilities.
This process not only enhances performance but also prolongs the life of the wheel. There are various methods for dressing grinding wheels, including mechanical dressing tools and diamond dressers. Each method has its advantages depending on factors such as wheel type and desired finish.
Balancing Speed and Feed Rates for Efficient Precision Grinding
Balancing speed and feed rates is crucial for achieving efficiency in precision grinding processes involving hardened dies and punches. The speed at which the grinding wheel rotates (spindle speed) must be carefully matched with the rate at which the workpiece is fed into it (feed rate). An optimal balance between these two parameters ensures effective material removal while minimizing heat generation and wear on both the tool and workpiece.
If spindle speed is too high relative to feed rate, it can lead to excessive heat buildup, resulting in thermal damage to both components. Conversely, if feed rate is too high compared to spindle speed, it may cause inefficient cutting action or even stall the machine. Therefore, operators must conduct thorough testing to determine ideal settings based on specific materials and desired outcomes.
Using Jigs and Fixtures for Precise Positioning in Precision Grinding
The use of jigs and fixtures is instrumental in ensuring precise positioning during precision grinding operations for hardened dies and punches. These tools provide stability and repeatability by securely holding workpieces in place throughout the grinding process. Proper positioning is essential for achieving accurate dimensions and surface finishes; any movement or misalignment can lead to defects or inconsistencies.
Jigs are typically designed for specific tasks or shapes, allowing operators to quickly set up their machines without extensive adjustments each time a new part is processed. Fixtures serve a similar purpose but may be more versatile in accommodating various workpieces. By utilizing jigs and fixtures effectively, manufacturers can streamline their operations while enhancing accuracy in producing hardened dies and punches.
Post-Grinding Inspection and Quality Control for Hardened Dies & Punches
Post-grinding inspection is a critical step in ensuring that hardened dies and punches meet quality standards after precision grinding operations are completed. This phase involves thorough examination using various measurement tools such as calipers, micrometers, or coordinate measuring machines (CMM). Inspecting dimensions against specified tolerances helps identify any deviations early on, allowing for corrective actions before parts are sent out for use.
Quality control processes should also include assessments of surface finish quality through visual inspections or specialized equipment like profilometers. By implementing rigorous post-grinding inspection protocols, manufacturers can maintain high levels of quality assurance while minimizing waste associated with rework or scrap parts. In the end, effective quality control measures contribute significantly to customer satisfaction by ensuring that only top-quality hardened dies and punches reach end-users.
FAQs
What is a 2×72 grinder?
A 2×72 grinder is a type of belt grinder that uses a 2-inch by 72-inch belt for grinding, sharpening, and shaping metal and other materials. It is commonly used in metalworking and knife making.
What are hardened dies and punches?
Hardened dies and punches are metal tools used in manufacturing processes to cut, shape, or form materials such as metal, plastic, or wood. They are made from hardened steel to withstand the high pressure and wear associated with their use.
Why is grinding hardened dies and punches challenging?
Grinding hardened dies and punches is challenging because the hardened steel material is very tough and resistant to abrasion. It requires specialized grinding techniques and equipment to effectively shape and sharpen these tools without damaging them.
How is a 2×72 grinder used for grinding hardened dies and punches?
A 2×72 grinder is used for grinding hardened dies and punches by using the abrasive belt to remove material and shape the tools to the desired dimensions. The grinder allows for precise control and shaping of the hardened steel, making it suitable for this challenging task.
What are the benefits of using a 2×72 grinder for grinding hardened dies and punches?
Using a 2×72 grinder for grinding hardened dies and punches offers benefits such as precision, control, and efficiency in shaping and sharpening the tools. The grinder allows for the removal of material while maintaining the integrity and hardness of the dies and punches.
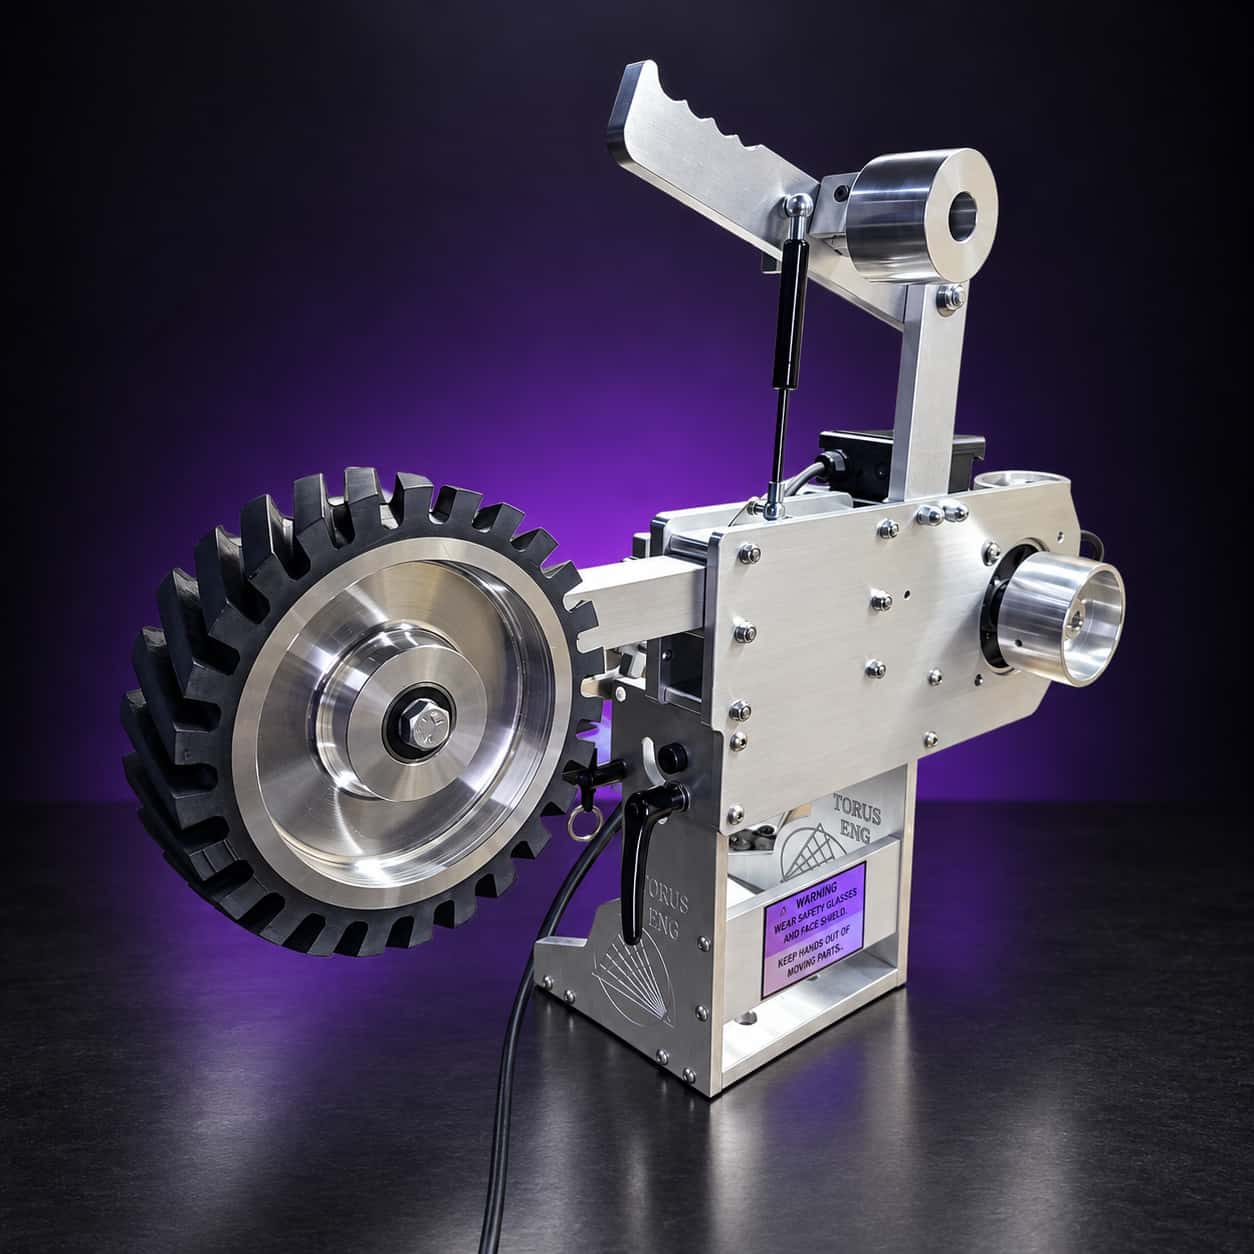
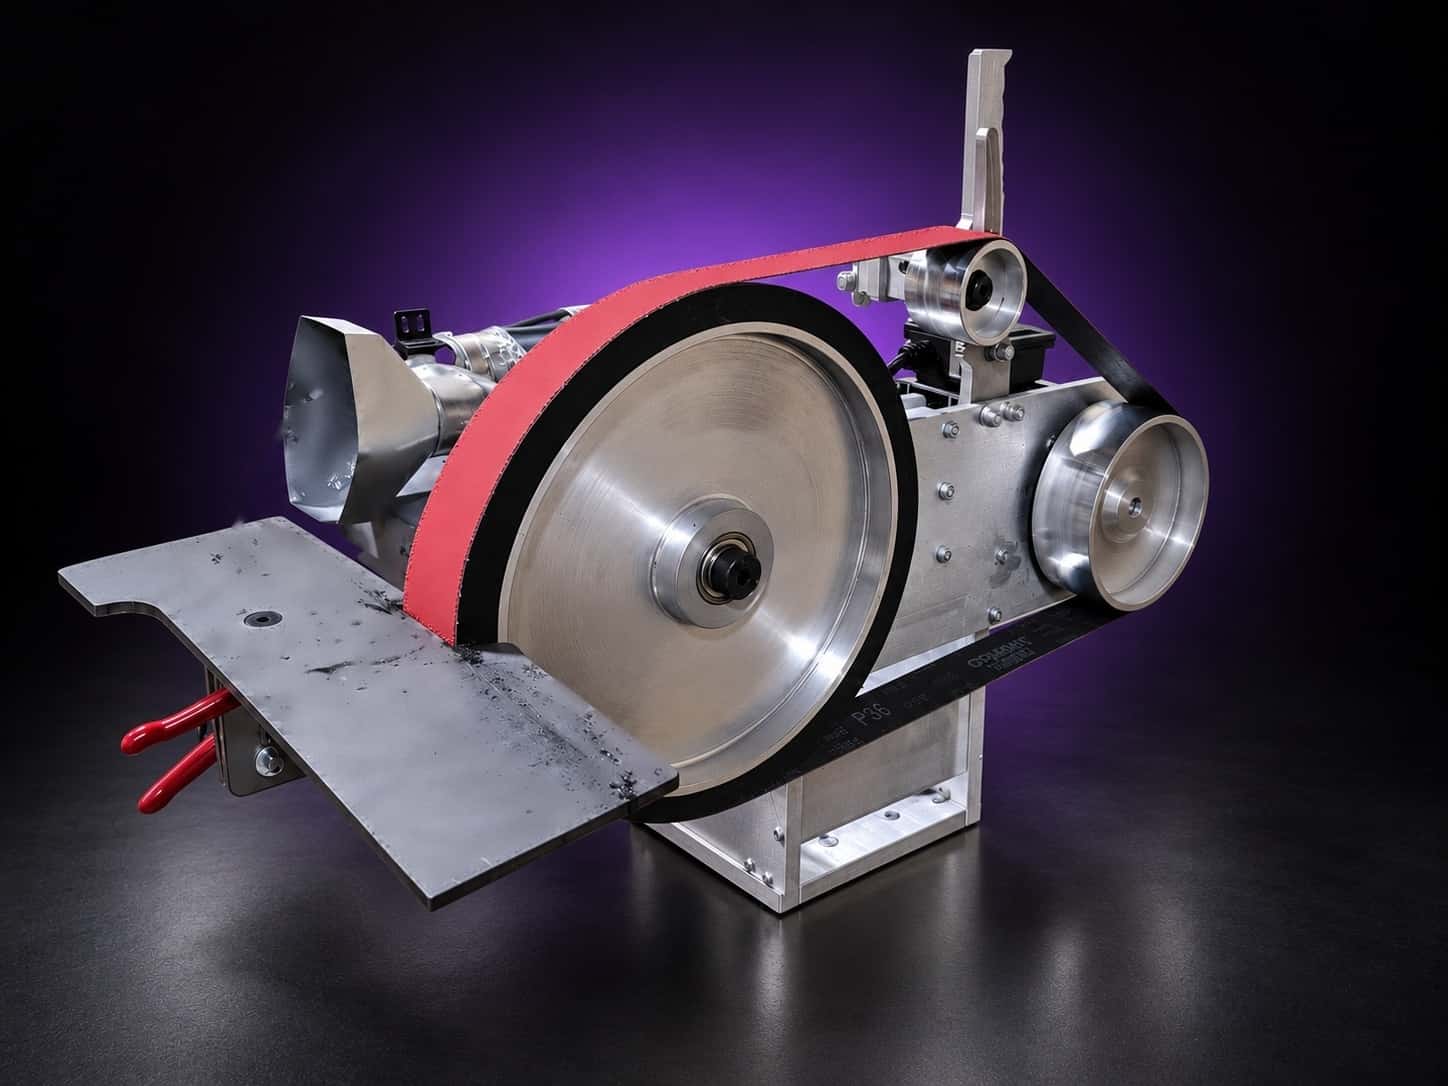
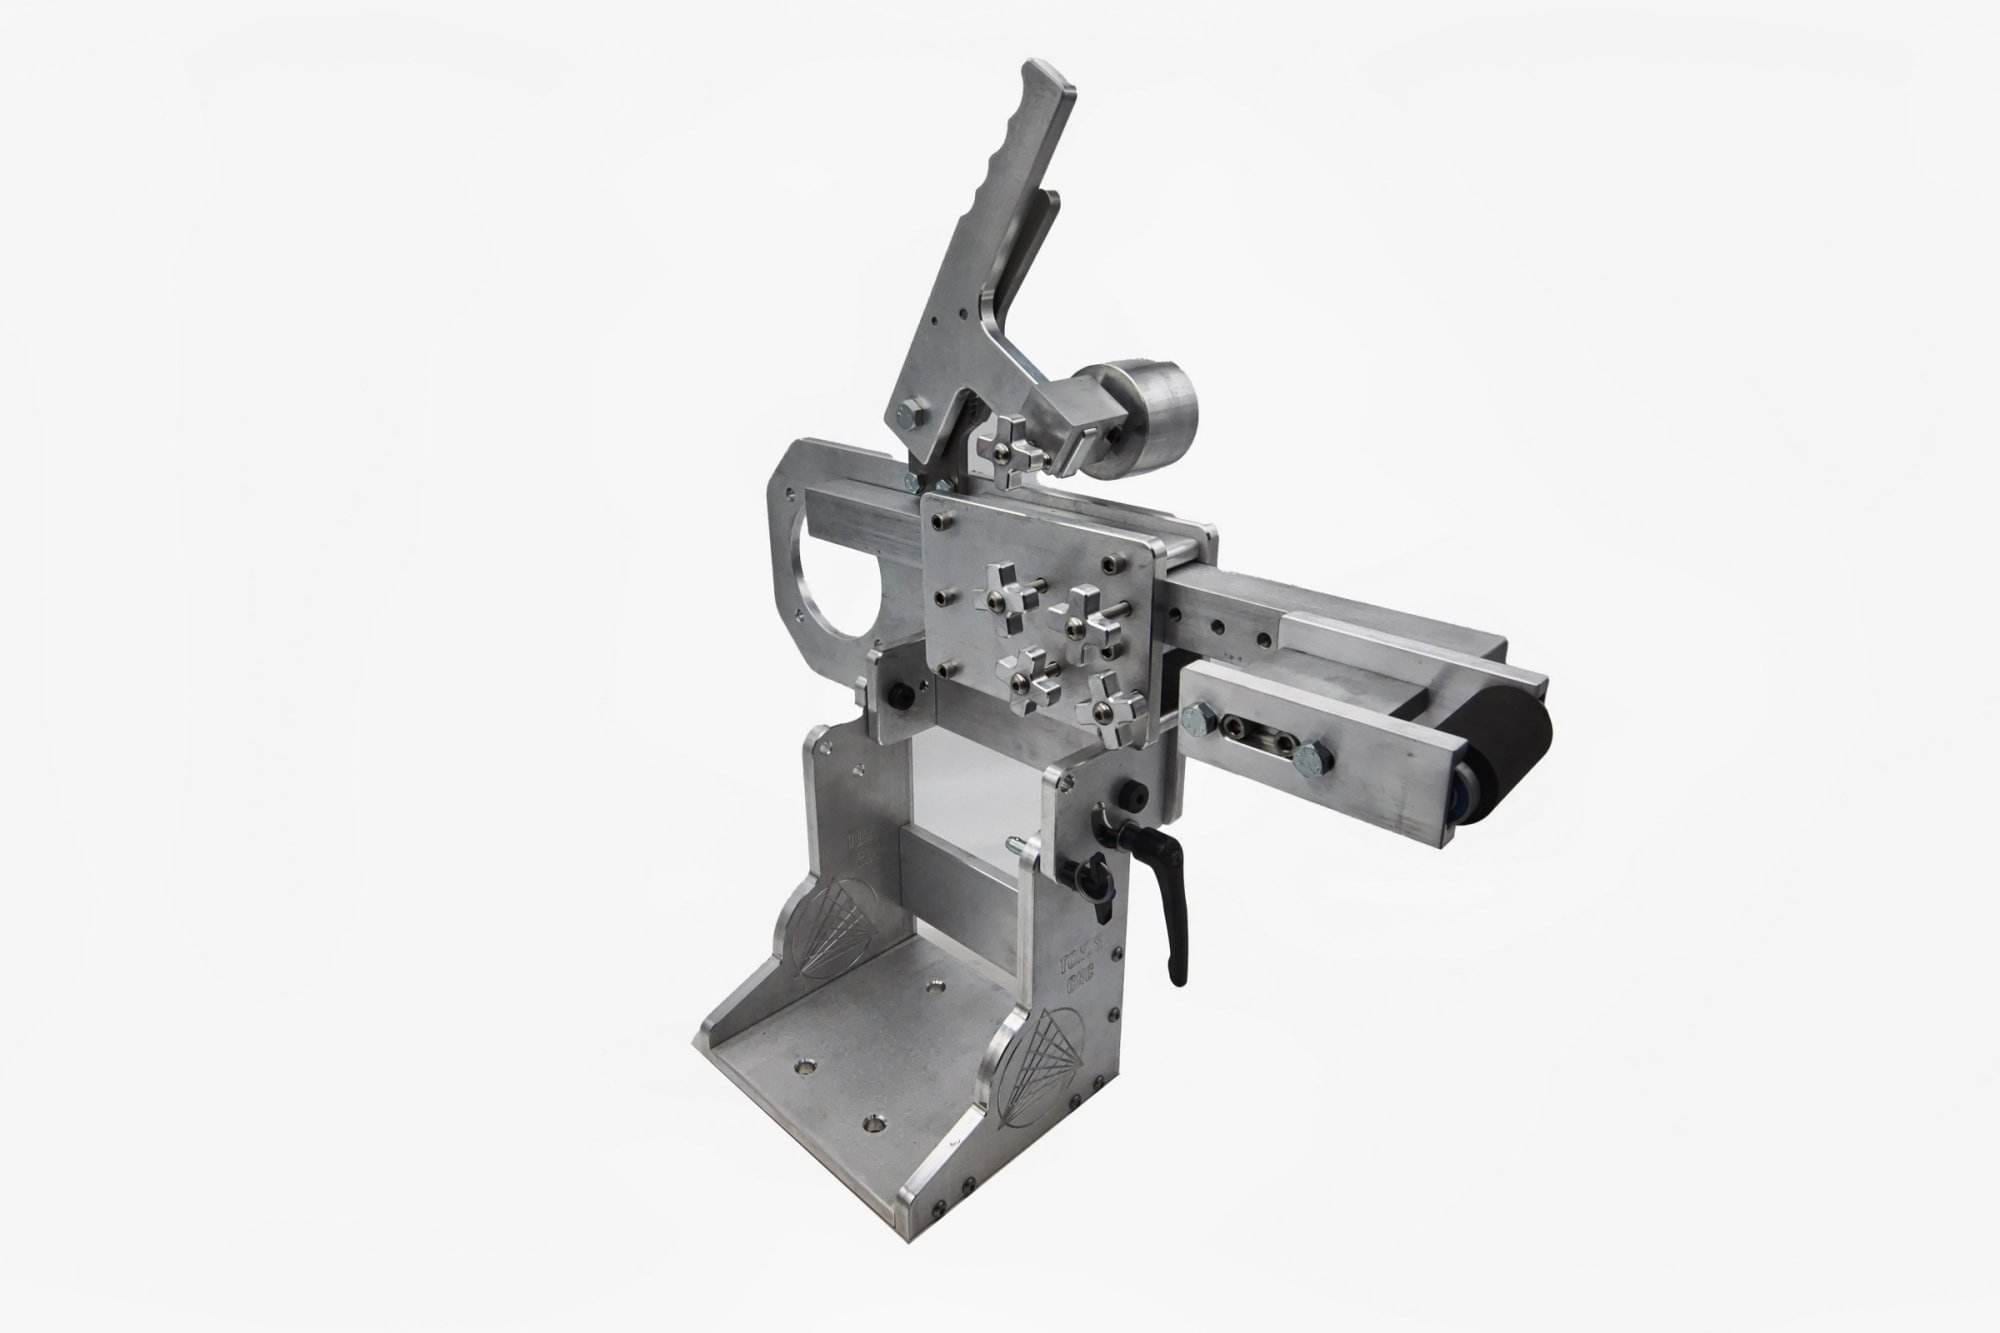
Tight tolerances want a chassis that does not flex and a table that does not move. The Nebula 2×72 is 3/8-inch steel, the 6×16 work table is 5/16-inch steel on a 3/8-inch bracket, and the VFD slows the belt for hardened stock. Built and tested in Sterling, Illinois.