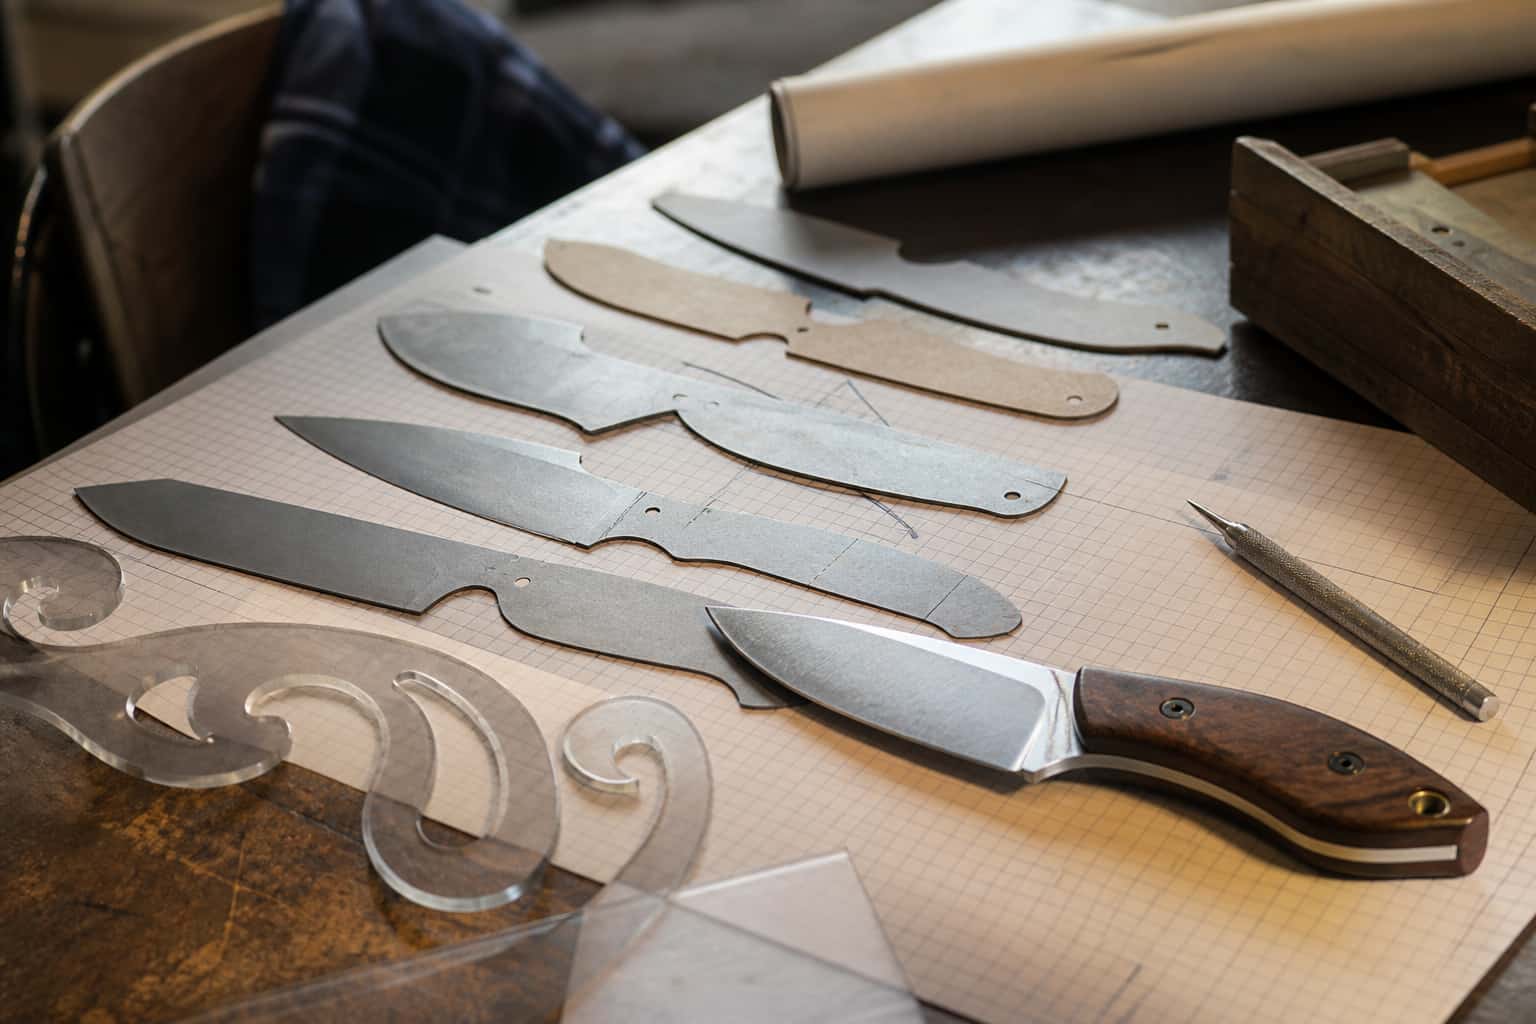
Abrasives and belt grinding in a working knife shop

Abrasives

Hand Sanding a Blade: The Method That Actually Removes Scratches

How to hand sand a blade properly: grit progression, hard backers, WD-40 lubricant, the 45-degree direction change, and the go-back-down rule.

3 min readWritten by Rich LinvilleFree to read

Hand sanding is the tax every clean blade finish collects, and most makers pay it wrong: hours of scrubbing that polish scratches instead of removing them. The actual skill fits in a few rules — hard backer, one direction per grit, never skip ahead with scratches still showing — and once they’re habits, a hand-rubbed 400-grit satin stops being a chore and becomes the signature of your work. This is the companion skill to everything in Blade Finishes Explained, and it’s the entire finishing method if you’re working without a grinder.
The Setup

  • Quality wet/dry paper. This is not the place for hardware-store bargain sheets — the community standard is a premium wet/dry paper (Rhynowet Red Line is the perennial forum favorite) that cuts fast and doesn’t shed grit into your finish. Good paper is the single biggest time-saver in hand sanding.
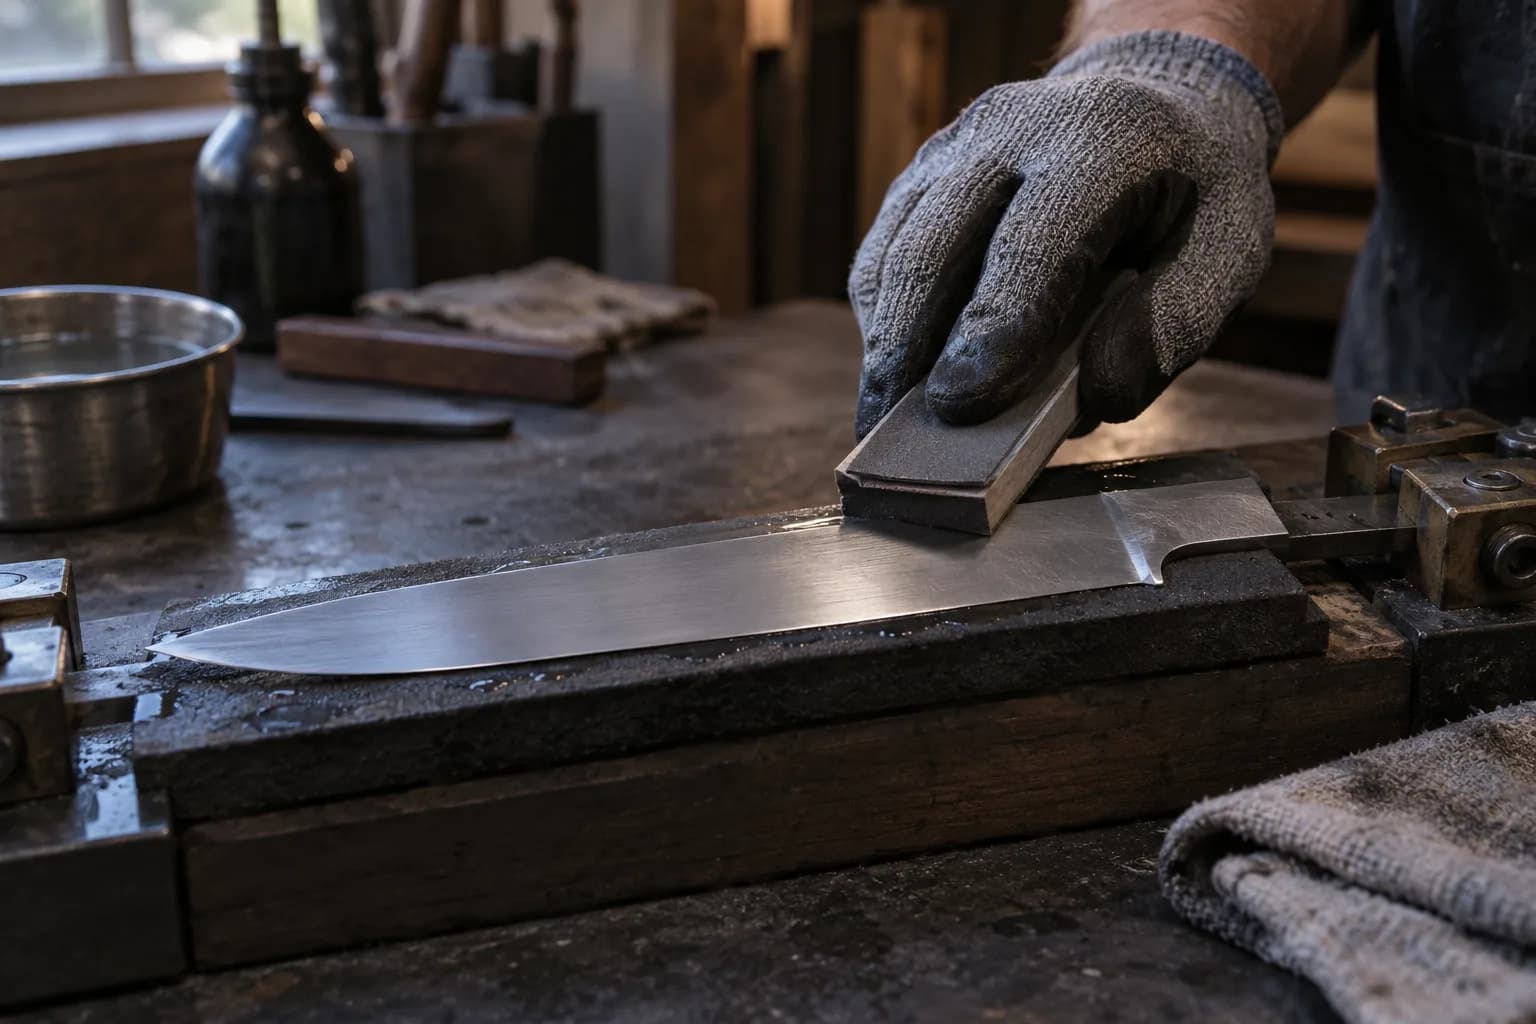
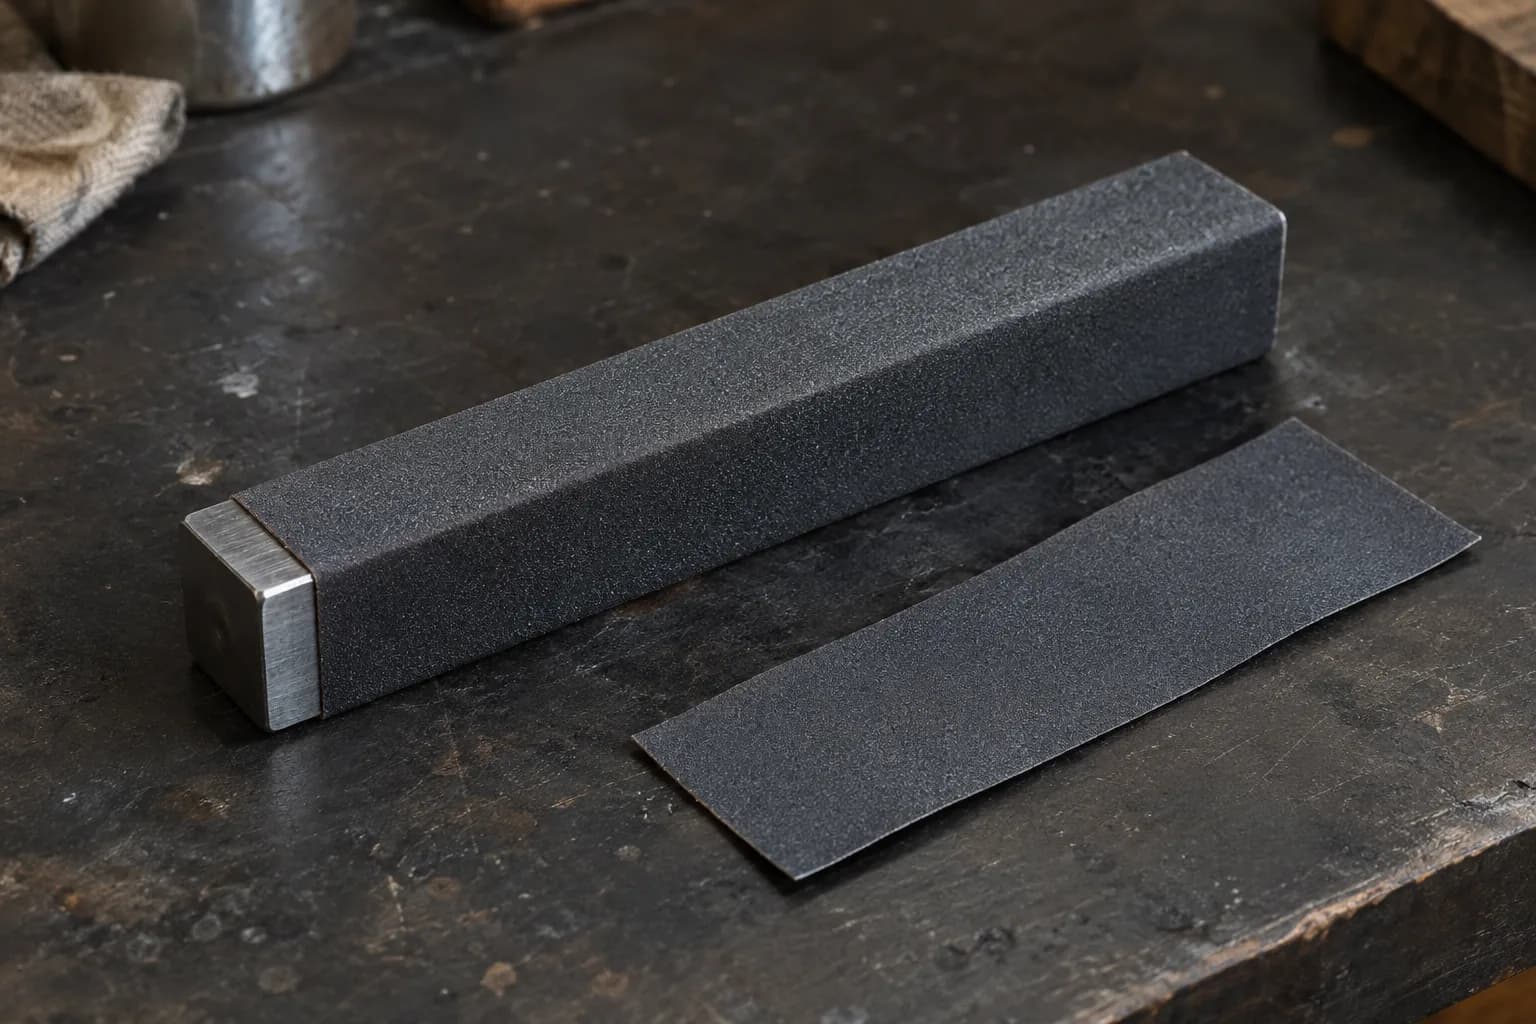
  • A hard, flat backer. Paper wrapped around a steel bar, micarta block, or hardwood stick. Fingers-only sanding rounds crisp grind lines into mush; the backer keeps flats flat and plunge lines sharp. Many makers switch to a leather-faced stick after 400 grit for the final passes — firm base, tiny bit of give.
    Dark wet-dry paper wrapped tightly around a square steel bar on a charcoal bench, with a spare paper strip beside it.
  • A lubricant. WD-40, Windex, or soapy water — it floats the swarf out of the paper, cuts faster, and shows scratches honestly. Dry sanding loads the paper and lies to you.
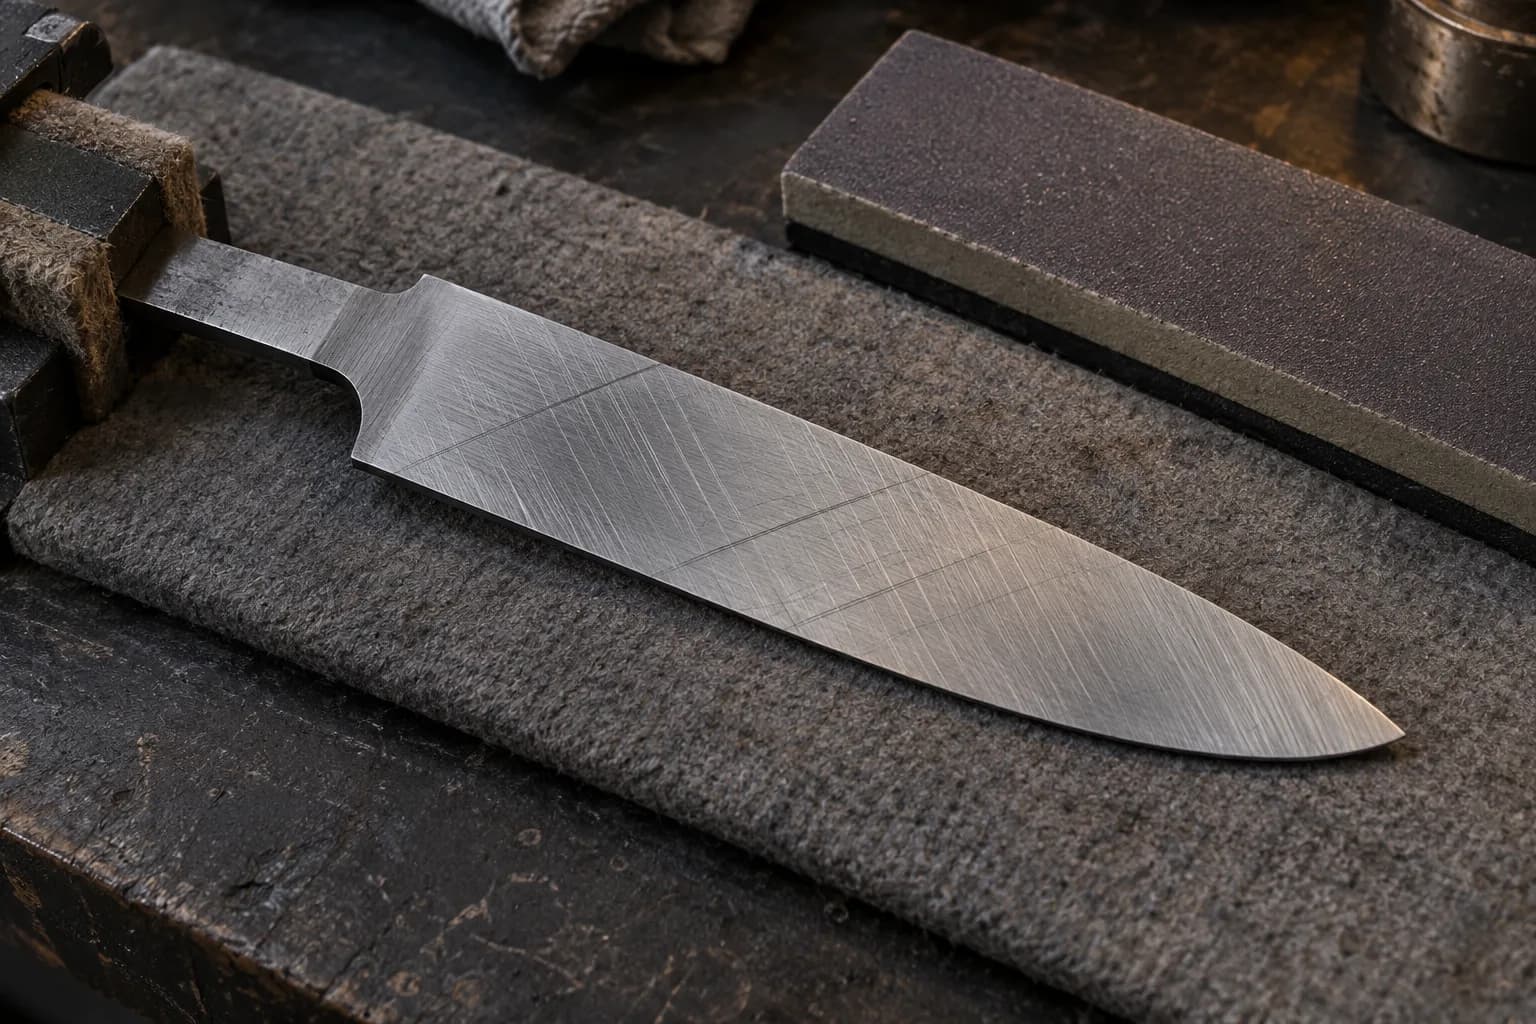
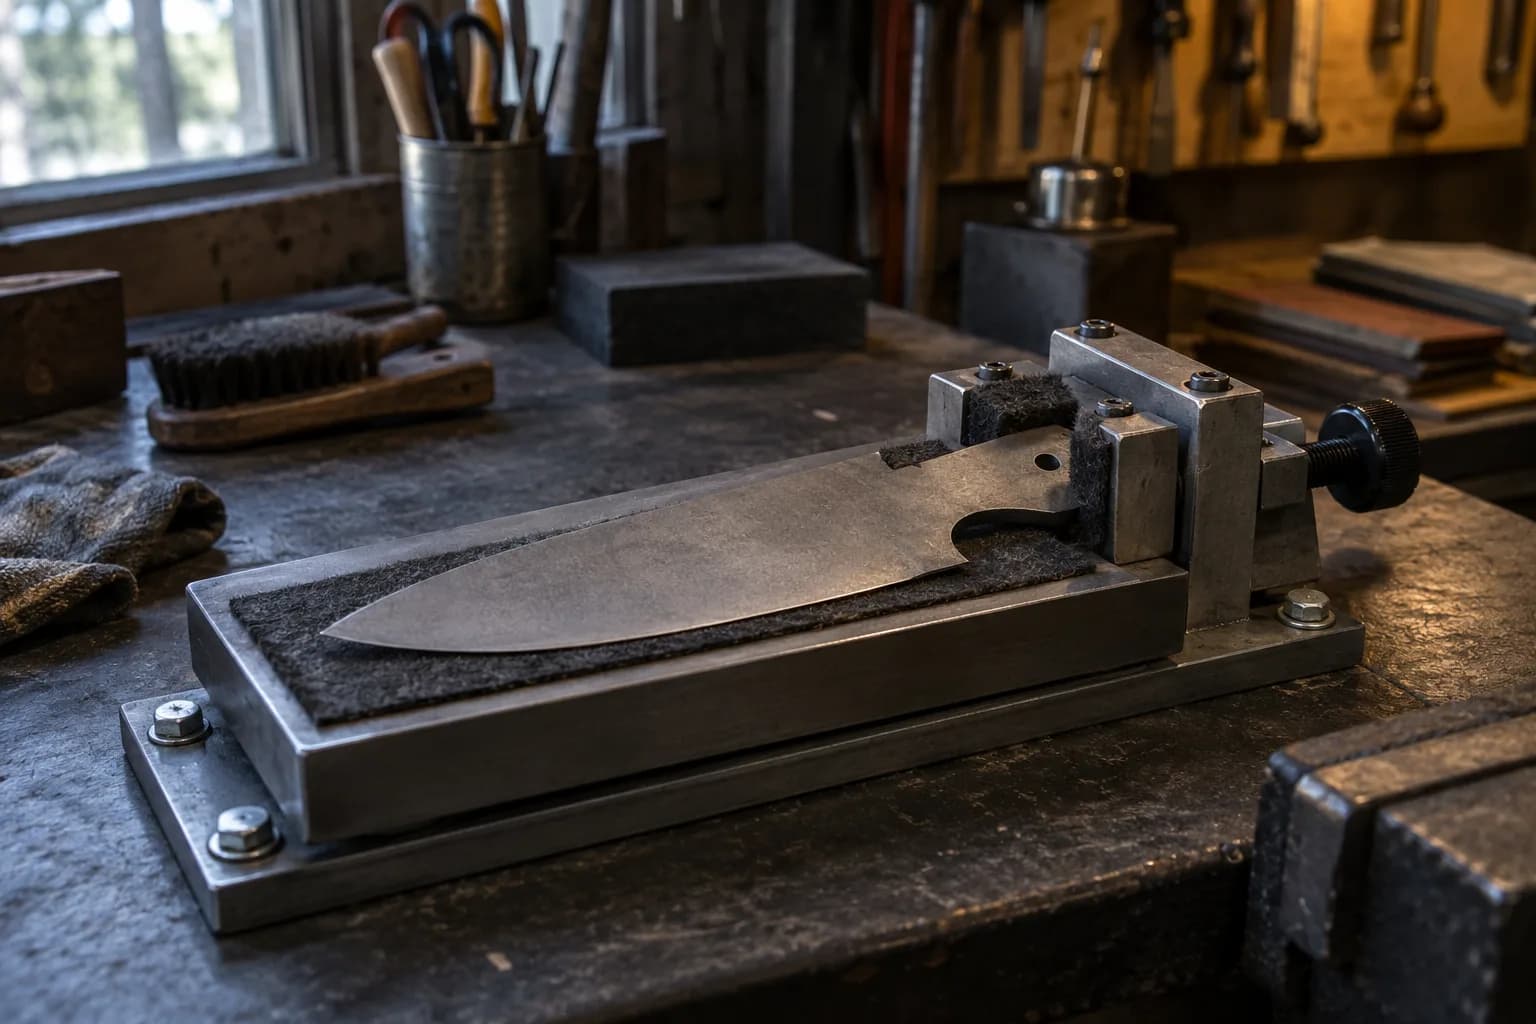
  • A way to hold the blade still. Clamp it flat to the bench (padded), or use a bladed jig — sanding a blade you’re also holding is how fingers meet edges.
    Flat blade blank resting on a felt-padded steel plate, its tang held in padded screw jaws bolted to the bench.

The Method

  1. Start where the scratches are, not where you wish they were. Off a 220-grit belt, start hand sanding around 220–320. Starting at 600 to “save time” costs triple.
  2. One direction per grit — then change it. Sand each grit at roughly 45° to the previous grit’s lines. When every old-direction scratch is gone, that grit is done — the direction change is your progress meter, and it’s the whole secret. Typical run: 220 → 320 → 400 (→ 600 → 800+ only if the finish calls for it).
    Bare knife blade lying on a felt pad with its tang in padded vise jaws, fine diagonal sanding lines crossed by deeper scratches
  3. Fresh paper, often. Worn paper burnishes instead of cutting. If progress stalls, the paper’s done, not you.
  4. Stubborn scratch? Go back down, not up. A scratch that won’t leave at 400 will never leave at 600 — it only gets shinier. Drop back a grit, kill it, move on. This single rule saves more hours than every other tip combined.
  5. Finish with intent. For the classic hand-rubbed satin: final grit in one uniform direction, usually spine-to-edge or tip-to-ricasso, long even strokes. A trick from the forums for a softer satin — go one grit past your target, then come back down one and finish there.
    Gloved hand drawing a paper-wrapped sanding stick along a wet blade held flat on a padded bench fixture.

The Traps

  • Skipping grits. 220 to 600 isn’t a shortcut; it’s the scenic route through frustration.
  • Polishing before de-scratching. Shiny with deep scratches is worse than honest satin — the polish spotlights them.
  • Soft backing everywhere. Save the leather-backed touch for final passes; foundations want hard.
  • Sanding a blade after sharpening. Finish work first, apex last — in both senses.

Budget expectations honestly: a full hand-rubbed finish on a hardened blade runs from one to several hours depending on how clean your belt progression left the surface — the machine grits you finish at determine the hand grits you start at, which is the best argument for finishing well on the grinder.

Sources

Keep reading

Read these related guides

Three more from the same bench.

Same bench

Put the reference to work

I machine the parts, hand-assemble, track and test Torus grinders in Sterling, Illinois. Most orders ship in seven to ten business days from time of order.

  • Classic aluminum 2x72 grinder, side view with flat-platen tool arm and yellow Safety Rules label, on black with a purple glow

    Torus 2×72 Classic Aluminum Belt Grinder

    Prior-design aluminum chassis, 90-degree tilt and 1.5-inch tooling arms.

    Starts at$995View

One-man shop

Still stuck? Ask me.

I answer my own email. Tell me the steel, the machine and what it is doing, and I will tell you what I would try next.