Heat Treat
Heat Treating Knife Steel: Complete Guide
Heat treating is what turns a piece of flat bar stock into a functional knife blade. Done correctly, it transforms the steel’s internal crystal structure…
Metallurgy
Why the right HRC is not the highest one: the hardness-versus-toughness trade-off, typical ranges by knife use, and why one number behaves differently by steel.
4 min readWritten by Rich LinvilleFree to read
Heat treat recipes and steel spec sheets both cite a target hardness on the Rockwell C scale, but the number by itself doesn’t explain why that specific target was chosen instead of just going as hard as the steel allows. Understanding the tradeoff behind that number is what separates picking a hardness on purpose from just following a recipe blindly.
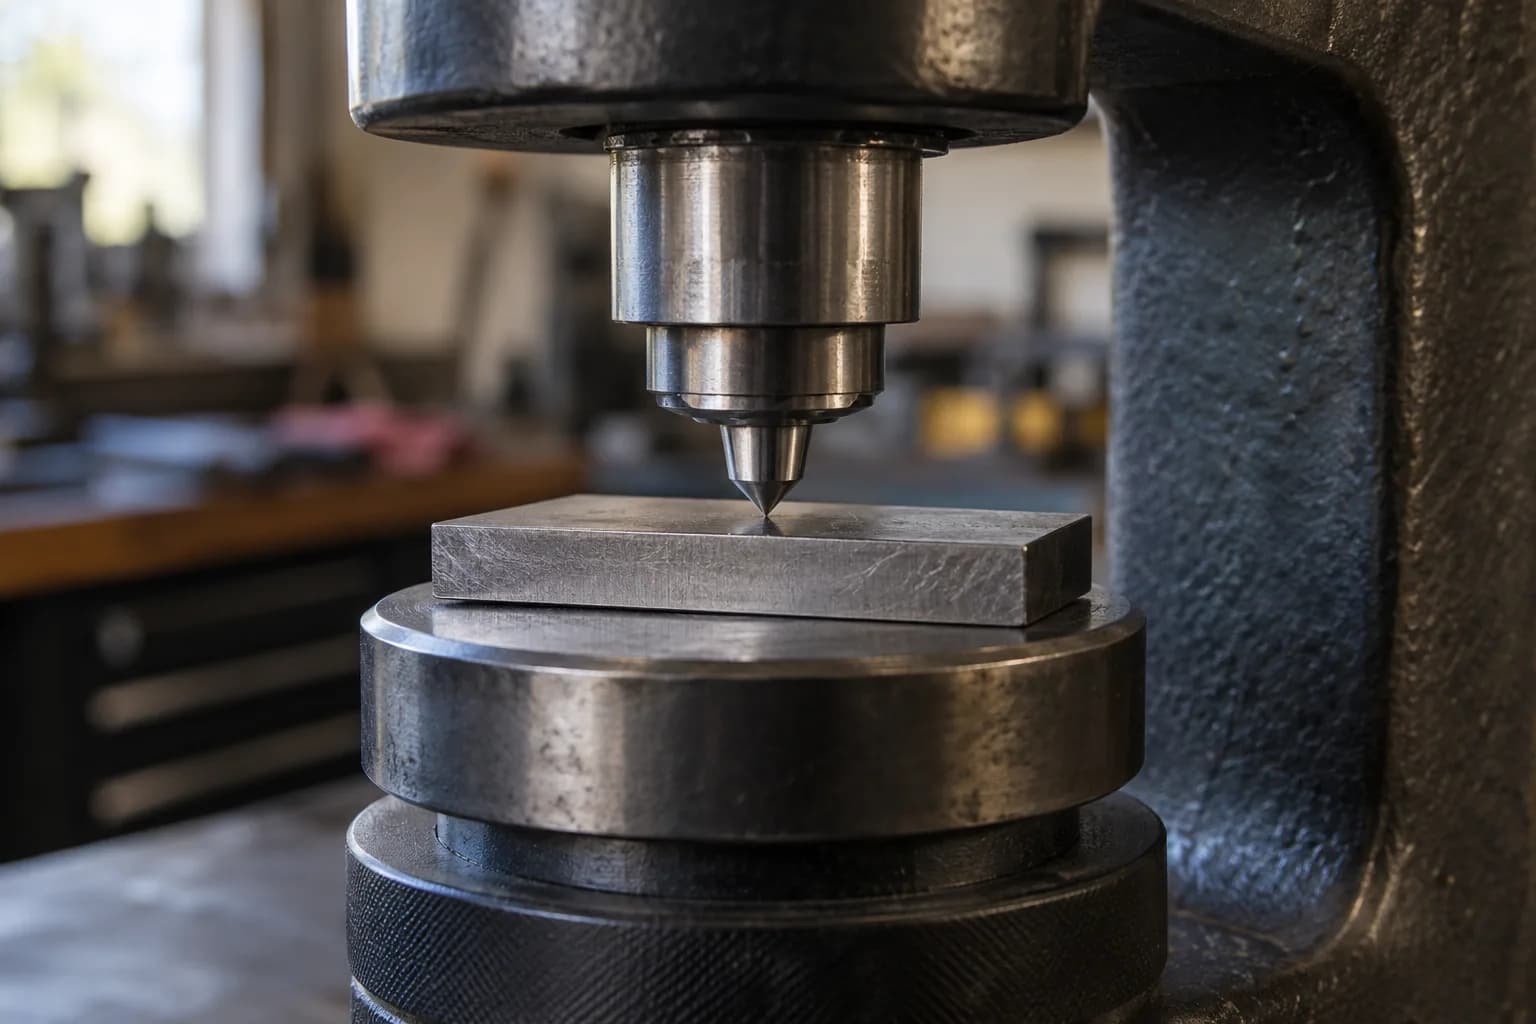
Rockwell C (HRC) measures resistance to a diamond indenter being pressed into the steel under a set load, higher numbers mean the steel resists that indentation more, which correlates closely with how well an edge resists rolling, denting, and wearing down in use. Most knife steels finish somewhere between 55 and 65 HRC depending on the alloy and intended use, a fairly narrow window compared to the full scale, but one where small differences matter a lot.
As hardness goes up, a steel generally holds a sharper edge longer and resists wear better, but it also becomes more brittle and more prone to chipping or cracking under lateral stress or impact. As hardness goes down, the steel becomes tougher and more forgiving of hard use, but the edge rolls, dents, and dulls faster. Every heat-treat target is a deliberate point on this tradeoff, not an attempt to maximize hardness for its own sake.
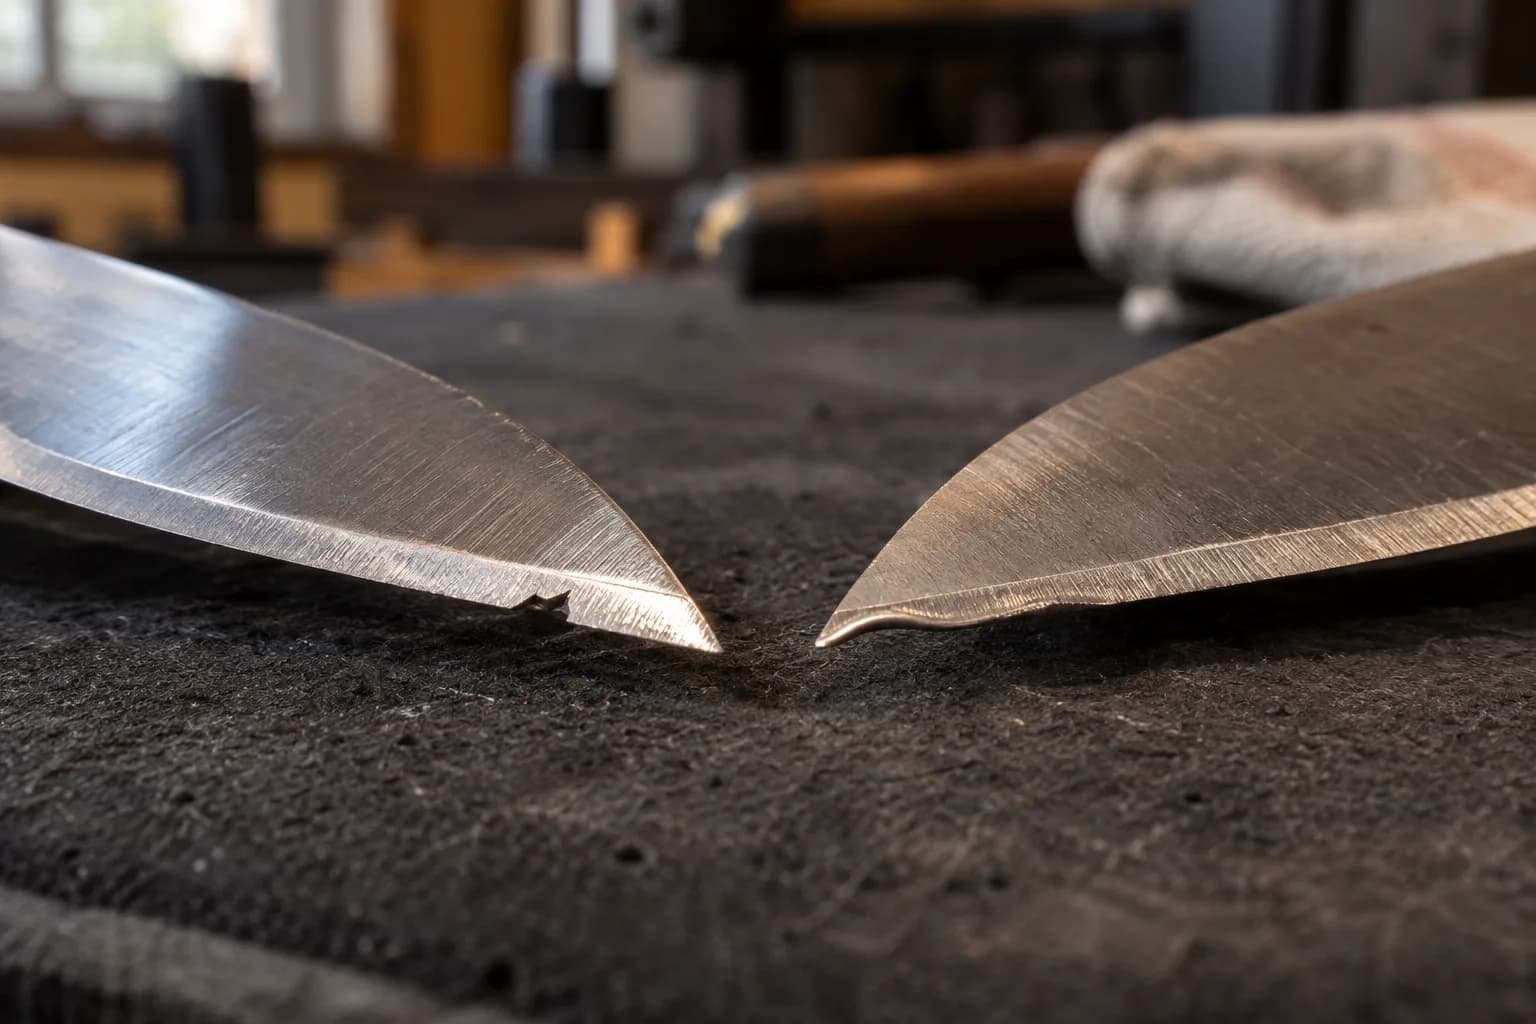
Pushing a steel to its maximum achievable hardness usually means giving up enough toughness that the edge becomes genuinely fragile, prone to chipping on contact with hard materials, bone, staples, or even just an awkward cutting angle, and in extreme cases prone to cracking under normal use. Overly hard steel can also become harder to sharpen predictably, since a very hard, brittle edge can fracture at the apex during sharpening instead of forming a clean edge. Maximum hardness is rarely the goal; the right hardness for the job is.
Going too soft trades away real cutting performance. A soft edge rolls over rather than staying sharp, dents easily, and dulls quickly even in normal use, requiring far more frequent sharpening. Below a certain point, a blade stops behaving like a knife steel and starts behaving like mild steel, holding essentially no edge at all. Softness isn’t automatically safer, it just fails in a different way (constant dulling) instead of the way overhardening fails (chipping).
Kitchen and fine-slicing knives commonly target 58-62 HRC, prioritizing a keen, long-lasting edge since they rarely see lateral stress or impact. General-purpose EDC and hunting knives often land in a similar 58-61 HRC range, balancing edge retention with enough toughness for normal use. Hard-use, chopping, or survival knives are frequently tempered a bit softer, often 56-58 HRC, deliberately trading some edge retention for meaningfully better impact and chip resistance. These ranges aren’t rigid rules, they’re starting points that shift based on the specific steel and how it’s actually going to be used.
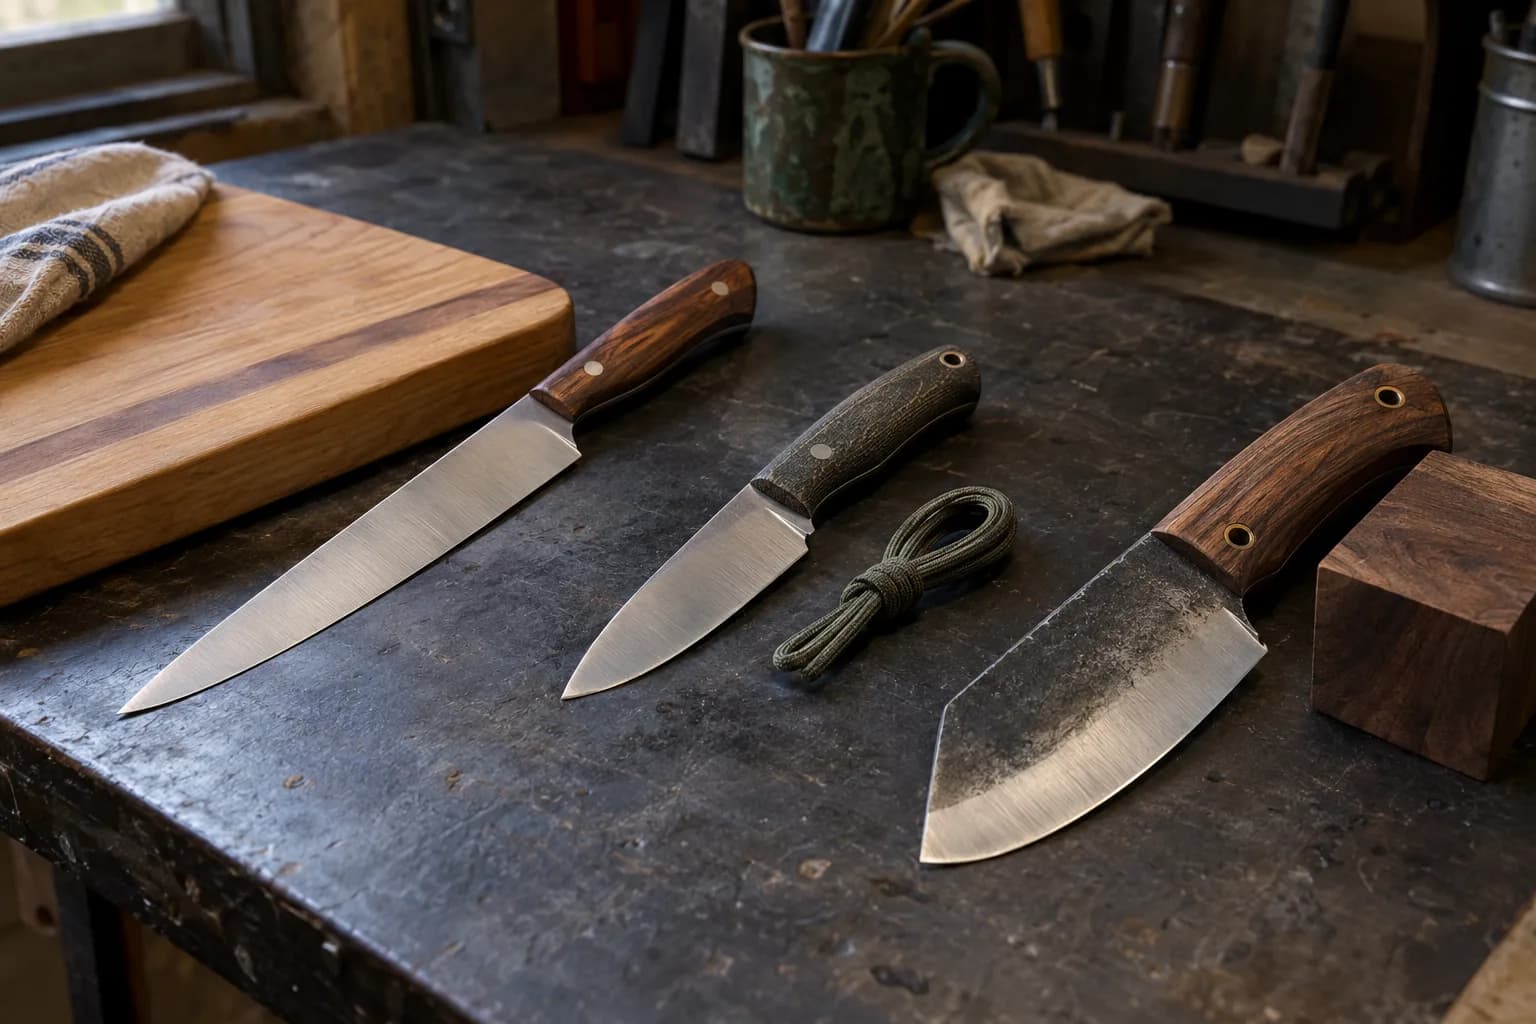
60 HRC in a simple carbon steel and 60 HRC in a high-vanadium powder-metallurgy steel don’t behave identically, the alloy content and carbide structure change how that hardness translates into real-world toughness and edge stability. This is why steel selection and hardness target are decided together, not independently, see Choosing Steel by Application for how the two interact.
Steels aren’t equally good at every hardness within their range. Most have a sweet spot where toughness and edge retention balance well, push past it and toughness drops off faster than edge retention improves; stay well below it and the steel underperforms what it’s actually capable of. Manufacturer and metallurgist-published data (like Crucible’s data sheets for CPM steels) typically show this relationship directly, and it’s part of why heat-treat recipes specify a fairly narrow target range rather than “as hard as possible.”
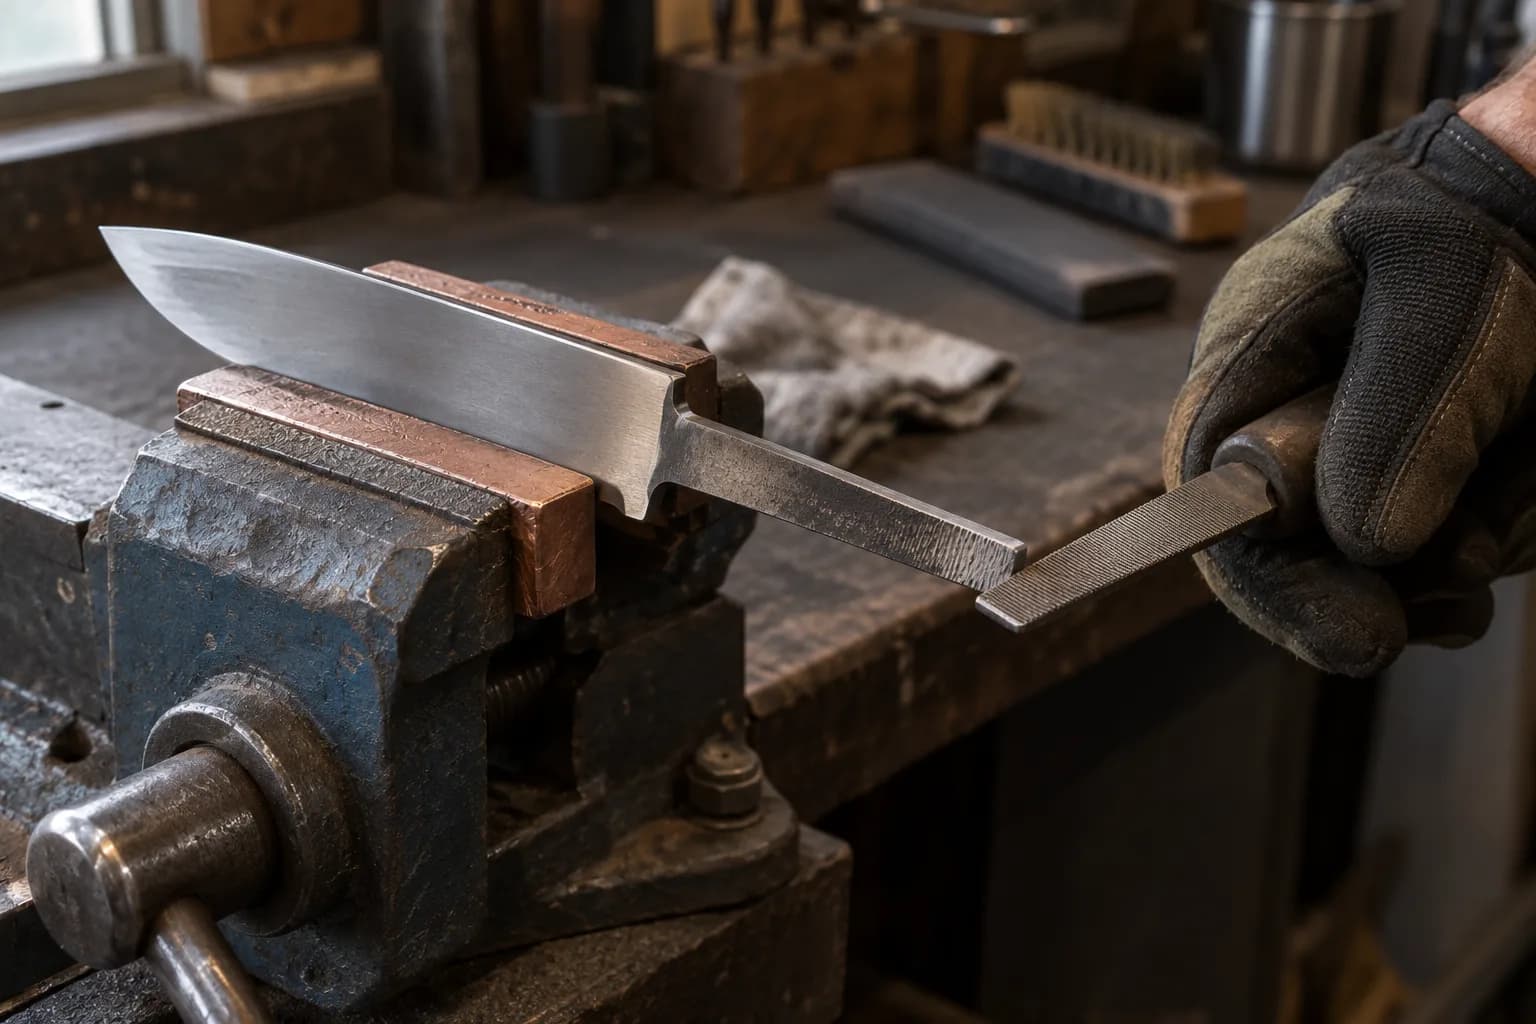
None of this matters if the actual hardness achieved isn’t verified. A file test at minimum, or Rockwell testing if available, confirms the heat treat actually landed in the intended range rather than assuming it did. See 10 Common Mistakes Beginner Knifemakers Make for how often this step gets skipped.
No. Harder generally means better edge retention but more brittleness; the right hardness depends on how the knife will actually be used, not on maximizing one property at the expense of everything else.
Follow the published heat-treat recipe for whatever steel you’re using, most simple carbon steels land naturally in the 58-60 HRC range with a standard recipe, which is a solid, balanced target for a first build rather than something you need to push higher or lower.
Yes. Pushing past a steel’s practical range doesn’t just add diminishing returns, it can actively make the blade worse, more prone to chipping and cracking without a meaningful edge-retention benefit to show for it.
Keep reading
Three more from the same bench.
Heat treating is what turns a piece of flat bar stock into a functional knife blade. Done correctly, it transforms the steel’s internal crystal structure…
The Heat Treating Guide covers the practical steps: normalize, austenitize, quench, temper. This guide covers what’s actually happening inside the steel…
Every steel in the Knife Steel Database is rated 1-5 across four properties: toughness, edge retention, corrosion resistance, and machinability. Here’s…
Same bench
I machine the parts, hand-assemble, track and test Torus grinders in Sterling, Illinois. Most orders ship in seven to ten business days from time of order.
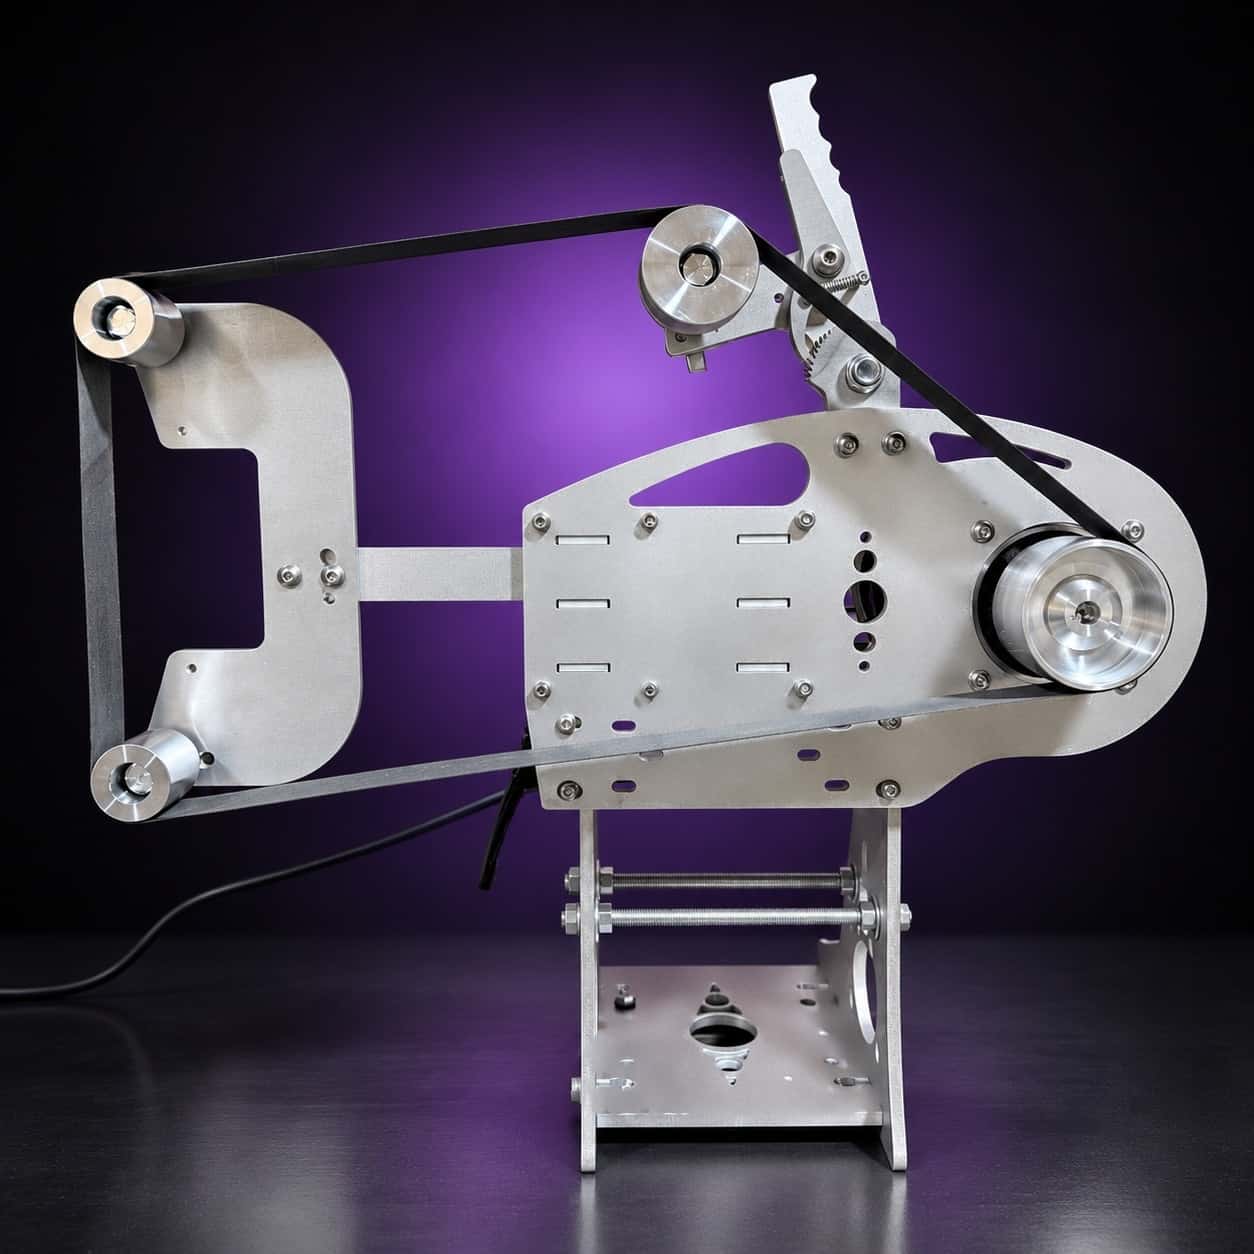
Current dual-axis platform with a fiber-laser-cut 6061 chassis and single-knob tracking.
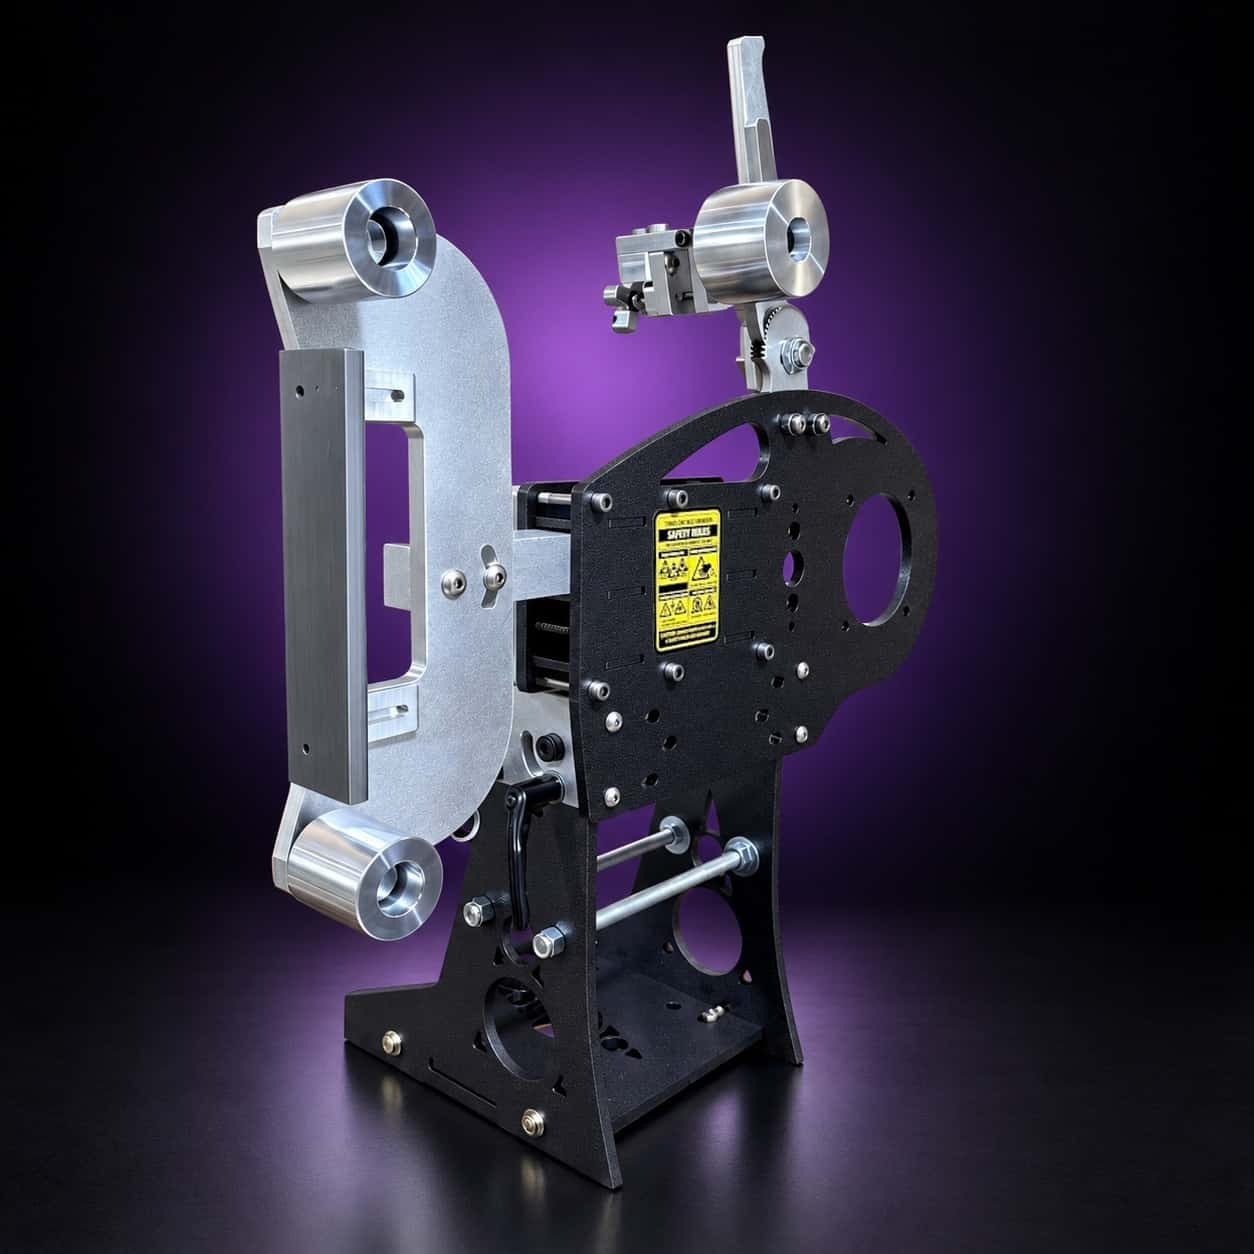
Current dual-axis platform with a steel chassis, more mass and less vibration.
These are the last Nebula chassis available until the next release. Once this run sells out, availability pauses until the next run is ready.
Next release: 10 more chassis expected Nov 17–Nov 24 (3–4 weeks from Oct 27).
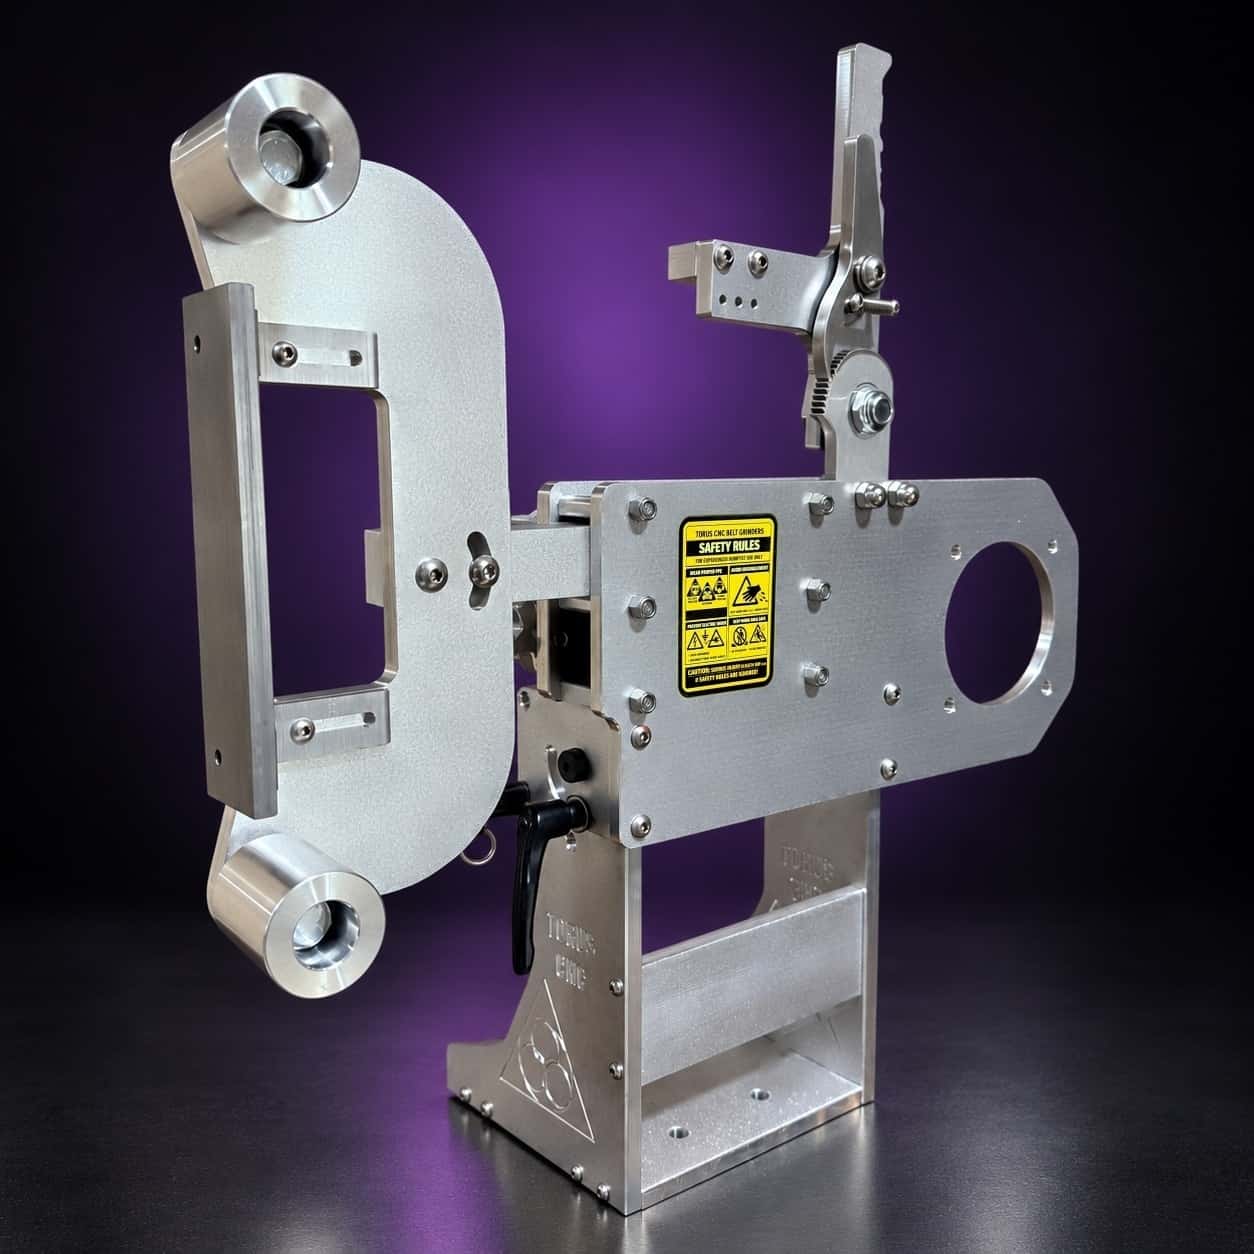
Prior-design aluminum chassis, 90-degree tilt and 1.5-inch tooling arms.
One-man shop
I answer my own email. Tell me the steel, the machine and what it is doing, and I will tell you what I would try next.