
Heat Treat
Heat Treating Knife Steel: Complete Guide
Heat treating is what turns a piece of flat bar stock into a functional knife blade. Done correctly, it transforms the steel’s internal crystal structure…
Abrasives
Belt recommendations, grit progression, and diamond sharpening tips for grinding CPM 20CV on a 2x72 belt grinder. Free guide from Torus CNC's ForgeBrain.
1 min readWritten by Rich LinvilleFree to read
CPM 20CV sits alongside CPM S30V and CPM M4 among the more demanding steels in this database to grind and sharpen. The same heavy chromium-vanadium carbide load that gives it exceptional edge retention also means belts load and dull faster than on tougher, easier-working steels like MagnaCut or Elmax, and standard sharpening stones struggle to cut its carbides once it is hardened.
Ceramic belts are essentially mandatory for CPM 20CV, the same recommendation that applies to other high-carbide CPM steels like S30V. Zirconia or aluminum oxide belts will work, but wear out noticeably faster and cut more slowly on this steel’s dense carbide structure. Budget for more belts per knife than you would with a tougher, easier-grinding steel.
A practical progression after heat treat looks similar to other premium stainless steels, just expect to change belts more often along the way:
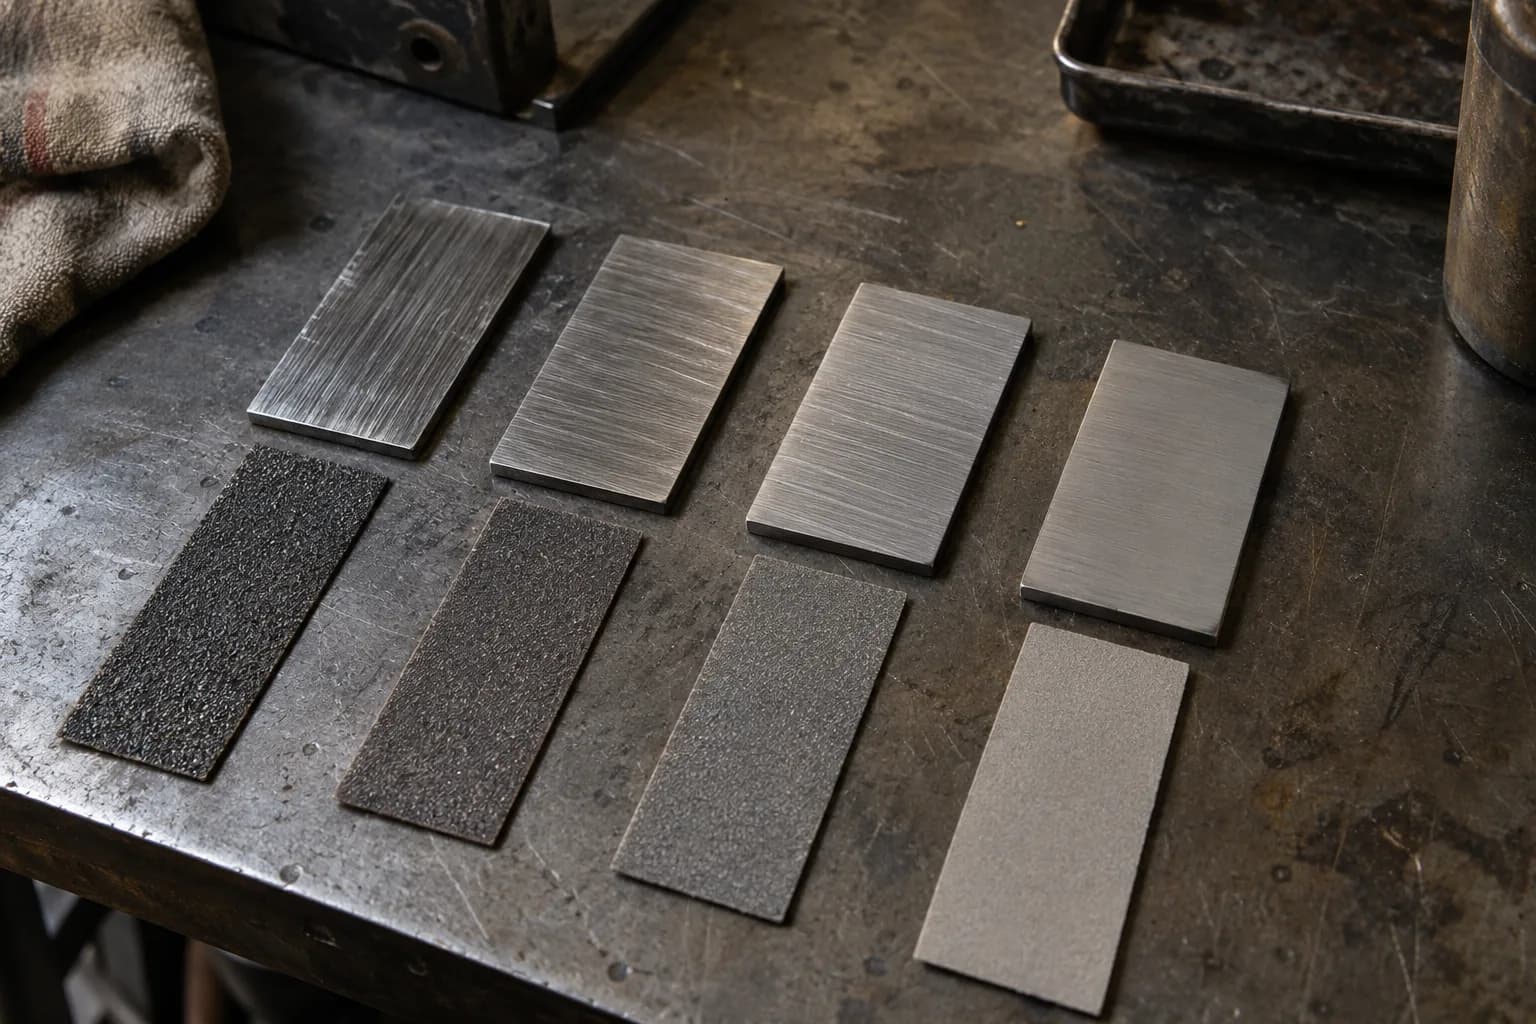
| Stage | Grit |
| Profiling / heavy stock removal | 50 |
| Bevel refinement | 60 |
| Pre-finish | 80 |
| Finish grinding | 120 |
Use higher belt speed with light, controlled passes rather than heavy, slow pressure, which loads the belt faster without cutting any more effectively. Keep a belt eraser or dressing stick close by and clean the belt regularly. A generous coolant mister helps prevent overheating, both for the edge and for belt life, since CPM 20CV’s demanding heat treat (see the heat treat details further down this page) means preserving the temper during grinding matters even more than usual.
Standard aluminum oxide or ceramic stones struggle to cut CPM 20CV’s carbide structure efficiently once hardened. Diamond stones are the clear recommendation for reprofiling and touch-ups, cutting cleanly through the carbides rather than just burnishing over them. A practical progression many sharpeners use is a coarse diamond or waterstone in the 1000-1200 grit range, followed by a medium stone around 5000 grit, then stropping with diamond compound for a final polish. Ceramic hones can work for light touch-ups between full sharpenings, but are not a substitute for diamond abrasives when the edge needs real correction.
Keep reading
Three more from the same bench.
Heat treating is what turns a piece of flat bar stock into a functional knife blade. Done correctly, it transforms the steel’s internal crystal structure…

Belts are the single biggest recurring cost in this hobby, and buying the wrong ones wastes money twice: once on belts that wear out fast, and again on…
Every Torus ships as a complete assembled chassis with the motor sold separately — which hands you the one decision that shapes the machine’s personality…
Same bench
I machine the parts, hand-assemble, track and test Torus grinders in Sterling, Illinois. Most orders ship in seven to ten business days from time of order.

Current dual-axis platform with a fiber-laser-cut 6061 chassis and single-knob tracking.

Current dual-axis platform with a steel chassis, more mass and less vibration.

Prior-design aluminum chassis, 90-degree tilt and 1.5-inch tooling arms.

One-man shop
I answer my own email. Tell me the steel, the machine and what it is doing, and I will tell you what I would try next.