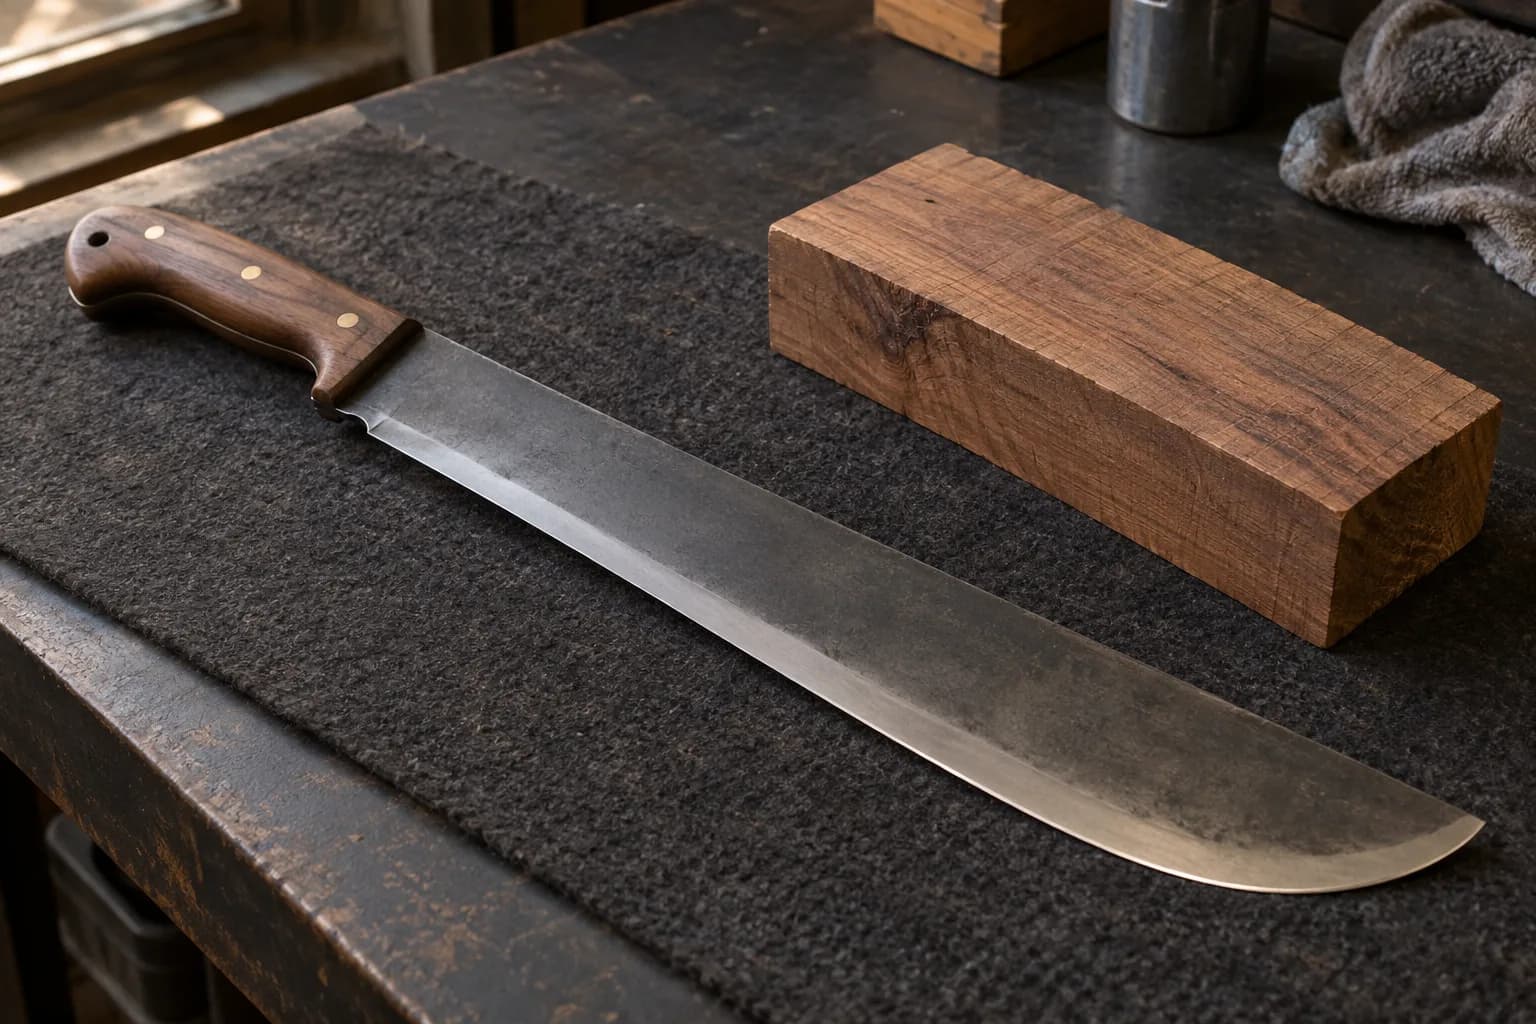
| Toughness | 5/5Among the toughest of the simple high-carbon steels, which is why it is the go-to choice for swords, machetes, and other blades that need to survive hard impacts without chipping or snapping. | 4/5Very good for a simple carbon steel, and a big part of why it is so widely recommended: it holds up well to impact without the brittleness risk that comes with over-hardened, lower-manganese steels like 1095. | 1075 holds a real edge here, among the toughest simple carbon steels available, which is exactly why it is favored for swords and machetes over 1084. |
|---|
| Edge retention | 2/5Lower carbon content than 1084 or 1095 means fewer carbides and correspondingly modest wear resistance; expect to touch up the edge more often on demanding use. | 2/5Modest, in line with other simple carbon steels lacking wear-resistant alloy carbides, but it takes a very keen edge easily. | Tied. Both share similar carbon content and offer modest, comparable wear resistance typical of simple high-carbon steels. |
|---|
| Corrosion resistance | 1/5No chromium and no meaningful corrosion resistance. Needs regular oiling and drying like any plain carbon steel. | 1/5No chromium and no meaningful corrosion resistance. Needs regular oiling and drying like any plain carbon steel. | Tied. Neither has meaningful corrosion resistance and both need the same regular oiling and drying. |
|---|
| Heat treat | Austenitize at 1450-1480 F, holding 5-15 minutes. Because 1075 carries less manganese than 1084, it hardens best in a fast oil (such as Parks 50) rather than a slower conventional quench oil, reaching roughly 64-65 RC as-quenched. Temper in two 2-hour cycles: around 400-450 F for tough, hard-use blades like swords and machetes (57-61 RC), or as low as 300-350 F for applications favoring edge holding over shock resistance (63-65 RC), letting the blade cool to room temperature between cycles. | Optionally normalize at 1607-1652 F to refine grain and relieve stress after forging or heavy machining. Austenitize at 1500-1525 F, holding 5-15 minutes, then quench in preheated oil (around 104-140 F) for reliable, full hardness thanks to 1084's higher manganese content. Temper starting around 350 F, going up to about 450 F depending on desired hardness; for general hunting and utility blades, 375-425 F for 2 hours across 2-3 cycles is a common recommendation, letting the blade cool to room temperature between cycles. | 1084's higher manganese content gives it more reliable hardenability in ordinary oil. 1075 needs a faster-quenching oil to reach full hardness, making 1084 the more forgiving choice for less controlled quench setups. |
|---|
| Grinding | 5/5Very easy to grind and forge, with a wide, forgiving heat-treat window that makes it a common recommendation for first-time bladesmiths. | 5/5Extremely easy to grind and forge, one of the most forgiving steels available for both stock removal and forging work. | Tied. Both are among the easiest steels available to grind and forge. |
|---|